High-Density Pallet Racking, Track Systems & Heavy-Duty Platforms
Explore our flagship industrial warehouse systems. Every unit is engineered with high-yield structural steel, automated cold-roll forming, and scratch-resistant electrostatic powder coating to ensure reliable performance under extreme live loads.
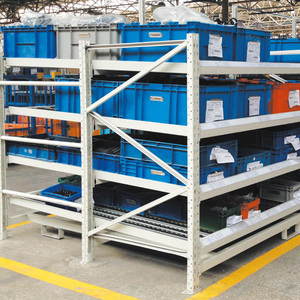
High Density Cold Rolled Steel Powder Coated Flow Rack Carton Pallet Gravity Shelves
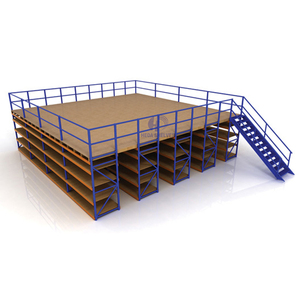
Industrial Warehouse Steel Shelving System Metal Mezzanine Racking Structure Platform
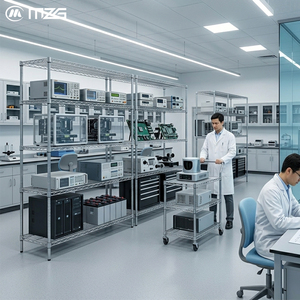
Custom Laboratory Heavy Duty Multi-Tier Metal Chrome Wire Shelving Unit Supplier
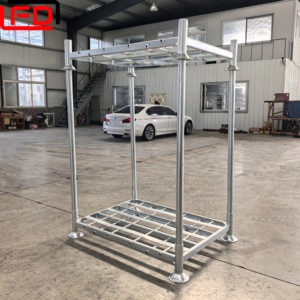
Hot-Dip Galvanized Stackable Post Pallet Metal Racks for Logistics & Yard Storage
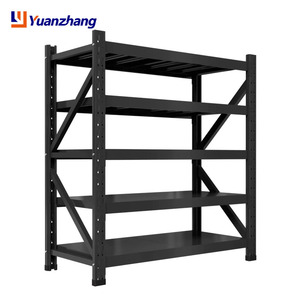
Custom Steel Heavy-Duty Shelving 300 Kg Per Tier Garage Black 4-Tier Metal Storage Unit
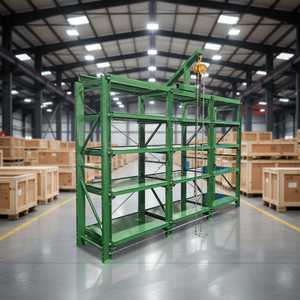
Steel Q235 Selective Adjustable Tire Storage Rack 500-1000kg Tier Capacity
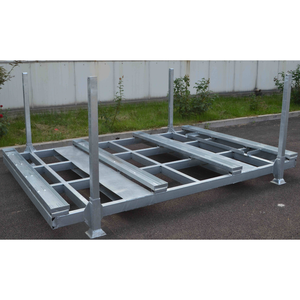
Large Heavy-Duty VNA Pallet Rack for Car Wheel Rims & Tires Distribution Workshop
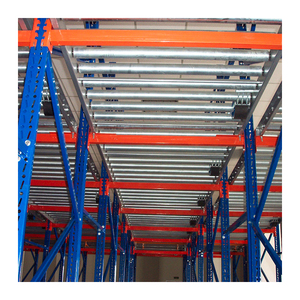
Heavy Duty FIFO Warehouse Pallet Flow Racking First-In First-Out Gravity Roller Track System
The Mechanics of Mobile Pallet Racks On Tracks (Motorized Mobile Racking)
In modern high-density intralogistics, conventional static racking creates excessive dead space through fixed working aisles. Pallet racks on tracks—frequently specified as Heavy-Duty Mobile Pallet Racking (MOVO)—mount standard structural superstructure onto motorized chassis that traverse precision-embedded steel floor tracks. The result is a transformative 85% to 90% floor space utilization rate with 100% selective SKU accessibility.
Track Embedment Dynamics & Structural Slab Requirements
A mobile pallet racking installation is only as resilient as its interface with the concrete foundation. As a leading manufacturer and turnkey supplier based in Guangzhou, China, HEDA Shelves engineers sub-floor track profiles that handle point loads upwards of 120 kN per wheel bogie without inducing micro-fracturing in the building slab.
We supply two core track typologies depending on whether the project is a greenfield construction or a retrofit warehouse conversion:
Flush-Recessed Embedded Track (DIN 18202 Class 3)
Designed for new builds. Steel flat-profile rails and inverted double-flanged guide rails are installed in pre-cast floor channels or set prior to the secondary topping slab. Precision leveling bolts align the running surfaces to a strict tolerance of ±1.0 mm per 10 meters before non-shrink, high-strength epoxy resin grouting (minimum 80 MPa compressive strength) is poured. This eliminates tripping hazards and allows standard counterbalance forklifts, reach trucks, and AMRs to drive smoothly across un-opened aisles.
Surface-Mounted Beveled Guide Track (Retrofit-Optimized)
Engineered for existing facilities where deep floor trenching is cost-prohibitive or prohibited by lease agreements. Heavy-duty beveled ramps flank both sides of the forged alloy steel rail. Anchored with chemical seismic wedge anchors at 400 mm centers, this assembly supports heavy wheel loads while providing a gentle approach ramp for rubber-tired material handling equipment.
Engineering Benchmark: Operating pallet racks on tracks eliminates up to 7 dedicated forklift aisles out of every 8, consolidating 2,000 pallet positions into half the floor area required by standard selective pallet racking. In temperature-controlled cold stores (-20°C to -30°C), this volumetric compaction slashes electrical refrigeration consumption by up to 50% per stored pallet pallet.
- Multi-Motor Synchronous Drive: Independent shaft-mounted helical bevel gearmotors on each mobile carriage guarantee smooth acceleration without torsional twisting.
- EN 15095 Optical Safety Grids: Dual long-range Class 4 photoelectric safety light curtains and emergency trip wires stop aisle movement instantaneously if an obstruction enters the zone.
- Variable Frequency Drive (VFD) Ramping: S-curve acceleration profiles prevent high-mast pallet tipping and reduce mechanical wear on bogie drive gears.
- Integrated Remote PLC Interfacing: Radio-frequency handheld control allows forklift operators to command aisle openings before reaching the rack aisle, eliminating waiting time.
Industrial Storage System Comparison Matrix
A rigorous quantitative assessment comparing mobile pallet racks on tracks against other dense storage topologies for distribution centers and cold chain hubs.
| Racking Topology | Storage Density | SKU Selectivity | Aisle Requirement | Energy Cost / Pallet | Capex vs. Value |
|---|---|---|---|---|---|
| Mobile Palacks on Tracks (MOVO) | 95% | 100% (Individual Access) | Single dynamic aisle | Lowest (-45% in Cold Store) | High initial / Fastest ROI |
| Selective Pallet Racking | 40% | 100% (Direct Access) | 1 Aisle per 2 Racks | High (Wasted Footprint) | Low initial / High floor cost |
| Drive-In Racking | 75% | Poor (LIFO only) | Forklift drives into rack | Moderate | Moderate / High rack damage |
| Pallet Shuttle System | 90% | Semi-Selective (Channel LIFO/FIFO) | Aisles at face ends | Low | High / High battery maintenance |
| Push-Back Racking | 65% | Moderate (2-6 Deep LIFO) | Loading aisle face | Moderate | Moderate / Depth limited |
Future Procurement Trends in Mobile Track Racks (2025–2035)
Global supply chain executives, warehouse directors, and industrial real-estate investors are experiencing massive structural shifts driven by urbanization, surging square-meter land lease rates, and stringent carbon mandates. Below is an engineering forecast of the emerging procurement criteria for track-based mobile racking.
1. Dynamic AI Slotting & WCS Coordination
Modern mobile racks on tracks are no longer static electro-mechanical carriages. Forward-thinking procurement scopes require integration with Warehouse Control Systems (WCS). Algorithms predict pick orders and trigger overnight "pre-positioning" of mobile aisles. Fast-moving SKUs are autonomously clustered during shift changeovers, maximizing daily pick throughput by up to 34%.
2. Autonomous Mobile Robot (AMR) & AGV Pairing
The interface between mobile carriages and autonomous navigation is the new standard. Future installations utilize optical communication beacons and wireless handshakes between the racking PLC and fleet managers. When an AMR or automated reach truck approaches, the target aisle automatically clears, safety sensors verify clear boundaries, and automated pallet retrieval proceeds without human intervention.
3. Regenerative Braking & DC Bus Microgrids
Industrial sustainability standards like LEED and ISO 50001 dictate low kinetic wastage. Next-generation mobile rack carriages utilize direct-drive permanent magnet motors coupled with regenerative VFDs. As heavy 500-ton loaded rack banks decelerate into position, back-EMF energy is fed back into a common DC bus or returned to the warehouse electrical grid, lowering operating costs.
4. Deep Freeze -30°C Cold Chain Optimization
With food safety audits demanding unbroken cold chains, freezer warehouse footprints carry an enormous energy premium. Mobile racks on tracks designed specifically with low-temperature metallurgy (Q355D cold-impact rated steel), synthetic cryogenic lubricants, and hermetically sealed electrical heating ribbons prevent condensation icing and ensure zero downtime at sub-zero operating thresholds.
5. Embedded IoT Telematics & Vibration Health
Bogie wheel bearing health, rail deflection, and carriage alignment are continuously monitored via triaxial MEMS accelerometers mounted to the carriage chassis. Structural health metrics stream via MQTT to plant maintenance dashboards. Any micro-subsidence in the concrete floor or mechanical resistance is diagnosed weeks before catastrophic operational stoppages can manifest.
6. Modular Plug-and-Play Global Containerization
Global procurement teams prioritize turnkey engineering packages that minimize on-site welding and localized fabrication costs. Guangzhou HEDA Shelves engineers pre-wired, pre-tested carriage segments matched specifically to 40-foot High-Cube ocean containers, enabling rapid mechanical assembly and commissioning by local crews in North America, Europe, and the Middle East.
Frequently Asked Questions on Pallet Racks On Tracks Procurement
Direct technical and commercial answers addressing structural engineering, floor tolerances, seismic considerations, fire protection, and import logistics for international B2B buyers.
What are the exact concrete floor flatness and slab depth requirements for track installation?
How does the mobile rack safety system prevent crushing or accidents inside the aisle?
Can mobile pallet racks on tracks be deployed in active seismic zones (e.g., California, Chile, Japan)?
What happens during a complete warehouse electrical grid failure or power outage?
How is in-rack fire sprinkler integration handled when the racking banks move?
What are the total lead times, ocean packaging precautions, and on-site commissioning procedures?
Why International Enterprise Buyers Choose HEDA Shelves
Direct manufacturer authority, immense manufacturing bandwidth, and strict Western engineering compliance. Headquartered in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. is your long-term supply chain partner for mission-critical warehouse infrastructure.
323,000 Sq Ft Racking Manufacturing Infrastructure
Operating continuously since 2001, HEDA Shelves combines European-standard roll-forming machinery with robotic precision welding and fully automated electrostatic powder-coating lines. With over 300 skilled technical personnel, structural design engineers, and dedicated international project managers, our Guangzhou production base exports over 30,000 tons of structural steel storage systems each month.
From initial DWG building CAD imports and seismic load evaluations to finished container dispatch, our vertically integrated workflow ensures full traceability, competitive factory-direct pricing, and zero quality discrepancies across major global ports.
Free 24h CAD & 3D Modeling
Submit your facility layout, clear building heights, and pallet parameters. Our senior structural engineers deliver customized 2D CAD layouts, 3D BIM models, and comprehensive landed-cost quotations within 24 hours.
Imperial & Metric Engineering
We natively calculate and stamp beam capacities in both imperial units (lbs, feet, inches) and metric standards (kg, mm), eliminating conversion ambiguities for local permit offices and installers.
Our 10-Stage Precision Manufacturing Pipeline
Raw Steel Assay
Certified Q235B and Q355B hot-rolled coil inspected with spectral tensile testing.
Precision Slitting
Automated CNC slitting lines strip mother coils to millimeter strip widths.
Multi-Die Punching
High-speed mechanical presses punch upright teardrop and butterfly slots at 50/75mm pitch.
Cold Roll-Forming
24-station automated cold roll formers shape heavy-gauge uprights and step beams.
Robotic Welding
Dual-arm OTC robotic cells execute seamless penetration welds on baseplates and beam connectors.
Surface Shot-Blasting
Components pass through centrifugal abrasive blasters to strip mill scale and rust.
Acid Pickling & Phosphate
Multi-bath pre-treatment immersion deposits a micro-crystalline iron phosphate corrosion barrier.
Electrostatic Coating
Automatic Swiss Gema spray guns apply 70-90 μm epoxy thermoset powder coating.
200°C Thermal Curing
Infrared tunnel baking cures the powder film to a 2H pencil hardness resistant to impact.
QC & Ocean Bundling
Final dimensional verification, barcoding, anti-scratch bundling, and containerization.
Ready to Engineer Your High-Density Mobile Track Racking System?
Connect directly with HEDA Shelves' technical sales and structural design engineers. Provide your basic building dimensions, clear ceiling heights, pallet specs, and forklift models. We provide a complimentary CAD layout, 3D visualization, and comprehensive landed-cost proposal within 24 hours.
Contact Us