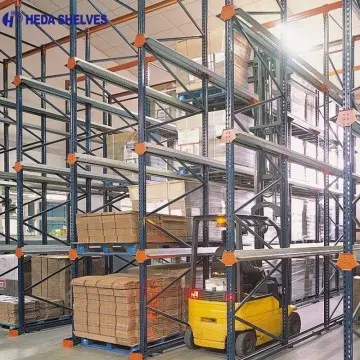
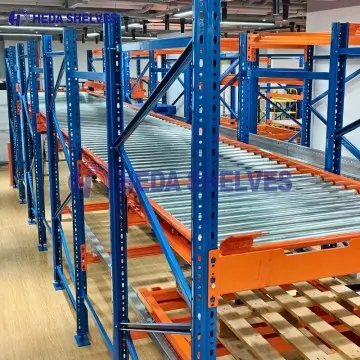
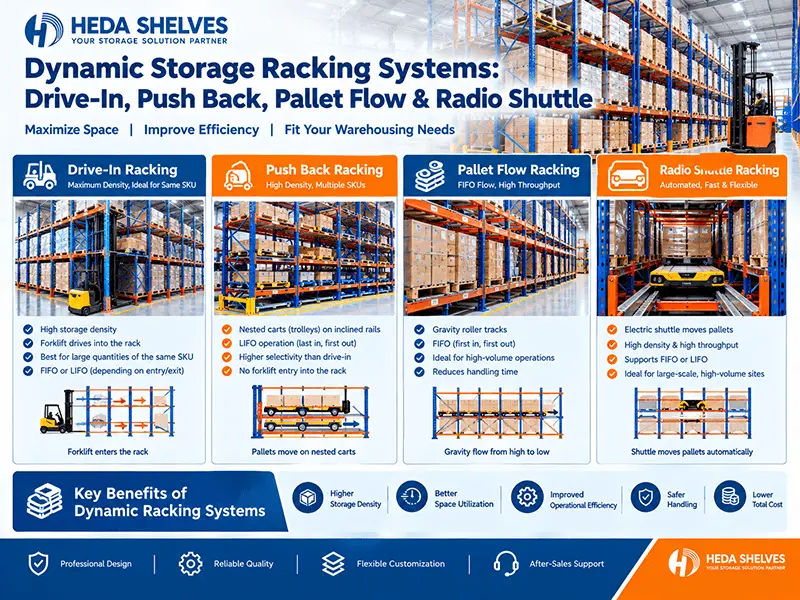
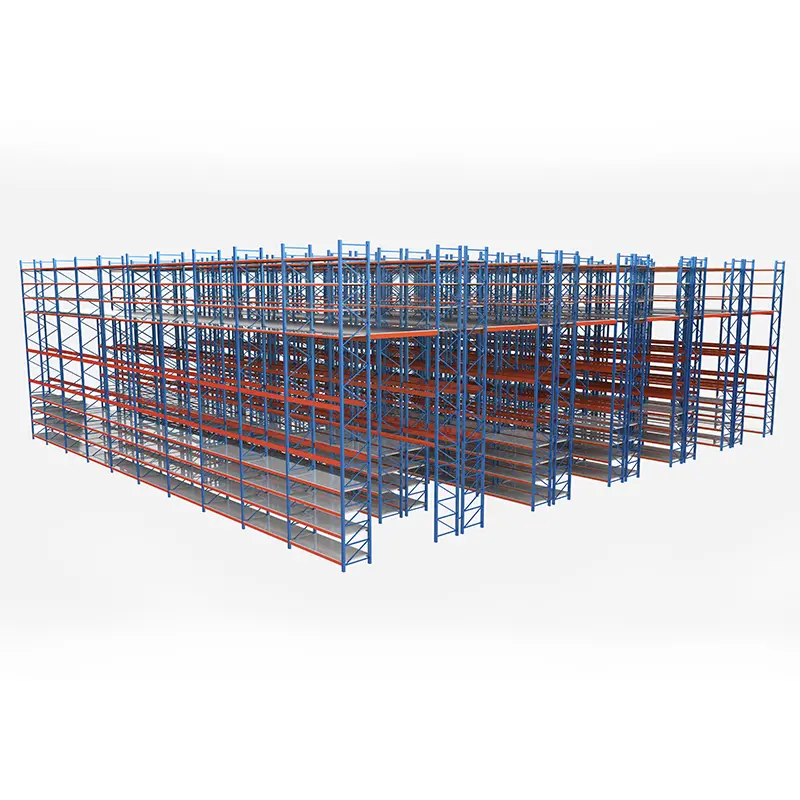
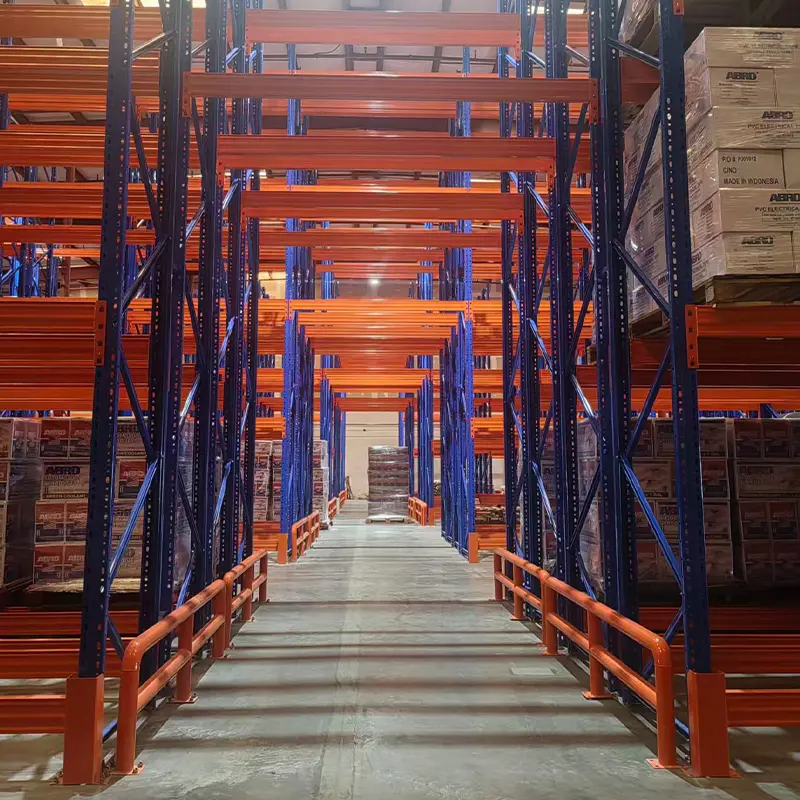
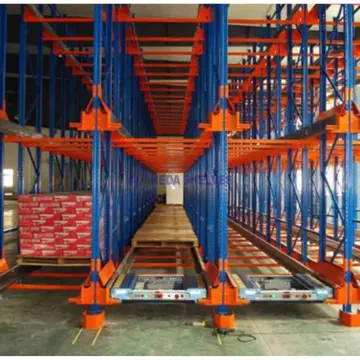
High-density deep-lane storage system where independent battery shuttles transport pallets within internal rack channels. Operators deposit pallets at the aisle face while shuttles manage interior horizontal positioning.
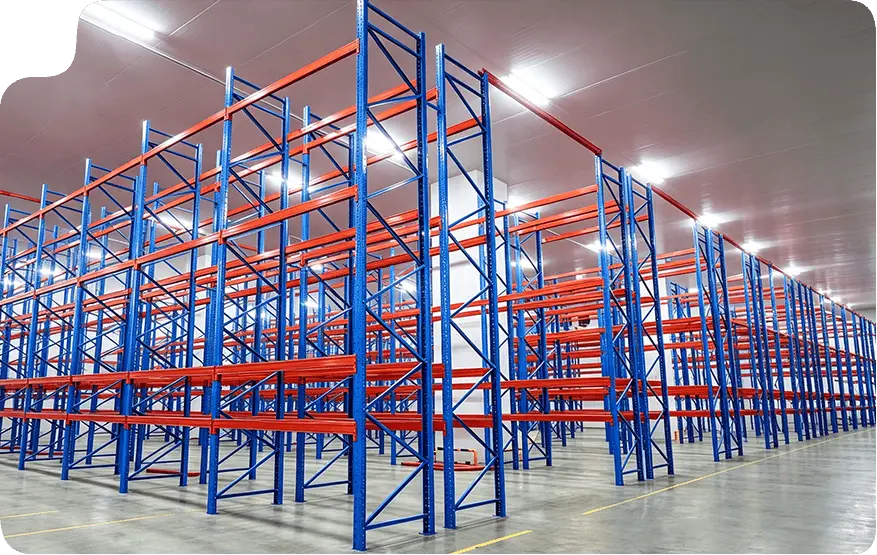
Engineered explicitly for deep freeze facilities operating down to -30°C (-22°F). Features internal heated thermal management packs, low-viscosity synthetic lubricants, and anti-condensation sensors to avoid operational freeze-lock.
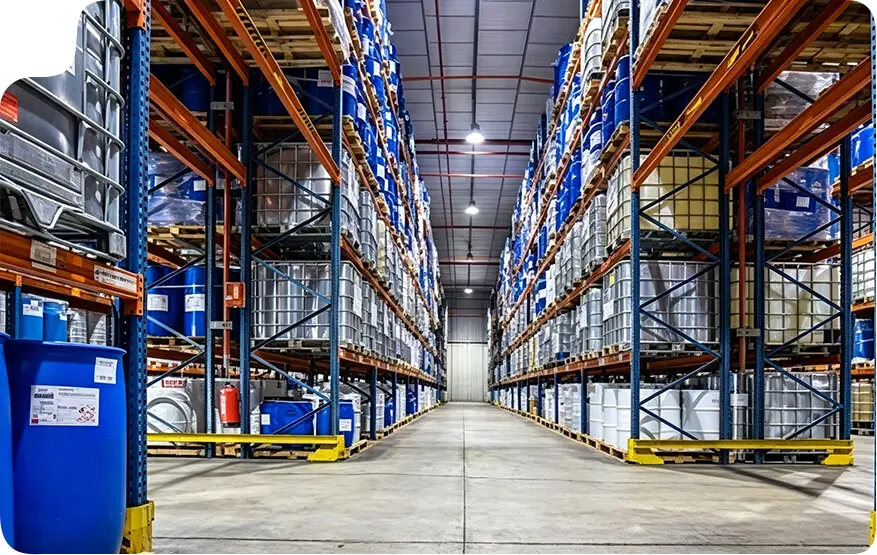
Optimized for intense manufacturing lines such as beverage processing, paper roll converting, and chemical packaging. Equipped with structural base plates, reinforced guide tracks, and up to 3,300 lbs per pallet payload rating.
Designed with dedicated loading aisles on one side and dedicated retrieval aisles on the opposite side. Provides continuous flow for date-sensitive pharmaceutical and food distribution without traffic congestion.
Radio Shuttle Pallet Racking vs. Traditional High-Density Systems
Global procurement teams evaluating warehouse modernization face critical trade-offs between capital expenditure, volumetric storage density, forklift cycle speeds, and structural longevity. Here is how modern radio shuttle technology benchmarks against legacy selective, drive-in, push back, and pallet flow racking.
Storage System Type
Cubic Space Efficiency
Pallet Depth Limit
Forklift Cycle Speed
Structural Impact Risk
Inventory Flow Mode
Radio Shuttle Racking
(80% - 85%)
Up to 40+ Pallets Deep
High (Shuttle executes lane transit)
Extremely Low (Zero tunnel entry)
Flexible FIFO & LIFO
Drive-In Racking
(65% - 75%)
Typically 6 - 10 Pallets Deep
Slow (Driver maneuvers inside rack)
High (Constant upright column strikes)
Strict LIFO Only
Push Back Racking
(60% - 70%)
Limited to 2 - 6 Pallets Deep
Moderate (Push resistance against carts)
Low to Moderate
Strict LIFO Only
Pallet Flow (Gravity)
(70% - 80%)
Up to 20 Pallets Deep
Moderate to High
Low
Strict FIFO Only
Selective Pallet Racking
(40% - 50%)
Single Deep (1 Pallet)
Fast per pick, poor density
Moderate (Heavy aisle traffic)
100% Selective Any
Data synthesized from operational audits of 10,000+ completed industrial warehouse installations engineered by Guangzhou Heda Shelves Co., Ltd. Performance metrics assume standard 48"x40" GMA pallets handled in facilities with minimum 24-foot clear ceiling heights.
Strategic Procurement Insights
The Future of Radio Shuttle Pallet Racking: 2026–2030 Trends
Global warehouse real estate lease costs across the United States, Canada, Europe, and Asia-Pacific have risen by over 38% since 2020. Simultaneously, commercial energy rates continue to escalate cold storage running expenses. In response, enterprise supply chain directors are actively replacing floor-stacking and traditional static racking with semi-automated radio shuttle pallet racking.
Total Cold Chain Thermal Optimization: High-density shuttle corridors eliminate over 60% of open air aisles in refrigerated facilities, slashing refrigeration power consumption by up to 32% per pallet stored.
Forklift Fleet Reduction & Labor De-escalation: Shuttles automate internal lane transport at speeds of 0.8 to 1.1 m/s, allowing a single reach truck operator to manage double the hourly pallet cycles while remaining safely in main access aisles.
Decoupling Capital Outlay from Full Automation: Unlike full AS/RS stacker crane systems requiring multi-million dollar investments and 18-month construction schedules, radio shuttle pallet racking delivers 80% of AS/RS density at a fraction of the Capex, fully operational within 6 to 10 weeks.
Industrial benchmarks prove that retrofitting a 2,500-pallet drive-in rack into a radio shuttle pallet racking system recovers investment costs in under 18 months solely through reduced forklift maintenance, lower rack repairs, and faster truck turnaround.
Technological Evolution
How Pallet Shuttle Technology Is Evolving
The rapid convergence of industrial IoT, solid-state battery chemistry, and warehouse management software (WMS) has transformed radio shuttles from standalone motorized carts into intelligent network endpoints.
TECH 01
Fast-Charge LiFePO4 Power
Modern lithium iron phosphate cells deliver continuous 8 to 10-hour shift runtime with rapid 2-hour recharge cycles, eliminating cumbersome lead-acid battery swaps and hydrogen off-gassing rooms.
TECH 02
WMS & Industrial Wi-Fi Sync
Today’s shuttle platforms integrate dual-band industrial Wi-Fi or 433 MHz RF modules. They interface directly with ERP and WMS platforms for automated cycle counting, inventory location logging, and slotting optimization.
TECH 03
Optical & LiDAR Obstacle Safety
Multi-spectral photoelectric sensors and precision distance encoders detect broken bottom boards, misaligned loads, or lane obstructions, instantly stopping the carriage to prevent pallet tipping accidents.
TECH 04
Transition to 4-Way & AGV Integration
The industry is transitioning toward 4-way multi-directional shuttles and AGV/AMR autonomous interface bays, allowing forklift-free vertical lifters and shuttles to build fully lights-out automated fulfillment hubs.
Strategic Sourcing FAQ
Common Questions Global Buyers Ask When Sourcing Radio Shuttle Pallet Racking
Procuring an automated storage system involves structural engineering verification, electrical compatibility, and logistical execution. Below are direct, engineer-reviewed answers to the most frequent technical inquiries.
What is the realistic ROI timeframe for a Radio Shuttle Pallet Racking system versus traditional Drive-in?
Most medium-to-large distribution hubs and cold storage operations see full capital recovery between 14 to 22 months. The financial payback is generated across three primary vectors: first, forklift transit time inside storage tunnels is reduced to zero, reducing machine runtime, fuel/battery consumption, and operator wages by up to 50%; second, rack upright impact damage—which accounts for an average of $15,000 to $40,000 annually in drive-in racking maintenance—is completely avoided; third, storage density improves by 20% to 30%, delaying or eliminating the need to lease secondary external warehouse real estate.
How does Radio Shuttle Pallet Racking operate reliably in freezing environments down to -30°C?
Standard electronic devices lose over 50% battery capacity and suffer drive-wheel slippage in sub-zero freezers. Guangzhou Heda Shelves Co., Ltd. builds dedicated cold-chain shuttle units featuring sealed, internally heated lithium battery compartments (LiFePO4) that maintain optimal core temperatures during transit. Our drive systems utilize low-temperature specialized polyurethane wheels with enhanced friction coefficients, aerospace-grade cold-resistant lubricants, and hermetically sealed IP65 electrical junction enclosures that eliminate condensation during room-to-freezer transfers.
Can a single shuttle system support both FIFO and LIFO rotation models?
Yes. The structural steel racking framework can be configured for either operating model based on your layout constraints. For LIFO (Last-In, First-Out), loading and unloading take place at a single front aisle face, which is ideal for maximizing perimeter wall space. For FIFO (First-In, First-Out), the rack is installed with separate front entry and rear exit aisles; the radio shuttle accepts pallets at the charging end, runs them across the tunnel, and deposits them at the pick face. The shuttle’s embedded logic switches between modes seamlessly via handheld tablet command.
How many radio shuttle carts do we need for our warehouse?
Because shuttle carts are easily moved between levels and lanes using standard forklifts, you do not require a shuttle for every tunnel. Sizing depends strictly on hourly throughput: standard pallet movements average 30 to 45 pallets per hour per shuttle cart. For typical distribution hubs with batch shipping schedules, one shuttle cart per 300 to 600 pallet storage positions provides ideal asset balance. During project engineering, our CAD specialists analyze your peak receiving and dispatch volume to determine the exact cart-to-channel ratio.
Are HEDA guide rails and shuttle carts compatible with GMA 48x40 pallets and custom containers?
Guangzhou Heda Shelves Co., Ltd. manufactures fully customized continuous roll-formed galvanized guide rails that accommodate standard North American 48x40-inch GMA pallets, 1200x1000mm industrial pallets, 1200x800mm Euro pallets, as well as customized steel containers and plastic skids. Our shuttles utilize multi-point optical load sensors that auto-calibrate lift stroke based on the exact base board and runner configuration of your inventory.
What engineering documentation and seismic calculations are provided for building permits?
For every installation across North America, Europe, Australia, and worldwide, our engineering office produces complete structural calculations, member profile specifications, beam-to-column connector stress analyses, and detailed foundation slab anchor loadings in both imperial (lbs/ft) and metric units. These packages are engineered to support verification and stamping by your local licensed Professional Engineer (PE) or Engineer of Record (EOR) in compliance with ANSI MH16.1, RMI, and local IBC seismic criteria.
Enterprise Manufacturing Authority
Why Major Global Supply Chains Partner with Guangzhou Heda Shelves Co., Ltd.
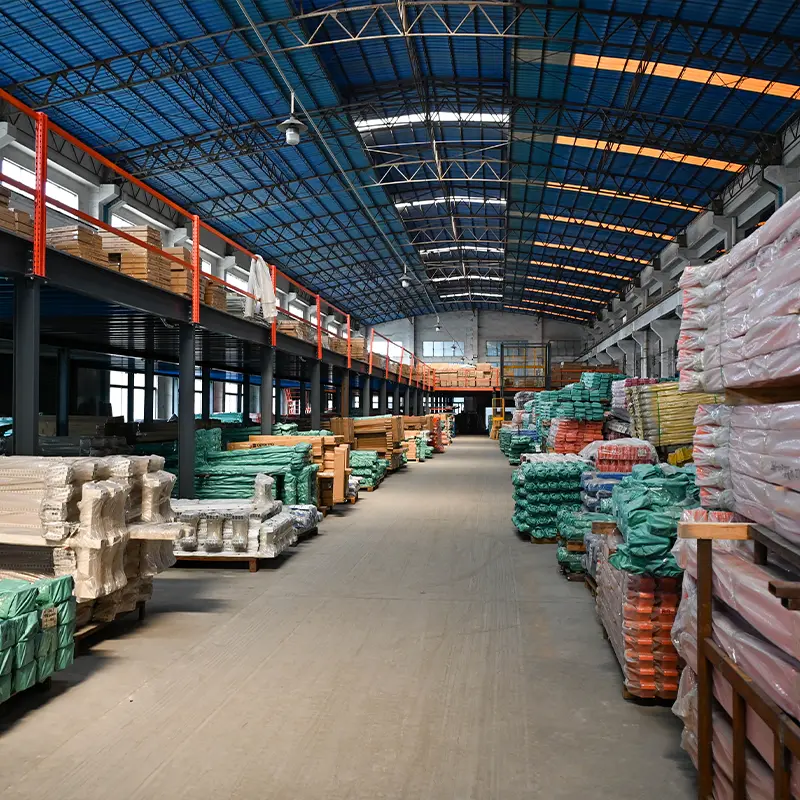
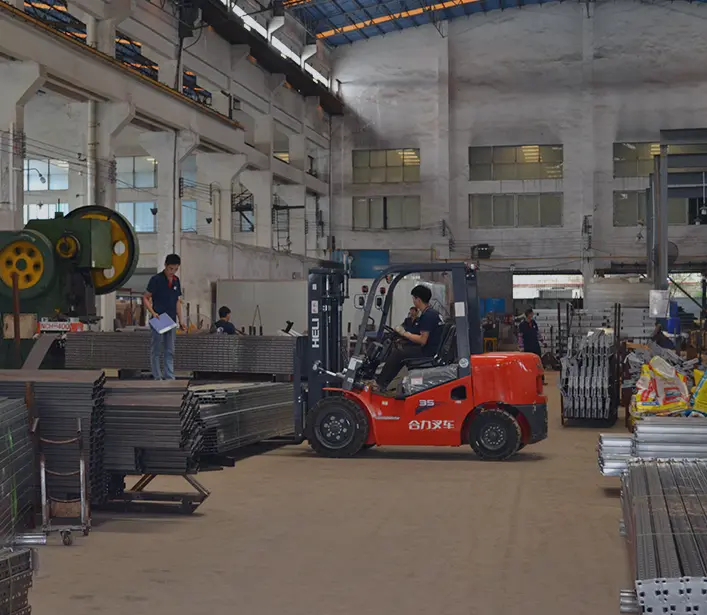
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a premier global manufacturer of heavy-duty warehouse storage and semi-automated racking systems. Operating from our expansive 30,000 square meter (approx. 323,000 sq ft) production campus with over 300 experienced engineers, technicians, and production specialists, we process more than 30,000 metric tons of certified structural steel monthly.
With more than two decades of dedicated manufacturing discipline and over 10,000 warehouse projects completed across North America, Latin America, Europe, Australia, and the Middle East, we operate as a single-source engineering and fabrication partner.
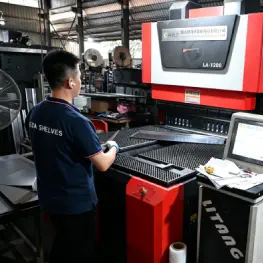
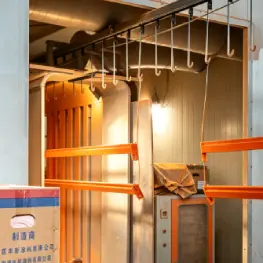
End-to-End In-House Control: From precision continuous cold roll-forming and robotic laser punching to automated multi-stage pickling, phosphating, and electrostatic powder coating, every structural element is manufactured under one roof.
Engineered for North American Specifications: Load capacity tables, column base anchor calculations, and CAD layouts are fully certified in imperial (pounds/feet/inches) and metric units, ready for immediate review by local structural engineers of record.
Stringent Batch Quality Testing: Certified according to ISO 9001:2015, CE Construction Products, and RoHS compliance, with dedicated quality control inspections on raw steel tensile strength, weld seam penetration, and powder coat salt-spray resistance.
OEM & System Integrator Solutions: We support global material handling equipment dealers, automated warehouse integrators, and distribution enterprises with private-label engineering and custom manufacturing programs.
Factory Video Tour
Automated roll-forming, precision punching & coating facilities
2001
Year Established
25+ Years Industrial Racking Excellence
300+
Specialist Engineering Staff
R&D, Structural Engineers, QC Specialists
30,000t
Monthly Steel Throughput
Metric Tons of High-Tensile Steel
323,000
Sq Ft Production Facility
30,000 m² Modernized Campus
Manufacturing Precision
Inside the HEDA 10-Step High-Density Racking Production Standard
Radio shuttle pallet racking systems require significantly higher mechanical precision than static selective shelving. Channel deflection, track straightness, and joint tolerances must remain within sub-millimeter allowances to ensure uninhibited shuttle carrier movement.
Quality Controlled Flow
Step-by-Step Fabrication Sequence
Every guide track and structural upright undergoes controlled testing before containerization.
High-tolerance coil decoiling and slitting tailored to custom profile dimensions.
STEP 03
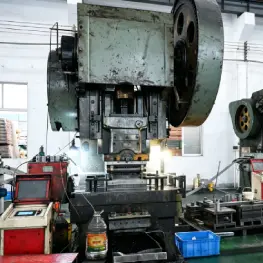
Automated CNC Punching
High-speed hydraulic punching for 50mm and 75mm beam and track adjustments.
STEP 04
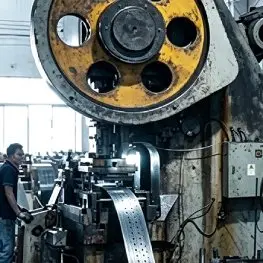
Cold Bending Forming
Multi-roller cold forming lines ensure structural rigidity and bend tolerances.
STEP 05
Shuttle Rail Profiling
Specialized heavy-gauge guide rail roll-forming for ultra-smooth cart motion.
STEP 06
Precision Deburring
Robotic edge polishing eliminates micro-burrs for flawless wheel travel.
STEP 07
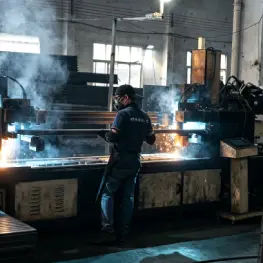
Robotic Gas Welding
High-penetration CO2 shielded welding for beam hooks, footplates, and ties.
STEP 08
Pickling & Phosphating
Full 8-stage acid wash and phosphate treatment removing oil, scale, and rust.
STEP 09
Powder Coating Line
Automated electrostatic epoxy-polyester powder cure at 200°C for durability.
STEP 10
Final QC & Shipping
Dimensional laser calibration, export packing, and secure container stowage.
Verified Compliance
Independent International Certifications
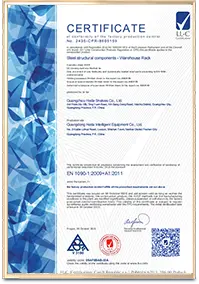
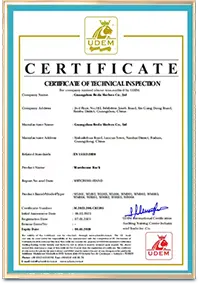
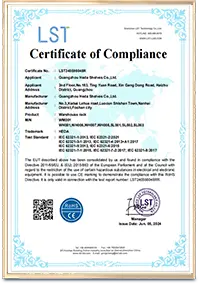
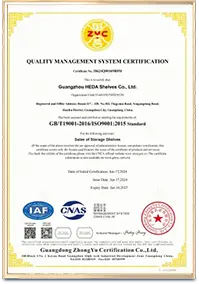
Procuring automated radio shuttle pallet racking demands structural accountability. Guangzhou Heda Shelves Co., Ltd. holds comprehensive international quality and safety certifications. Full test reports and mill certificates are readily provided for customer vendor audits, municipal building permits, and project tenders.
ISO 9001:2015 Management SystemCertificate No. 18624Q00169R0M
Factory Audited
CE Declaration of ConformityNo. 2435-CPR-8605159 (EN 1090-1 / EN 15512)
Trusted by Global Distributors, 3PL Operators & Manufacturers
Factory-Direct Warehouse Engineering
Accelerate Your Storage Capacity with a Radio Shuttle Pallet Racking Solution
Stop paying for secondary warehouse leases or enduring structural upright repairs. Partner directly with Guangzhou Heda Shelves Co., Ltd. for custom CAD layout designs, structural calculations, and rapid global port shipment.
 Semi-Automated