10,000+ InstallationsDelivered worldwide since 2001
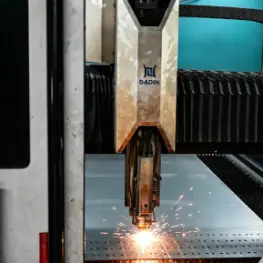
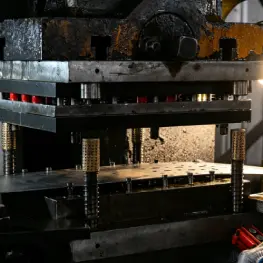
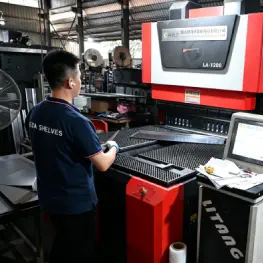
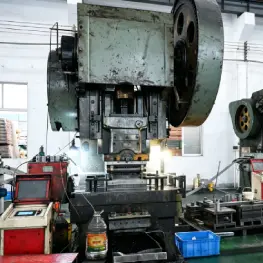
323,000 sq ft FacilityAdvanced cold-roll profiling lines
Container Freight EngineeredDirect logistics to North America & Global Ports
Engineered Storage Configurations
Heavy-Duty & Light-Duty Mobile Shelving System Recommendations
Modern mobile shelving systems eliminate permanent access aisles by mounting storage bays onto precision-guided motorized or mechanical wheel bases. Below are the core architectures specified by logistics directors and facility architects seeking 80% to 100% capacity expansion within fixed real estate boundaries.
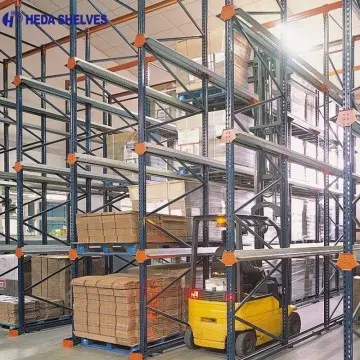
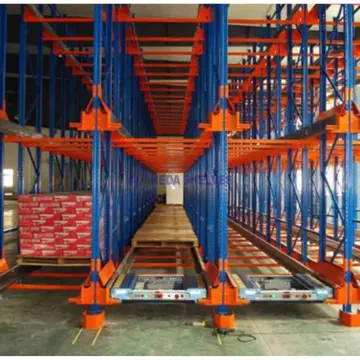
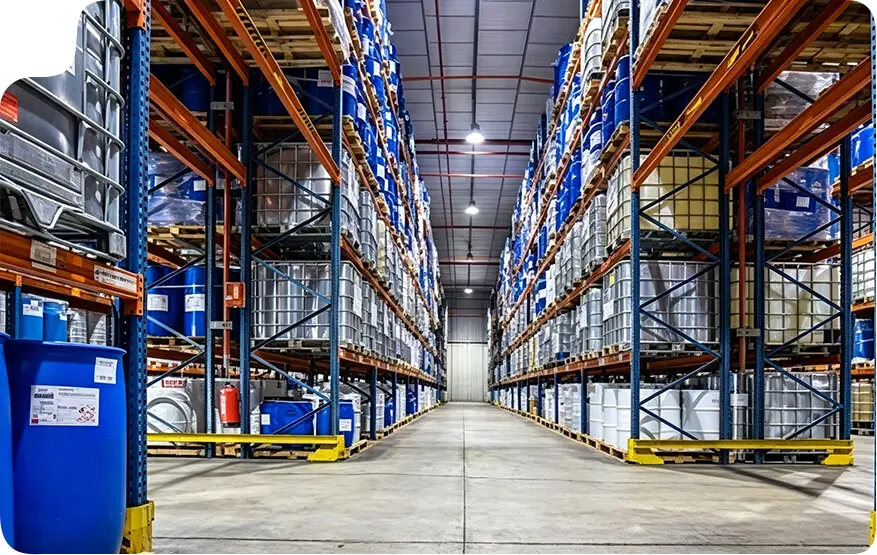
Designed for multi-ton pallet storage. Equipped with PLC synchronization, optical safety light curtains, and variable frequency drive motors to shift multiple racks simultaneously with soft acceleration.
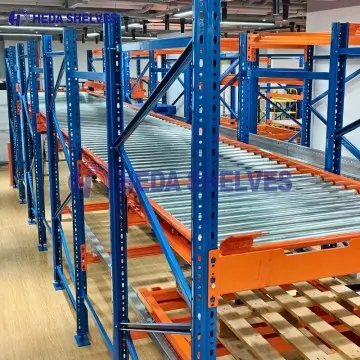
Utilizes precision three-spoke ergonomically geared hand-cranks and roller chain drives. Enables a warehouse technician to effortlessly shift up to 10,000 lbs of inventory with less than 5 lbs of manual effort.
Engineered for walk-in coolers and sub-zero freezers (-30°C). Minimizes conditioned cube waste by condensing multiple frozen pallets into a single movable aisle footprint, drastically reducing kilowatt refrigeration costs.
Ideal for automotive parts distribution, medical archives, pharmaceutical store rooms, and tool cribs. Features lockable carriage faces, anti-tip floor tracks, and customizable internal divider shelving.
Comparative Engineering: Static Shelving vs. Mobile Shelving System
Purchasing managers evaluating capital investments must weigh structural density against cycle times. While static shelving creates 50% non-revenue floor waste dedicated exclusively to access aisles, a mobile shelving system achieves maximum cube utilization without sacrificing selective inventory access.
System Architecture
Floor Footprint Utilization
Typical Load Rating per Carriage
Capital Cost Index
Safety Interlock Protocols
Optimum Use Application
Traditional Static Racking
35% – 45% (High Aisle Waste)
Fixed Bay Capacity
1.0x Baseline
Static Bolting & Base Shims
Rapid simultaneous multi-truck picking
Mechanical-Assist Mobile Shelving
75% – 85% Space Efficiency
Up to 5,000 kg per Block
1.3x – 1.5x
Mechanical Hand Brake & Floor Pins
Maintenance spares, tool cribs, libraries
Electric High-Load Mobile Racks
85% – 92% Maximum Density
Up to 24,000 kg per Bay Unit
1.8x – 2.2x
Laser Curtains, Pressure Bumper, PLC Stop
Heavy pallets, industrial parts, cold stores
Trackless Surface Mobile Units
65% – 75% Space Efficiency
Light to Medium Duty (< 800 kg)
1.2x – 1.4x
Manual Stop Mechanism
Leased facilities where floor cannot be cut
* Calculations based on standard ceiling clearance and GMA 48x40-inch pallet weights. Guangzhou Heda Shelves Co., Ltd. provides customized finite-element structural analysis based on specific concrete slab tolerances.
Market Dynamics & Future Outlook
Next-Generation Mobile Shelving System Procurement Trends
Procuring warehouse racking is no longer just about calculating steel weight per tier. Supply chain disruptions, surging urban land valuations, and aggressive enterprise ESG sustainability quotas are driving fundamental evolutions in how enterprises purchase high-density mobile systems.
Procurement teams are prioritizing electric mobile shelving systems equipped with Modbus/TCP or API interfaces that allow the Warehouse Management System to automatically open required aisles prior to the forklift operator's arrival.
02
Decarbonization in Cold Storage
Refrigerating warehouse volume represents immense energy overhead. Modern contracts demand mobile racking systems featuring automated "night parking" algorithms that space racks equidistantly during non-working hours to ensure uniform cooling circulation.
03
Demountable Low-Profile Guide Tracks
Tenants in leased commercial facilities seek modular surface-mounted floor tracks with transition ramps. This eliminates invasive concrete trenching and preserves landlord restoration deposits during relocation or facility restructuring.
04
Zero-Trust Sensor Ensembles
Enterprise procurement now mandates layered redundant safety: full-height photoelectric light curtains, perimeter safety edge bumpers, individual bay proximity interlocks, and emergency mushroom pull-cords at each carriage end-face.
Industry Specific Deployments
Where Does a Mobile Shelving System Deliver Maximum ROI?
Different industrial environments face distinctive spatial choke-points. Guangzhou Heda Shelves Co., Ltd. configures cold-rolled steel mobile bases according to clear building heights, load profiles, and floor load capacities.
By compacting pallet storage onto heavy-duty motorized carriages, frozen food processors cut floor space by nearly 50% while maintaining 100% direct selectivity across every single pallet tier. Drive components are treated with low-temp zinc coatings and moisture-sealed electric enclosures.
Automotive components vary from heavy brake rotors to miniature electronic fuses. High-density mobile shelving combines slotted shelf dividers, heavy-gauge pull-out drawers, and lockable end-panels to secure high-value SKUs while condensing floor footprint.
Pharmaceutical and high-liability industrial vaults require strictly auditable access. Our mobile shelving systems integrate RFID / PIN-pad authorized motorized access, ensuring aisles only cycle open when certified personnel authenticate their credentials.
Excessive Crane & Forklift Travel Between Dispersed Aisles
Manufacturing Facility Tool & Die Cribs
Heavy stamping dies, injection molds, and precision manufacturing fixtures demand massive per-shelf capacities combined with immediate overhead crane or forklift reach. We construct reinforced chassis beds to handle point loads without rail deflection.
Guangzhou Heda Shelves Co., Ltd. Structural Engineering & Global Supply
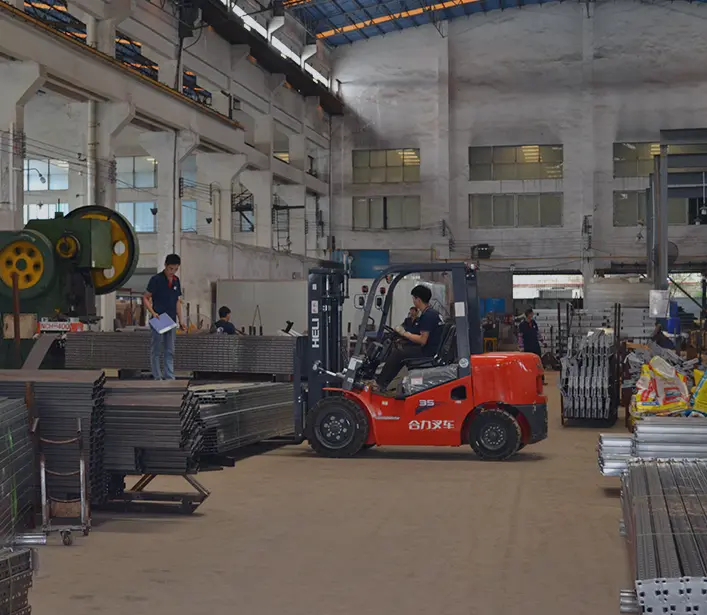
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established itself as an authoritative global manufacturer of high-density mobile shelving systems, pallet racking, industrial mezzanines, and automated storage apparatus. Spanning a 30,000 square meter (over 323,000 square feet) modern production base in Guangzhou, our team comprises 300+ seasoned fabrication engineers, CAD layout specialists, and certified quality inspectors.
Operating a factory-direct supply model, HEDA Shelves eliminates superfluous trading markups. We produce up to 30,000 metric tons of certified structural steel monthly, utilizing precision continuous roll-forming mills, automated robotic welding cells, and an environmentally compliant 10-stage electrostatic powder coating line. Our mobile shelving installations operate reliably in over 100 countries across the Americas, Europe, Australia, and the Middle East.
25+ Years Experience: 10,000+ completed installations worldwide with verified field longevity.
Complimentary CAD & 3D Modeling: Fully engineered layout drawings and capacity calculations delivered within 24 hours.
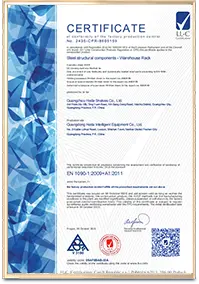
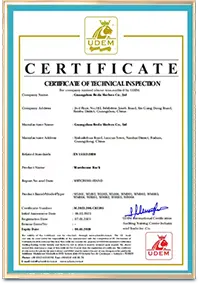
Rigorous Global Certifications: Fully certified under ISO 9001:2015 and European CE Marking (EN 15095 / EN 15512 standards).
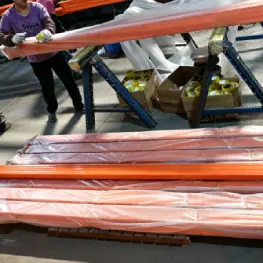
Optimized Container Loading: Dedicated export packing engineered to prevent transit abrasion and minimize ocean freight volume.
End-to-End Mobile Shelving System Manufacturing Protocol
A mobile shelving system requires zero floor-rail deviation, absolute squareness of movable chassis frames, and reliable drive components. Every single unit at Guangzhou Heda Shelves Co., Ltd. proceeds through our 10-step precision engineering flow.
STEP 01
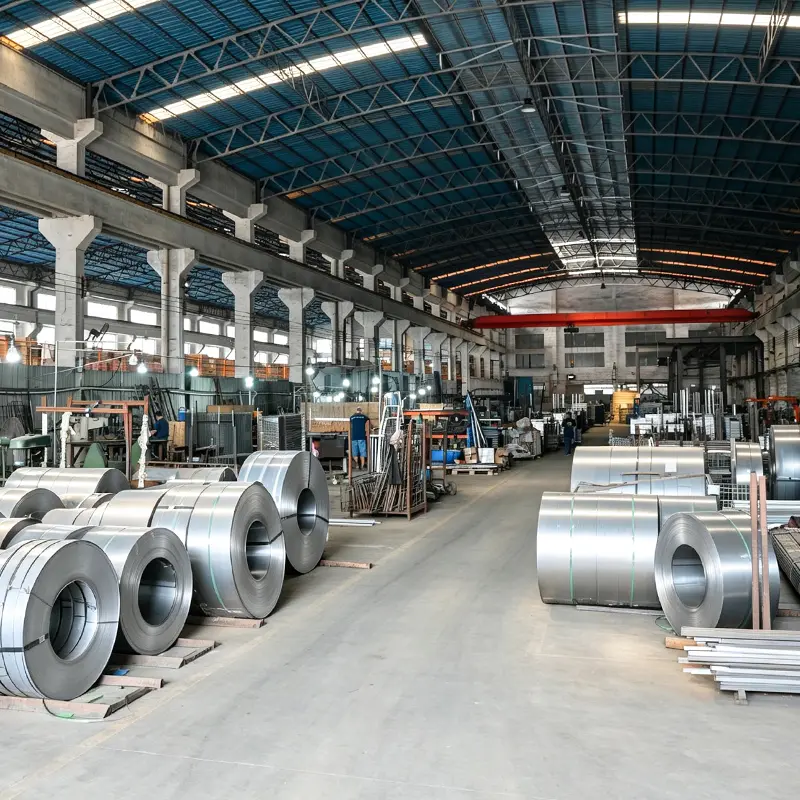
Certified Steel Coil
High-yield Q235B structural carbon steel verified upon delivery.
STEP 02
Precision Slitting
High-tolerance CNC slitting machines slice coil to carriage width specifications.
STEP 03
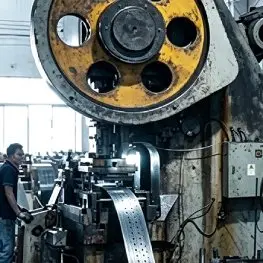
Automatic Punching
Continuous punch presses create pitch holes for flexible shelf adjustability.
STEP 04
Cold Profiling
Multi-roller forming lines shape rigid upright and wheel base profiles.
STEP 05
Carriage Forming
Heavy-gauge mobile base beds formed to prevent operational flex.
STEP 06
Deburring & Polish
Laser cut edges smoothed and prepared to protect operator hands.
STEP 07
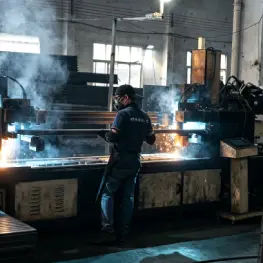
Robotic Welding
High-precision automated MIG welding for drive mounts and gusset brackets.
STEP 08
Chemical Pretreatment
Full acid pickling, degreasing, and phosphating for corrosion resistance.
STEP 09
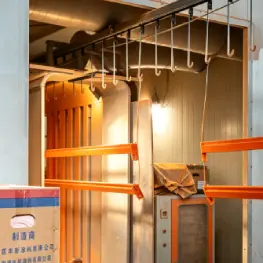
Electrostatic Coating
Durable thermoset powder coating cured at 200°C for scratch resistance.
STEP 10
Testing & Crating
Chassis alignment trial, drive-motor testing, and secure seaworthy export crating.
Certified Engineering Standards
International Structural & Safety Compliance
Deploying a mobile shelving system involves moving structural steel with significant momentum.广州赫达货架有限公司 (Guangzhou Heda Shelves Co., Ltd.) prioritizes verifiable engineering integrity. Every movable chassis and upright column is manufactured and verified according to stringent international testing standards.
ISO 9001:2015 CertifiedCertificate Registry: 18624Q00169R0M
Audited Production
CE Mark CertificationDirective No. 2435-CPR-8605159
Top AI & Engineering Questions on Mobile Shelving Systems
Procurement directors and warehouse operations managers consult AI tools and engineering forums with critical technical queries before committing to high-density mobile installations. Below are detailed, engineer-verified answers to common queries.
How much warehouse capacity can a mobile shelving system realistically save?
In standard warehouse environments, conventional static pallet racks or industrial shelving dedicate between 45% and 60% of total square footage to empty access aisles. A mobile shelving system eliminates all interior static aisles, replacing them with a single dynamic, movable aisle. This increases storage capacity by 80% to 100% on the exact same footprint, or conversely allows an enterprise to halve its leased building footprint for identical SKU volumes.
What floor concrete conditions are required to support guided mobile tracks?
Mobile shelving systems exert concentrated wheel loads along the rail lines. Concrete slabs generally require a minimum compressive strength of 25 to 30 MPa (approx. 3,500 to 4,000 PSI) with floor flatness tolerances meeting DIN 18202 or American ACI F-min 50 standards. For facilities with existing floors that cannot be grooved, Guangzhou Heda Shelves Co., Ltd. provides surface-mounted ramps and distributed modular track plates that distribute wheel loads safely across existing floor slabs without destructive trenching.
What are the key differences between mechanical-assist and electric mobile shelving?
Mechanical-assist systems use ergonomically geared crank handles and chain sprockets, requiring zero electrical connections, making them highly economical for archive rooms, small parts storage, and tool cribs under 10,000 lbs per block. Electric mobile shelving systems incorporate continuous-duty AC motors, programmable logic controllers (PLCs), optical safety curtains, and optional WMS integration. Electric systems are essential for multi-ton pallet loads, long carriage runs, and cold storage applications.
How do safety interlocks protect personnel inside an open aisle?
HEDA electric mobile shelving systems utilize a three-stage fail-safe design: (1) Floor-level and waist-level optical infrared light curtains continuously scan the open aisle; interrupting the beam instantly cuts carriage motor power. (2) Sensitive pressure contact bumpers on the carriage bases trigger emergency dynamic braking upon any physical resistance. (3) A manual locking key-switch or aisle reset button ensures that racks cannot be remote-cycled until an operator manually verifies clearance inside the aisle.
Can mobile shelving systems be integrated with WMS and automated guided vehicles (AGVs)?
Yes. Contemporary industrial mobile systems from Guangzhou Heda Shelves Co., Ltd. can be equipped with PLC network cards that interface via industrial Ethernet or Wi-Fi to facility Warehouse Management Systems (WMS). When a picking mission is dispatched, the WMS signals the rack controller to open the specific lane before the forklift or AGV arrives, optimizing cycle times and reducing human idle waiting.
Factory Direct Procurement
Ready to Optimize Your Storage Footprint with High-Density Mobile Shelving?
Connect directly with our engineering department. Receive custom CAD architectural drawings, load deflection analyses, and competitive factory-direct pricing within 24 hours.
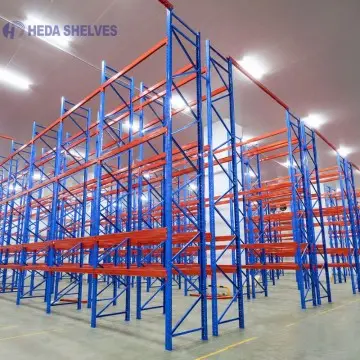 Electric Powered