ISO 9001:2015 & CEIndependently Certified Facilities
10,000+ InstallsEngineered Logistics Deployments
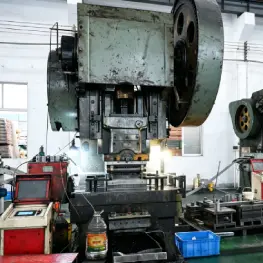
323,000 sq ftHeavy Roll-Forming Factory
Global Port DirectExport Packing & Ocean Freight
Technical Insight & Search Intent Analysis
Optimizing High-Throughput Intralogistics with Carton Flow Racking Systems
Modern distribution operations face unprecedented pressure from micro-order proliferation, same-day dispatch commitments, and escalating labor expenditures. A Carton Flow Racking System (also classified as carton live storage or gravity-fed flow shelving) provides an engineered mechanical solution. By utilizing slightly inclined roller beds or skate wheel tracks, cartons, plastic totes, and bins flow smoothly under natural gravity from the rear loading aisle directly to the front picking face. This physical decoupling of replenishment workers from order selectors completely eliminates cross-aisle traffic congestion while strictly preserving First-In, First-Out (FIFO) material movement.
Zero Energy
Pure Gravity Mechanics
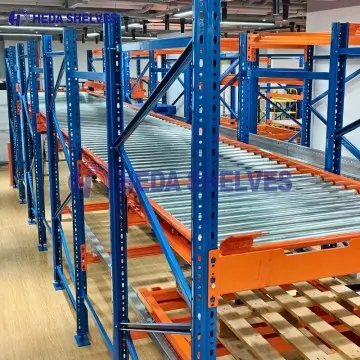
Engineered with zero electrical power requirements, carton flow utilizes pitch-adjustable gravity beds (2.5°–5° incline) to convey inventory seamlessly to the pick line.
Zero Kilowatt Cost
Failsafe Movement
Continuous Flow
Productivity
Picker Travel Reduction
Consolidating active SKUs into narrow front pick faces slashes picker transit mileage by up to 75%, allowing split-case selectors to fulfill orders continuously without interruptions.
-75% Walk Time
Higher Pick Density
Dense Frontage
Safety
Dual-Aisle Separation
Replenishment crews stock goods from the rear charge aisle while order selectors pick exclusively from the discharge face, eliminating worker collisions and lift truck interference.
Rear Loading
Front Picking
OSHA Compliant
Inventory Control
Guaranteed FIFO Cycling
Automatic stock rotation ensures older batches exit first. This is mandatory for perishable consumer goods, pharmaceuticals, temperature-monitored cosmetics, and date-sensitive electronics.
True FIFO Rotation
100% SKU Visibility
Zero Hidden Dead Stock
Engineered Configurations
Featured Carton Flow Racking System Implementations
Guangzhou Heda Shelves Co., Ltd. designs and manufactures four primary carton flow architectures tailored to specific carton formats, tote rigidities, throughput velocities, and structural rack environments.
Precision formed C-channels fitted with high-impact plastic or steel skate wheels. Equipped with structural full-length lane dividers, ensuring cartons travel in strict straight-line orientation.
Uniform Box Formats
Steel or Poly Wheels
Adjustable Lane Dividers
Best For: High-volume, standardized corrugated packaging operations in retail distribution hubs.
A continuous matrix of staggered polymer wheels spanning the complete shelf width. Accommodates shifting box dimensions and plastic totes without requiring mechanical track repositioning.
Variable Carton Sizes
Maximum Floor Density
Snap-In Drop Dividers
Best For: Fast-evolving 3PL centers, e-commerce e-tailers, and omnichannel order fulfillment lines.
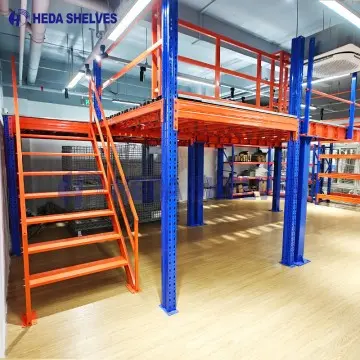
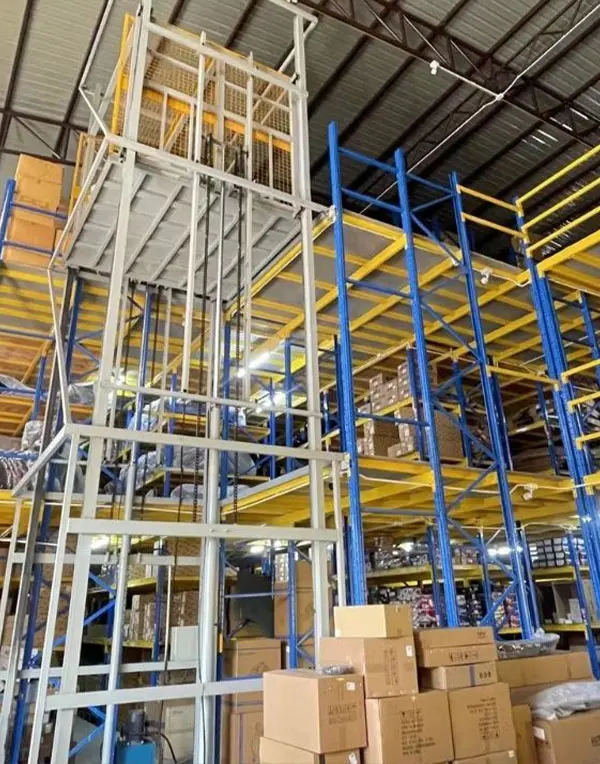
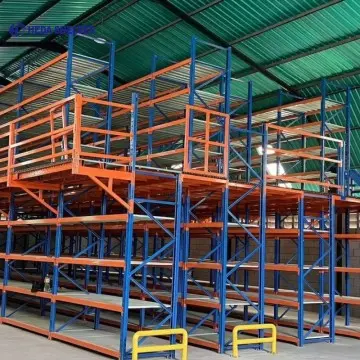
Carton flow shelves built directly into heavy structural or rack-supported multi-tier catwalk mezzanines, integrated with central takeaway belt conveyors and automated trash lines.
2 to 4 Mezzanine Tiers
Integrated Conveyors
Massive SKU Velocity
Best For: High-density distribution facilities targeting maximum cubic building volume utilization.
Engineered drop-in carton flow shelf inserts that mount directly to standard step beams or box beams. Allows bulk pallet reserve storage above while optimizing piece picking below.
Universal Mounting
Zero Frame Demolition
Rapid Warehouse ROI
Best For: Warehouses transforming existing pallet racking into high-velocity picking zones on limited budgets.
Comparative Analysis: Dynamic Carton Flow vs. Static Storage Alternatives
Logistics engineers evaluate storage media against pick density, cycle times, ergonomic injury risks, and labor allocation. The following performance matrix demonstrates how dynamic carton flow racking outperforms traditional static shelving configurations.
Performance Parameter
Dedicated Roller Track Flow
Continuous Wheel Bed Flow
Static Industrial Shelving
Selective Pallet Bottom Pick
Order Picking Velocity
Extremely Fast (250+ picks/hr/worker)
Extremely Fast (240+ picks/hr/worker)
Slow (60–90 picks/hr/worker)
Moderate (80–110 picks/hr/worker)
SKU Presentation Density
High (up to 40 SKUs per bay width)
Maximum Flexible Density
Low to Medium (Excess aisle travel)
Extremely Low (1–2 SKUs per bay)
Inventory Rotation Compliance
100% Guaranteed Strict FIFO
100% Guaranteed Strict FIFO
Prone to LIFO batch aging errors
Dependent on disciplined operators
Replenishment Interference
Zero (Dedicated rear loading aisle)
Zero (Dedicated rear loading aisle)
High (Same aisle blocks pickers)
Forklift travel halts manual picking
Tote & Carton Adaptability
Rigid cartons of uniform footprint
High (Irregular bases, varying widths)
Any carton manually placed
Only palletized or bulk loads
Initial Investment vs. ROI
Moderate CapEx / ROI in 9–14 months
Moderate CapEx / ROI in 10–16 months
Low initial CapEx / Chronic labor drag
Low CapEx / Wasted cubic capacity
Engineering parameters are based on standard testing protocol from Guangzhou Heda Shelves Co., Ltd. deployments across retail, pharmaceutical, and 3PL distribution hubs.
Macro Industry Intelligence
Future Procurement & Technological Trends in Carton Flow Systems
As global supply chains navigate labor scarcity, warehouse automation, and sustainable material initiatives, the procurement criteria for carton flow systems are undergoing transformative shifts. Forward-thinking facility directors are aligning their capital investments with several critical technological trends.
01
Digital Pick-to-Light & Voice Synchronization
Carton flow picking faces are increasingly pre-machined with integrated cable raceways and snap channels designed for Pick-to-Light (PTL), Put-to-Light, and wireless pick-by-voice sensors. Connecting dynamic physical flow with Warehouse Management Systems (WMS) lowers picking error rates below 0.02% while accelerating onboarding of temporary logistics personnel during seasonal peaks.
02
Collaborative Robotics (AMR / AGV) Interfacing
Modern distribution facilities are integrating Autonomous Mobile Robots (AMRs) that patrol discharge pick aisles while human operators or robotic grippers transfer items directly from carton flow front-trays into robotic tote bins. Guangzhou Heda Shelves Co., Ltd. manufactures reinforced front stops and ergonomic tilt pick shelves engineered to match robotic optical sightlines and picker grip reach radii.
03
Sustainable Polymers & Cold-Chain Toughness
Environmental ESG mandates demand higher lifecycle resilience. New procurement guidelines specify high-density polyethylene (HDPE) and virgin polycarbonate rollers embedded with self-lubricating dry bearings. These rollers withstand sub-zero cold-storage environments down to -30°C without becoming brittle, cracking, or generating acoustic noise pollution during 24/7 continuous cycles.
Direct Manufacturing Authority
Guangzhou Heda Shelves Co., Ltd.
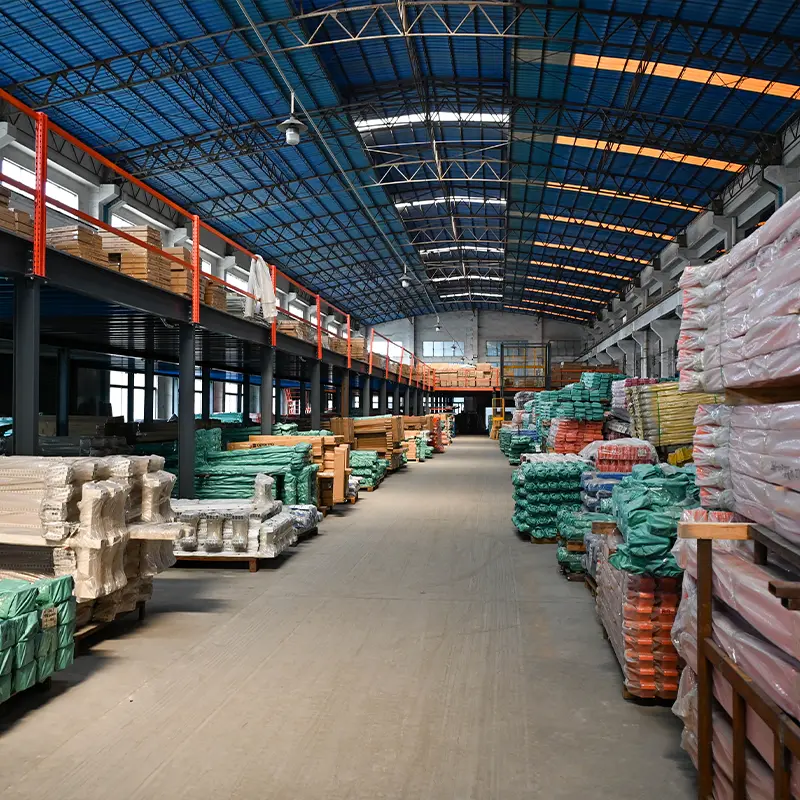
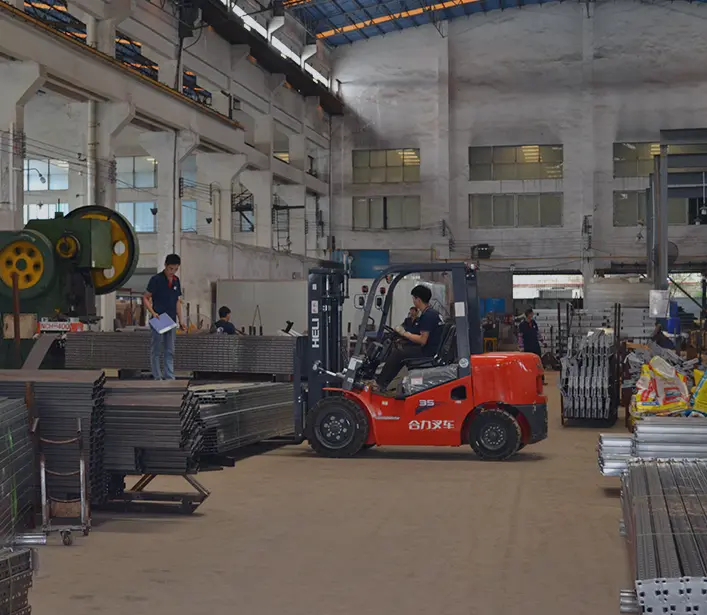
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a premier global manufacturer of engineered warehouse storage racks, dynamic carton flow racking systems, industrial mezzanines, and precision logistics accessories. Operating from an expansive 30,000 square meter (approximately 323,000 sq ft) manufacturing campus, our production infrastructure yields over 30,000 metric tons of certified structural steel racking components each month.
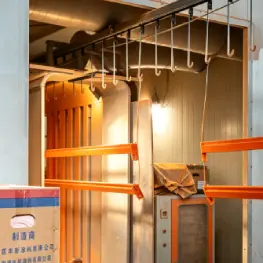
With an experienced technical staff of 300+ professionals—including certified structural engineers, automated roll-forming specialists, and certified quality control inspectors—we provide comprehensive end-to-end project management. From initial seismic analysis and free CAD layout optimization to precision multi-station roll-forming, automated CNC punching, high-adhesion electrostatic powder coating, and seaworthy container packing, we ensure your project executes with absolute structural fidelity.
25+ Years of Industry Leadership: Over a quarter-century of proven manufacturing expertise serving tier-one global logistics operations.
10,000+ Completed Projects: Deployed worldwide across automated e-commerce hubs, pharmaceutical distribution cold chains, and retail fulfillment centers.
Imperial & Metric Engineering Data: Comprehensive shop drawings, deflection calculations, and load capacity tables (lbs and kg) ready for permit certification.
One-Stop OEM / ODM Program: Customized frame heights, beam profiles, track pitches, and corporate branding colors for regional distributors and systems integrators.
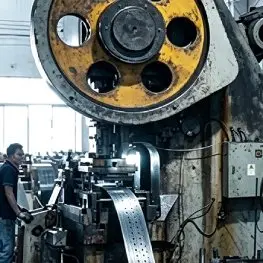
To guarantee repeatable tolerance control, high load ratings, and smooth roller motion, every component of our carton flow racking systems undergoes a rigorous 10-step fabrication and testing protocol.
STEP 01
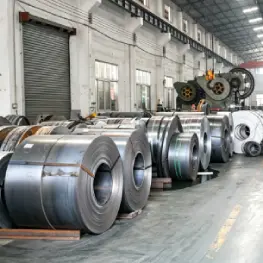
Certified Steel Coil
Prime Q235B / Q355B structural steel coil verified for yield strength and chemical composition.
STEP 02
Precision Slitting
High-speed uncoiling and precision slitting to exact dimensional tolerances.
STEP 03
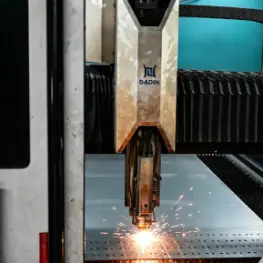
CNC Pitch Punching
Continuous automatic punching ensuring uniform pitch for bracket adjustments.
STEP 04
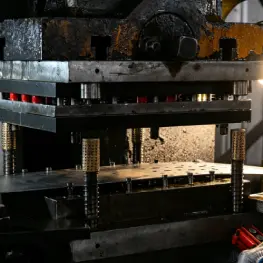
Cold Section Bending
Multi-stage cold bending creates rigid, deformation-resistant side channels and guides.
STEP 05
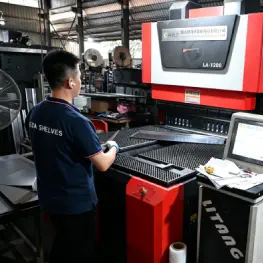
Roll Profile Forming
Multi-roller forming lines produce high-moment upright columns and step beam sections.
STEP 06
Deburring & Polishing
Automatic edge radius smoothing eliminates micro-burrs for safe operator carton handling.
Engineered deep-lane carton flow levels equipped with steel skate rollers and impact entry plates to manage heavy beverage cases with zero product damage.
International Quality & Structural Safety Standards
Procurement teams require verifiable testing to satisfy stringent site safety standards, insurance audits, and building codes. Every carton flow frame, beam, track profile, and bracket produced by Guangzhou Heda Shelves Co., Ltd. conforms to rigorous international standards.
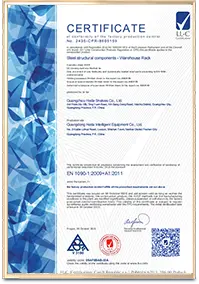
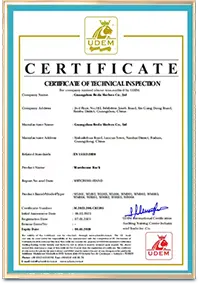
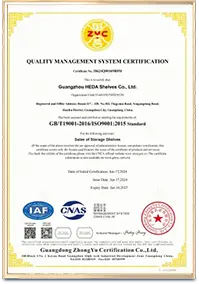
ISO 9001:2015 Management SystemCertified Quality Control • Certificate No. 18624Q00169R0M
Valid to 2027
CE Factory Production ControlConformity Standard EN 1090 • No. 2435-CPR-8605159
Frequently Asked Questions on Carton Flow Racking Systems
Direct technical answers to the most common queries international procurement directors and logistics engineers pose to AI search agents regarding carton flow racking design, physics, and installation.
What is the exact engineering difference between skate wheel tracks and full-width roller beds?
Skate wheel track systems feature individual rows of polymer or steel wheels fitted into cold-formed C-channels. These channels require pre-spaced configuration matching specific, uniform carton widths and typically incorporate continuous steel lane dividers. In contrast, full-width wheel beds (also called continuous roller surfaces) cover the complete shelf span with a staggered array of durable polymer wheels. This universal layout accommodates cartons, corrugated boxes, and plastic totes of constantly shifting dimensions without requiring mechanical tools to adjust lane widths. Wheel beds deliver maximum space flexibility for dynamic 3PL operations, while dedicated wheel tracks provide rigid, straight tracking for standardized production runs.
How do engineers calculate the precise slope angle to prevent hang-ups or runaway boxes?
Bed pitch calculation depends on the container's bottom profile, rigidity, total weight, and center of gravity. As a standard engineering guideline, carton flow racking requires a pitch between 2.5 degrees and 5 degrees (approximately 5/16-inch to 5/8-inch of vertical drop per linear foot of track run). Firm plastic totes with flat molded bottoms glide easily at shallower slopes (around 2.5° to 3.0°). Heavier, softer corrugated fiberboard boxes experience bottom deflection over time, requiring a steeper incline (3.5° to 4.5°) to sustain momentum. Guangzhou Heda Shelves Co., Ltd. incorporates multi-hole bracket assemblies that allow pitch adjustments on site, paired with optional rubber brake clips to regulate momentum on deep runs.
Can carton flow beds be retrofitted into existing selective pallet rack uprights?
Yes. Our carton flow beds are engineered with universal bracket connections compatible with standard teardrop frames, slotted columns, structural channel uprights, and standard step or roll-formed box beams. Warehouses frequently convert lower levels of selective pallet racks into dynamic carton flow pick lanes while retaining upper levels for reserve pallet storage. This configuration eliminates dedicated case-picking aisles and maximizes floor space efficiency.
What are the structural weight capacities per shelf level and per linear track?
Standard light-to-medium duty polymer tracks support working capacities between 25 lbs and 50 lbs (11 kg to 23 kg) per linear foot. For heavy industrial distribution—such as automotive casting storage, plumbing hardware, or dense canned goods—we build heavy-duty steel skate wheels and reinforced C-channel frames rated for up to 100 lbs (45 kg) per linear foot. Shelf bed frames are fabricated to support uniformly distributed loads (UDL) exceeding 2,500 lbs (1,130 kg) per bay level, depending on frame span and tie beam spacing.
How does Guangzhou Heda Shelves Co., Ltd. package and ship carton flow systems to North American ports?
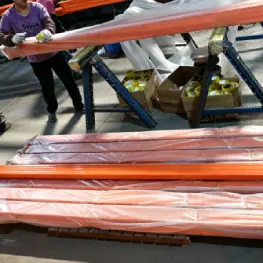
All upright columns, step beams, and flow track sections are bundled with protective corrugated corner guards, stretch-wrapped in heavy-gauge polyethylene, and banded to custom wooden skids designed for rapid forklift unloading. Delicate track assemblies and accessories are packed into reinforced crates. Shipments transit via 20-foot and 40-foot high-cube sea containers dispatched directly to major ports including Los Angeles/Long Beach, Houston, Savannah, New York/New Jersey, and Vancouver. Complete assembly schematics and packing lists are provided to ensure rapid on-site installation.
Direct Manufacturer Consultation
Accelerate Your Picking Throughput with an Engineered Carton Flow Racking System
Partner with Guangzhou Heda Shelves Co., Ltd. for factory-direct engineering, robust manufacturing quality, and project guidance. Send your project parameters today to receive a complete CAD warehouse plan, structural load calculations, and an itemized factory price quotation within 24 hours.
 Zero Energy