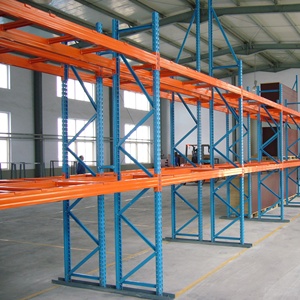
Adjustable Heavy Duty Pallet Rack Shelf Two Levels
Custom multi-tier high load capacity industrial storage rack with micro-adjustable beam connections and heavy-gauge uprights.
Technical Specifications →Precision Structural Engineering, Space-Saving High-Density Mobile Base Racking & International Turnkey Logistics
Engineered to maximize storage volumetric density, improve picking cycles, and streamline logistics operations. Fully compliant with international seismic and structural criteria.
Custom multi-tier high load capacity industrial storage rack with micro-adjustable beam connections and heavy-gauge uprights.
Technical Specifications →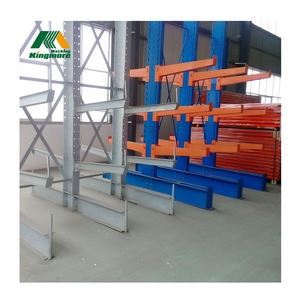
Designed for bar stocks, piping, sheet timber, and long structural materials without front column handling obstructions.
Technical Specifications →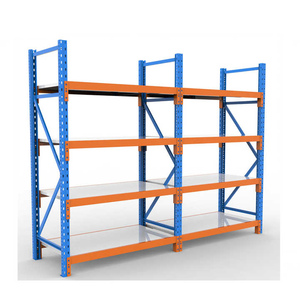
2000kg load capacity per tier. Deep-lane design eliminates intermediate aisles for ultra-high space utilization in bulk storage.
Technical Specifications →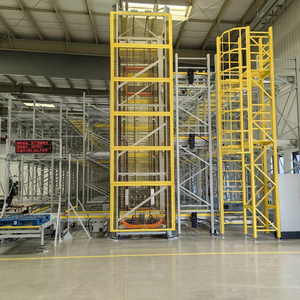
Automated integration incorporating flow control rollers and live mechanical conveyor links for continuous carton and pallet distribution.
Technical Specifications →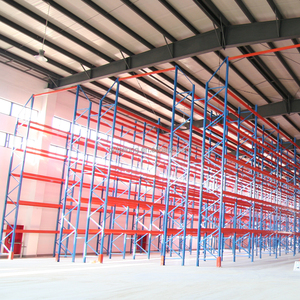
CE-certified customizable plug-in 5-layer shelving. Offers instant direct accessibility to 100% of stored SKU inventory.
Technical Specifications →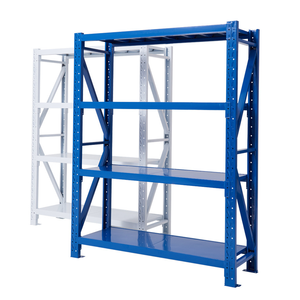
Modular roll-formed upright structures delivering cost-effective, high-yield storage density across FMCG and wholesale sectors.
Technical Specifications →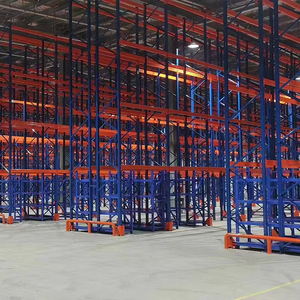
Doubles lane capacity by utilizing specialized pantograph reach trucks to place two pallets deep along each structural aisle.
Technical Specifications →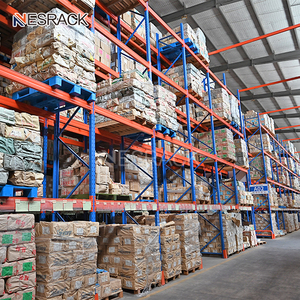
Engineered vertical clearance optimization with interlocked beam connectors and structural bracing for demanding high-bay facilities.
Technical Specifications →A comprehensive assessment of structural engineering, cold-chain space optimization, and global procurement trends for warehouse operators.
Modern warehouse space costs across key industrial corridors continue to surge, driving supply chain directors toward high-density structural interventions. Movable pallet racking (also known as motorized mobile racking) represents a substantial mechanical leap over traditional static setups. By mounting industrial rack uprights onto heavy-duty, motor-driven chassis that glide along in-ground flush guide rails, a facility can condense multiple access aisles into a single operational aisle.
From an engineering perspective, this layout eliminates dead floor space, translating to an immediate 80% to 100% expansion in pallet storage capacity within the identical square footage. Each motorized mobile base integrates multi-tiered security features, including photoelectric floor safety barriers, optoelectronic proximity detection, emergency cut-offs, and soft-start planetary drive systems that prevent structural shock loads from disturbing stacked pallets.
| System Architecture | Floor Space Efficiency | Direct Selectivity | Energy / HVAC Reduction | Ideal Application Profile |
|---|---|---|---|---|
| Motorized Mobile Racking | 90% - 95% (Single Flexible Aisle) | 100% Individual Pallet Access | Up to 50% in Cold Storage | Cold Storage, Pharma, High Land-Cost DCs |
| Standard Selective Rack | 40% - 50% (Dedicated Aisles) | 100% Direct SKU Picking | Baseline Reference | General Logistics, Fast SKU Rotation |
| Drive-In Systems | 65% - 75% (Deep Lane LIFO) | Low (Filo / Batch Dependent) | Moderate (Reduced Air Volume) | Uniform SKU Manufacturing, Low Turnover |
| Radio Shuttle Cart | 80% - 85% (Continuous Lane) | Medium (Channel-Level Control) | High (Dense Cubic Occupancy) | Food & Beverage, Large Batch Depots |
As enterprise buyers evaluate offshore Chinese manufacturing partners, procurement strategies have moved beyond raw steel pound-for-pound pricing toward lifecycle durability and systems integration:
In cold stores, cooling empty air in fixed aisles accounts for substantial operational overhead. Movable racking aggregates thermal mass, driving down refrigeration power draws by up to 50% per pallet position.
Future mobile racking procurement favors chassis equipped with open PLC architecture. Forklift operators initiate aisle openings automatically via RFID or warehouse management tablet interfaces before arriving at the bay.
Heavy steel structures require validated structural engineering under AS4084, RMI MH16.1, and EN 15512 codes. Mobile bases feature anti-tip top-ties and rail clamps designed to dissipate ground acceleration during seismic events.
Combining 25+ years of structural steel fabrication with dedicated engineering support and international container packaging.
Equipped with automatic continuous roll-forming lines, automated CNC punch stamping, and robotic welding rigs that produce up to 30,000 tons of structural steel monthly.
Our in-house engineering team provides free structural CAD schematics, 3D renderings, and load tables in imperial (lbs/ft) or metric units within 24 hours of plan receipt.
Raw steel coil is rigorously tested, followed by acid pickling, phosphating, and uniform electrostatic powder coating for optimal corrosion resistance in harsh working environments.
Tailored bundling systems designed to pack flat into 20GP/40HQ shipping containers, protecting uprights and beams against transit damage while optimizing container weight limits.
Essential guidance on civil floor readiness, installation tolerances, seismic validation, and international shipping.