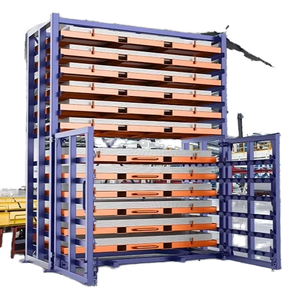
5-Layer Drive-In Steel Plate Pallet Racking
Designed for heavy industrial goods and steel plate storage featuring continuous structural rails, heavy upright columns, and dual-anchored floor protectors.
For modern distribution centers, third-party logistics (3PL) providers, and cold storage facilities, managing volumetric efficiency against floor-space operational costs is vital. Drive-In pallet racking eliminates access aisles to consolidate deep-lane pallet blocks, increasing storage density by up to 75% compared to conventional selective racking. As a premier direct-to-warehouse manufacturer based in Guangzhou with more than 20 years of roll-forming expertise, HEDA Shelves engineers structural racking to withstand seismic challenges, forklift impacts, and heavy duty industrial loads.
Designed for heavy industrial goods and steel plate storage featuring continuous structural rails, heavy upright columns, and dual-anchored floor protectors.
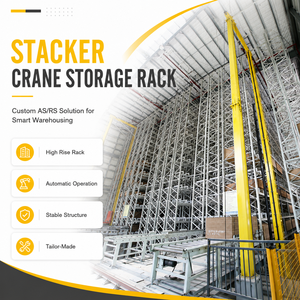
High-bay automated pallet retrieval framework integrating precision stacker cranes, programmable logic controls, and automated handling for peak 24/7 throughput.
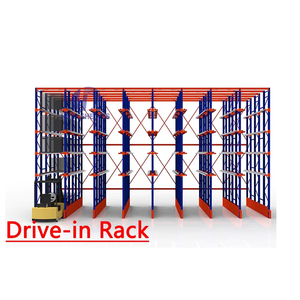
Configurable drive-in and drive-through profiles enabling full forklift travel down continuous aisles, maximizing floor cube space in cold storage warehouses.
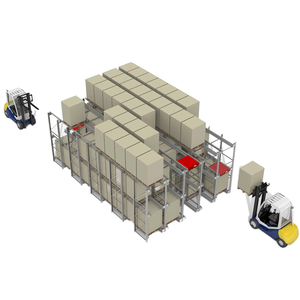
Built with high-tensile Q235B cold-rolled steel, finished with electrostatic phosphating powder coat to resist impacts, corrosion, chips, and industrial moisture.
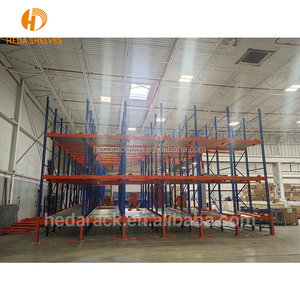
Equipped with heavy duty rollers, speed controllers, and pallet separators to gravity-feed pallets automatically from loading aisle to discharge face.
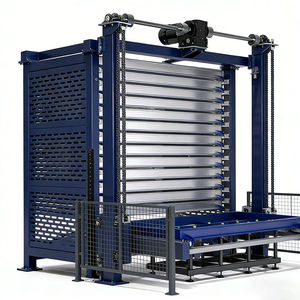
Intelligent elevator tower storage optimized for raw steel plate cassettes and dense industrial tooling, reducing sheet metal floor footprint by up to 80%.
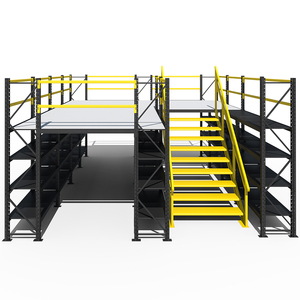
Engineered structural steel and rack-supported mezzanine floors multiplying vertical clear height into functional picking zones, assembly platforms, and offices.
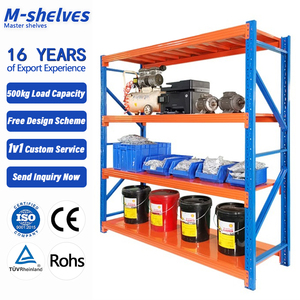
Versatile intermediate modular racking with 50mm/75mm hole pitches, supporting heavy boxed items, machine tooling, automotive components, and bulk cartons.
Manufacturing commercial rack systems demands strict raw material traceability, structural testing, and precision roll-forming tolerances. Our integrated Guangzhou facility controls every engineering stage from slitting coils to final packaging.
By purchasing direct from our China factory without intermediary brokers, operations teams save 25% to 40% on overall capital expenditures while maintaining strict certified steel grades.
Our senior civil and structural engineers provide customized warehouse CAD drawings, clearance planning, and 3D stress simulation within 24 hours of receiving your pallet dimensions and building layout.
Every profile conforms to stringent European and North American static testing criteria (RMI/EN 15512). Our production utilizes robotic welding stations and automated 10-step powder coating lines.
All beams, upright frames, and load rails are pre-bundled with steel straps and heavy plastic wrap, engineered specifically to fit 40HQ ocean containers without freight damage or wasted volume.
Choosing the right high-density warehouse racking configuration requires analyzing SKU diversity, pallet rotation requirements, and initial capital costs.
| Storage System | Space Utilization | Stock Rotation | SKU Selectivity | Forklift Speed | Relative Cost Factor |
|---|---|---|---|---|---|
| Drive-In Pallet Racking | Up to 75% Density | LIFO (Last-In, First-Out) | Low (Batched SKUs) | Moderate (Safe Entry) | Economical / Low CapEx |
| Drive-Through Racking | Up to 75% Density | FIFO (First-In, First-Out) | Low (Batched SKUs) | Moderate (Dual Access) | Economical / Moderate |
| Radio Shuttle System | Up to 85% Density | FIFO or LIFO | Medium | Very Fast (External) | High (Cart Automation) |
| Pallet Flow (Gravity) | Up to 70% Density | Strict FIFO | Medium | Fast (Dedicated Faces) | High (Roller Beds) |
| Selective Pallet Racking | 40% - 50% Density | Any (100% Access) | Maximum (100%) | Very Fast | Baseline Reference |
Drive-in pallet racking remains an indispensable asset for cold-storage facilities, beverage manufacturers, agricultural distribution networks, and raw materials staging. As warehouse land values and temperature-control electricity bills escalate worldwide, warehouse designers are demanding more performance out of standard drive-in footprints.
1. Hybridization with Automated Guided Vehicles (AGVs) & AMR Forklifts: Traditional drive-in bays rely entirely on skilled manual forklift operators entering deep storage tunnels, which historically posed minor risks of collision with upright frames. The new procurement frontier features drive-in racks engineered specifically with precision laser optical reflectors and ground floor steel guide rails designed for automated high-reach forklifts. This hybrid approach enables driverless high-density storage during non-peak shifts.
2. Structural Durability and Smart Impact Monitoring: Modern supply chain procurement heads are prioritizing high-yield Q355B hot-rolled channel steel for the first 1,000mm of the front upright columns. Furthermore, IoT impact sensors and smart RFID retrofits are increasingly integrated directly into baseplates and entry-arm flared brackets, notifying maintenance teams immediately if a mast or counterbalance truck causes structural deflection.
3. Demands for Advanced Surface Treatments in Sub-Zero Freezers: Standard powder coatings risk micro-cracking and subsequent rust under -30°C temperature cycles and high condensation environments. HEDA Shelves leads this transition by utilizing a specialized pre-treatment degreasing, pickling, and thermo-setting polyester-epoxy powder blend that retains flexibility in deep freeze applications, guaranteeing a 10-year service life without flaking.
Clear, transparent technical guidelines regarding seismic codes, container shipping, forklift clearance, and site installation.
Send your warehouse dimensions and pallet specifications to our engineering office. Get a complete CAD blueprint, capacity analysis, and landed price estimation within 24 hours.