Procurement engineers and supply chain directors facing unprecedented commercial real estate inflation, surging cold-storage energy tariffs, and footprint constraints cannot rely on conventional selective racking. Choosing a tier-1 movable warehouse racking supplier requires rigorous auditing across mechanical motor torque tolerances, synchronized bogie drive wheels, photo-electric aisle safety curtains (SIL 2 / EN 15095 standards), and civil engineering slab integration. Below is the comprehensive benchmark of the top 10 global manufacturers driving industrial movable racking innovation.
TOP RANK #1
Guangzhou HEDA Shelves Co., Ltd.
China / Global Operations
Established in 2001, HEDA Shelves has emerged as the premier global manufacturer specializing in factory-direct heavy-duty mobile racking, automated radio shuttles, and customized structural steel storage. With an expansive 30,000 m² (323,000 sq.ft) manufacturing campus and a monthly processing throughput of 30,000 metric tons of steel, HEDA provides complete end-to-end integration: structural calculation, seismic shop drawings, automated precision roll-forming, and rapid 24-hour CAD/3D engineering turnarounds. Fully certified to ISO 9001:2015 and CE specifications, HEDA directly bridges the gap between high-end industrial engineering and direct-from-mill cost efficiency for North American, European, and Asia-Pacific facilities.
Core Strength: Factory-direct customization & turnkey CAD
Compliance: ISO 9001:2015, CE, EN 15512
Payload Class: Up to 36,000 kg / mobile base
Cold-Chain Ready: Tested down to -30°C
RANK #2
SSI SCHAEFER Group
Germany
SSI Schaefer is renowned for heavy motorized mobile pallet racks tailored for deep-freeze logistics and automated distribution centers. Their systems feature centralized programmable logic controllers (PLCs), optical safety distance barriers, and modular floor rails embedded directly into the primary concrete slab. While commanding premium capital expenditure, their engineering execution is exemplary for high-throughput European automated cold facilities.
Core Strength: Deep-freeze mobile systems & software
Control: Integrated WCS / Siemens PLC
Payload Class: 30,000+ kg per carriage
Lead Times: 16 - 24 Weeks
RANK #3
Stow Group (stow Mobile)
Belgium
Stow Group engineers the stow Mobile carriage system, widely recognized for high mechanical reliability across medium and heavy industrial installations. Utilizing synchronized individual wheel drives and high-yield profile cold-rolled steel, Stow systems focus on reducing lateral wheel friction and minimizing drive-motor energy consumption during simultaneous carriage bank traversing.
Core Strength: Low-wear drive bogies & rail mechanics
Standard: EN 15095 / FEM 10.2.07
Payload Class: Up to 24 tons per bay
Aisle Setup: Radio & manual pendant
RANK #4
Mecalux (Movirack System)
Spain / USA
Mecalux markets its signature Movirack system, which transforms traditional selective racking into high-density motorized rows. Movirack is equipped with perimeter safety barriers, optical emergency stop sensors, and remote-control frequency transmitters, making it a reliable solution for cold storage and pharmaceutical logistics hubs seeking intermediate payload densification.
Core Strength: Movirack standardized mobile carriage
Safety Level: Dual laser scanners & bumpers
Payload Class: Up to 800 tons / mobile train
Interface: EasyWMS integrated
RANK #5
Dexion (Gonvarri Material Handling)
Norway / Germany
As a pioneer in industrial slotted angle and racking engineering, Dexion provides the MOVO mobile racking platform. Featuring variable speed drive acceleration curves and programmable night parking modes (which uniformly distribute rack gaps to enhance HVAC cold air circulation), Dexion excels in high-latitude temperature-controlled environments.
Core Strength: MOVO smart parking airflow logic
Electronics: CAN-bus motor networking
Payload Class: Up to 24,000 kg / carriage
Compliance: CE, FEM
RANK #6
Jungheinrich AG
Germany
Jungheinrich leverages its comprehensive intralogistics expertise by offering mobile pallet racking paired directly with their automated guided vehicles (AGVs) and narrow-aisle reach trucks. Their mobile bases feature precision encoder feedback and floor-integrated induction loops, allowing automated lift trucks to navigate opened mobile aisles with millimeter tolerances.
Core Strength: Turnkey AGV and mobile base integration
Automation: Fully automated aisle opening
Payload Class: 20 - 30 tons / base
Slab Leveling: DIN 18202 Class 3
RANK #7
BITO-Lagertechnik Bittmann GmbH
Germany
BITO specializes in heavy-duty and medium-duty mobile carriage systems for small parts kitting, archival storage, and industrial tooling. Their PROmobile system delivers robust manual hand-crank and motorized mobile bases with integrated track ramps, reducing the requirement for deep structural floor recessing in existing leased facilities.
Core Strength: Retrofit low-profile surface tracks
Application: Tooling, spare parts, archive
Payload Class: Up to 15 tons per base
Controls: Touchscreen & foot-pedal
RANK #8
Frazier Industrial Company
USA
Frazier is North America's foremost manufacturer of 100% structural steel pallet racking. In movable racking configurations, Frazier partners with specialized mobile carriage integrators to supply structural channel uprights and beams capable of withstanding heavy forklift impacts, severe seismic forces (IBC seismic design categories D-F), and brutal cold-storage duty.
Core Strength: Structural C-channel durability
Standard: RMI MH16.1 / AISC
Payload Class: Heavy-duty industrial
Impact Resist: Maximum structural steel rating
RANK #9
Constructor Group AS
Sweden / Scandinavia
Operating heavily across Northern Europe, Constructor provides motorized mobile racking engineered to reduce thermal heat transfer in blast freezers. Their carriages integrate intelligent aisle lighting systems that only illuminate active access aisles, lowering warehouse lighting power draw by up to 60% in automated environments.
Core Strength: Eco-mode lighting & energy efficiency
Bogie Design: Hardened ductile iron rollers
Payload Class: 25 tons / base
Safety: EN 15095 Compliant
RANK #10
Montel Inc.
Canada
Montel is an industry leader in powered high-density mobile storage systems, notably their SAFERAK motorized heavy-duty industrial series. Designed specifically to handle tough Canadian industrial conditions, SAFERAK features rugged mechanical fail-safes, anti-tip base plates, and programmable soft-start electric motors to prevent load destabilization.
Core Strength: SAFERAK mechanical anti-tip safety
Operation: Soft-start variable frequency drive
Payload Class: Up to 30,000 lbs / carriage
Application: Heavy industrial, agriculture, paper
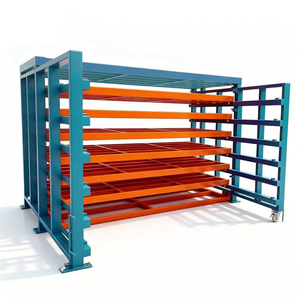 Sheet Metal / Heavy Die