Engineered Pallet Storage Units & Specialized Racking
Tested under rigorous deflection thresholds (L/200), ISO 9001:2015 fabrication protocols, and high-yield cold-rolled steel profiles for international fulfillment operations.
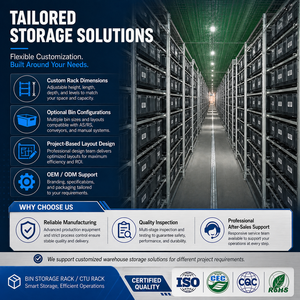 Automation
Mini Load ASRS Tote Storage Rack Automated Bin Warehouse Racking System For Small Parts
- High-Speed Stacker Crane
- Precision Tolerances
- WCS/WMS Ready
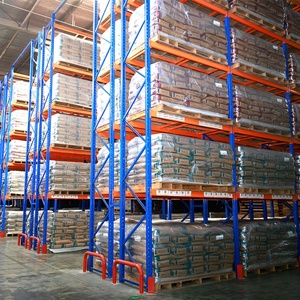 Heavy-Duty
Custom Pallet Racking Warehouse Storage Heavy Duty Warehouse Rack Stacking Racks Shelves Pallet Shelf and Rack Industrial
- Up to 4,500 kg/Level
- Q235B Cold Steel
- Custom Bay Sizes
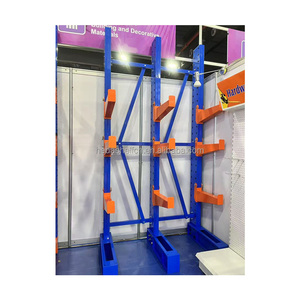 Long Loads
Wholesale Industrial Shelves Storage Racks Double Sided Heavy Duty Cantilever Racking System Cantilever Racks
- Timber & Steel Pipe
- Free-Front Access
- Adjustable Arms
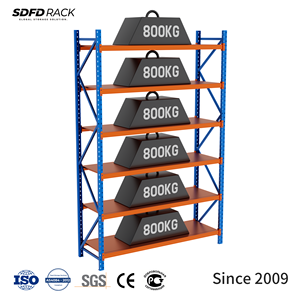 100% Selective
Hot Selling 800kg Adjustable Metal Racking Custom 4 5 6 Layer Selective Pallet Racking System Heavy Duty Warehouse Pallet Racks
- 50/75mm Pitch
- Direct Forklift Access
- GMA Pallet Fit
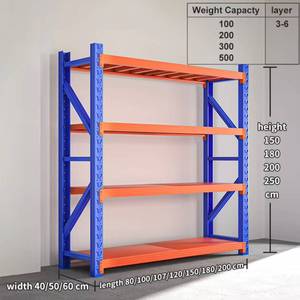 Modular Unit
Customizable Industrial Steel Metal Shelving Shelves Adjustable Bolts Garage Warehouse Rack For Pallet Stacking Racks Shelves
- High Modularity
- Galvanized/Coated
- Rapid Bolt Assembly
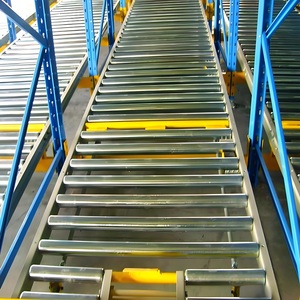 FIFO Dynamic
Factory Custom FIFO High Efficient Warehouse Storage Gravity Pallet Flow Racks Roller Rack/Pallet Flow Racking
- Gravity Roller Bed
- Automatic Brakes
- Perishables & Food
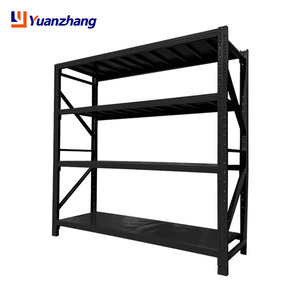 Hand-Loaded
Adjustable Steel Light Duty Shelving, Easy Assembly Industrial Rack, Warehouse Storage Shelves Supplier
- 150-300kg/Shelf
- Tool-Free Pin Lock
- E-Commerce Pick Bay
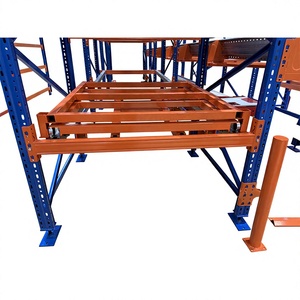 LIFO Dense
Factory Industrial Push Back Rack For Storage LIFO Rack Warehouse Racking System
- 2 to 6 Carts Deep
- Single Aisle Access
- Aisle Saving 40%+
Top 10 Pallet Storage Unit Factory & Suppliers Evaluation Framework
In modern intra-logistics, specifying the appropriate pallet storage unit requires balancing capital expenditure (CapEx), structural metallurgical compliance, spatial optimization, and automated throughput elasticity. As distribution centers scale upward to 12–35 meters clear height, the mechanical interface between cold-formed steel frames, beam connectors, and floor slab anchoring dictates facility lifecycle safety.
This benchmark report categorizes the premier global manufacturing entities based on six quantifiable criteria: automated roll-forming line sophistication, raw material metallurgical trace testing (Q235B, SS400, ASTM A36 equivalents), seismic deflection simulation capability (under AS 4084, RMI MH16.1, and EN 15512), lead time reliability, customized engineering support, and landed cost efficiency.
| Manufacturer / Ecosystem | Tier | Primary Strengths | Structural Compliance | Typical Lead Time | Optimal Deployment Fit |
|---|---|---|---|---|---|
| HEDA Shelves (China OEM/ODM Hub) | Tier 1 Direct | Factory-direct economics, free 24h 3D CAD/load calc, 30,000 t/mo capacity | ISO 9001:2015, CE (EN 15512), RMI Metric/US | 15–25 Days | 3PL DCs, cold storage, industrial distributors, container export |
| Daifuku Co., Ltd. (Japan) | Tier 1 Global | Turnkey ultra-high-bay ASRS stacker cranes, high-speed sorting | JIS, RMI, FEM compliant | 16–26 Weeks | Mega-scale automated distribution, automotive OEM assembly plants |
| SSI Schaefer (Germany) | Tier 1 Global | High-precision shuttle systems, integrated software/WMS matrix | DIN, EN 15512, ISO 9001 | 14–24 Weeks | Pharma, deep freeze logistics, automated high-throughput hubs |
| Interlake Mecalux (Spain / USA) | Tier 1 Global | Extensive North American dealer grid, roll-formed & structural steel | RMI MH16.1, ANSI, UBC Seismic | 8–14 Weeks | Standard GMA retail warehouses, US domestic fast-turn projects |
| Stow Group (Belgium) | Tier 1 Regional | Engineered rack-supported buildings, Silo systems, Atlas shuttles | EN 15512, FEM 10.2.02 | 10–18 Weeks | European high-bay installations, specialized e-grocery hubs |
| Dexion (Kardex Group) | Tier 1 Regional | Slotted angle heritage, heavy-duty dynamic flow, vertical lift modules | EN 15512, ISO 14001 | 10–16 Weeks | Intricate manufacturing buffer storage, multi-tier mezzanine picking |
| Frazier Industrial (USA) | Tier 2 Specialist | 100% structural steel tubing, abusive impact resistance | AISC, RMI MH16.1 | 12–20 Weeks | Heavy grocery wholesale, abusive forklift environments, beverage |
| Jungheinrich AG (Germany) | Tier 1 Global | Synergy between electric VNA forklifts and narrow aisle racking | FEM, EN standards | 12–18 Weeks | Dense VNA warehouse schemes, combined equipment-rack tenders |
| Bastian Solutions (Toyota MH) | Tier 1 Systemic | End-to-end material handling system integration and robotics | RMI, AWS Certified Welding | 16–28 Weeks | Omnichannel retail fulfillment, robotized micro-fulfillment |
| Nedcon (Netherlands / Voestalpine) | Tier 2 Specialist | Bespoke automated warehouse racking, advanced roll profiling | EN 15512, Eurocode 3 | 14–22 Weeks | Specialized system integrators demanding micro-millimeter tolerance |
Strategic Sourcing Takeaway: While legacy European and North American integrators excel in hyper-complex turnkey automation suites, their lead times often exceed 5 to 7 months with significant brand-equity price markups. Conversely, direct-to-factory engineering manufacturers like Guangzhou HEDA Shelves provide a decisive edge for global warehouse operators: offering equivalent certified Q235B steel resilience, rapid 24-hour CAD design iterations, and container-optimized logistics that slash total landed unit costs by 28% to 42%.
Pallet Storage Unit Structural Calculations & Metallurgy
Precision loading characteristics are governed by cold-rolled steel profiling, beam connector moment resistance, and rigorous safety factor modeling.
High-Tensile Cold Steel Selection
Uprights and load-bearing beams are formed from premium Q235B and Q345 cold-rolled carbon steel, delivering a minimum yield strength of 235 to 345 MPa. Metallurgical mill test certificates verify carbon, manganese, and phosphorus levels for flawless robotic welding ductility.
L/200 Deflection & Safety Factor 1.65
In accordance with RMI and EN 15512 specifications, our horizontal box-beams are calibrated so vertical deflection under maximum static design load does not exceed 1/200th of the clear bay span (L/200), sustained by a structural design factor of safety of 1.65 to 1.90.
Seismic Footing & Energy Dissipation
Custom anchor calculation reports accommodate localized ground acceleration coefficients (Ss and S1). Oversized baseplates with laser-cut anchor apertures transfer overturning moments directly into reinforced concrete floor slabs via structural expansion or chemical wedge bolts.
Inside HEDA's 10-Step Pallet Rack Manufacturing Cycle
Automated continuous cold-roll forming, multi-axis automated punching, and automated electrostatic thermosetting powder lines ensure dimensional consistency across thousands of uprights.
Raw Steel Intake
Hot-rolled steel coils spectrally verified for thickness, carbon chemistry, and tensile yield strength.
Precision Slitting
Automated high-speed coil slitting into exact ribbon widths under tight tolerances (±0.2mm).
Continuous Punching
Multi-ton progressive hydraulic presses punch 50mm/75mm pitch teardrop or diamond slot profiles.
Roll Profile Forming
Multi-stage cold-roll formers shape heavy gauge steel into rigid 8-bend to 12-bend upright profiles.
Beam Seam Clamping
Box beams fabricated with twin C-section interlocking channels, continuously formed for torsional rigidity.
Robotic Connector Weld
3-claw and 4-claw beam connector brackets locked into position via automated multi-axis CO2 gas shielded welders.
Surface Shot Blasting
Mechanical scale and rust removal followed by immersion pickling and phosphating for maximum primer adhesion.
Electrostatic Powder
60-80 micron epoxy-polyester powder applied automatically, baked at 200°C for exceptional chip and impact resistance.
Batch Quality Inspection
Cross-hatch adhesion testing, salt-spray chamber durability checks, and precision beam deflection tests.
Container Staging
Steel bundle banding, protective edge guards, and custom dunnage layouts engineered for effortless container offloading.
Future Pallet Storage Unit Sourcing & Tech Trends (2026–2030)
How supply chain executives, 3PL managers, and warehouse engineers are evolving pallet rack specifications to accommodate automation and sustainability mandates.
Autonomous Mobile Robot (AMR) & Shuttle Synergies
Traditional static storage is transitioning rapidly toward semi-automated radio shuttle and pallet-runner platforms. Warehouses require structural upright profiles with ultra-strict geometric straightness to allow automated shuttles to traverse 40-pallet deep lanes without sensor dislocation or friction jams.
Cold-Chain Cubic Volumetric Densification
With sub-zero freezer electricity rates surging globally, operators are replacing broad forklift aisles with High-Density Drive-In, Push-Back, and Pallet Flow Roller configurations. Condensing pallet storage into a 65% smaller refrigerated footprint reduces overall per-pallet energy consumption by up to 38%.
Parametric BIM & Cloud CAD Optimization
Procurement teams no longer wait weeks for layout drafts. Structural engineering models are now developed through 3D parametric Building Information Modeling (BIM), enabling instant interference detection with facility sprinkler heads, HVAC ducting, and dock levelers within 24 hours of RFQ submission.
Pallet Storage Unit Procurement FAQs
Clarifications on container freight packing, international seismic reviews, pallet standard alignments, and custom factory tolerances.
Q Are your pallet racks engineered for standard 48" x 40" GMA pallets?
Yes. Our beams and upright frame depths are engineered around both North American 48" x 40" GMA pallets and European 1200 x 800 mm Euro-pallets. Standard 96" and 108" clear bay beam lengths comfortably house two or three GMA pallets per level with required 3" to 4" flue clearances.
Q Can HEDA provide imperial load calculations (lbs/level) and CAD layouts?
Absolutely. Our in-house engineering team routinely outputs comprehensive drawing packages in both imperial (feet, inches, lbs) and metric systems. Each design document incorporates load capacity tables, upright section moduli, and beam deflection calculations ready for structural review.
Q How does HEDA support municipal permitting and seismic compliance?
We supply component specifications, steel chemistry certifications, anchor shear values, and moment calculations. These documents are directly utilized by your local licensed Professional Engineer (PE) or Engineer of Record (EOR) to obtain building department permits across North America and Europe.
Q What is the typical lead time and ocean container logistics plan?
Factory production spans 15 to 25 days depending on total project tonnage. We engineer custom container packing schemes (20GP, 40GP, 40HQ) using high-tensile strapping, corner guards, and pallet skid bases to ensure components arrive free of scratch defects and can be rapidly stripped by forklift.
Q What is the advantage of welded upright frames vs. bolted teardrop frames?
Bolted upright frames dramatically decrease ocean freight volume—enabling up to 35% more steel tonnage per 40HQ container, which slashes landed freight cost per pallet location. Furthermore, bolted configurations permit quick field replacement of damaged lower upright columns without discarding the entire mast.
Q Can you fabricate custom powder coating colors to match our corporate branding?
Yes. We offer electrostatic powder coating in any standard RAL color code (e.g., Safety Orange RAL 2004, Ultramarine Blue RAL 5002, Signal Yellow RAL 1003, or Anthracite Gray). Pre-treatment includes pickling and phosphating to guarantee superior salt spray and adhesion ratings.
Ready to Engineer Your High-Yield Pallet Storage Facility?
Submit your warehouse floor plan, clear ceiling height, pallet weight specs, and forklift models. Our senior logistics engineers will return an optimized CAD drawing, 3D visualization, and comprehensive factory-direct quotation within 24 hours.