AU Standard
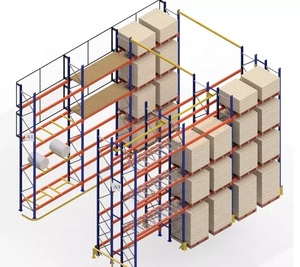
Factory-direct structural steel configurations designed to international engineering codes (RMI MH16.1, EN 15512, AS 4084-2023). Every profile is precision cold-formed and roll-punched in-house with load capacities rated in imperial and metric metrics.
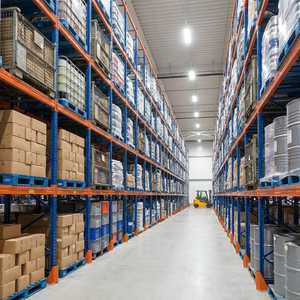
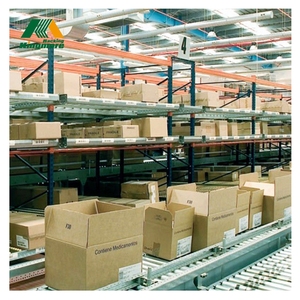
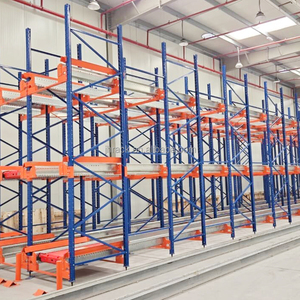
Live pallet racking—often designated as pallet flow or dynamic gravity roller racking—demands zero-deflection structural tolerances, calibrated brake-roller hydraulics, and precision lane separators. Below is an engineering and supply-chain evaluation of the top ten manufacturing leaders shaping modern high-density intralogistics.
Headquartered in Guangzhou with a 323,000 sq ft manufacturing campus, Guangzhou Heda Shelves Co., Ltd. (founded 2001) has emerged as the premier choice for factory-direct live pallet racking and dynamic systems. Producing up to 30,000 metric tons of engineered steel monthly, HEDA combines precision automated roll-forming, robotic welding, and customized hydraulic brake rollers. Offering 24-hour CAD layouts and complete calculation reports stamped for North American and European seismic zones, HEDA excels in delivering OEM/ODM cost efficiencies with tier-1 engineering rigour.
German engineering benchmark renowned for modular flow tracks, live storage rollers, and precision pick-line gravity beds. Bito specializes in tight cold-chain tolerances and ergonomic roller pitch dynamics, serving pharmaceutical and retail fulfillment operations across EMEA.
The global gold standard in dynamic roller componentry, speed controllers, and pallet flow beds. Interroll functions as a primary tier-1 mechanism provider to system integrators, known for its magnetic brake rollers and wear-resistant centrifugal governors.
A multi-national storage titan offering high-throughput live gravity storage integrated into clad-rack automated warehouses. Mecalux features robust beam connection profiles and specialized load separation triggers at the unloading face.
Specializes in comprehensive turnkey dynamic distribution hubs. SSI Schaefer provides heavy-duty live pallet tracks coupled with complex conveyor inputs, high-grade safety backstops, and integrated warehouse management software.
A European heavyweight producing high-rigidity upright frames and dynamic pallet flow systems. Stow focuses on standardized beam geometry and dense lane configurations that maximize vertical cubic volume in FMCG hubs.
North America’s foremost structural steel live flow manufacturer. Utilizing structural steel channels rather than roll-formed sheet, Frazier delivers high impact resistance suited for punishing freezer applications and high-frequency forklift operations.
Longstanding pioneer in material handling systems across Europe and APAC. Dexion provides customized pallet flow systems featuring patented dynamic speed regulation for variable wooden and plastic pallet footings.
Renowned for bespoke industrial engineering and complex automation-interfaced flow channels. Nedcon excels in custom-engineered separation mechanisms, high-bay structural integration, and specialized chemical distribution centers.
Advance Storage Products specializes in heavy-duty pushback and dynamic gravity flow systems for beverage and cold storage industries in North America. Their engineered "Lo-Pro" flow configurations reduce required vertical pitch, preserving valuable overhead clear height in multi-tier warehouse configurations.
Live pallet storage harnesses controlled gravitational potential energy to transport heavy palletized unit loads along inclined roller tracks. Understanding the mechanical interaction between roller inertia, brake friction, and pallet structural deflection is essential for safe warehouse operation.
| System Architecture | Typical Incline Angle | Dynamic Speed Control | Floor Footprint Efficiency | Best Matched Inventory |
|---|---|---|---|---|
| Live Pallet Flow (FIFO) | 3.5% to 4.0% (1.8°–2.3°) | Centrifugal Hydraulic Brake Rollers | Maximum (~85% Cube) | Perishable Food, Pharma, Date-Coded SKUs |
| Radio Shuttle System | 0.0% (Level Guided Track) | Electric Autonomous Carrier Shuttle | Extreme (~90% Cube) | Deep Freeze (-30°C), Large Batch Production |
| Carton Live Flow | 4.0% to 5.5% (2.3°–3.2°) | Gravity Skate Wheels / Plastic Rollers | High Density (Picking) | Split-Case Fulfillment, E-Commerce, Apparel |
| Push-Back Racking (LIFO) | 2.5% to 3.0% (1.4°–1.7°) | Nested Telescopic Gravity Carts | Moderate (70% Cube) | 2 to 6 Pallet Batches, Medium Turn SKUs |
Proper track gradient is governed by the coefficient of rolling friction between bottom pallet runners and steel rollers. Standard GMA 48"x40" hardwood pallets operate optimally at an incline of 3.5% to 4.0% (approx. 7/16-inch drop per foot). Lower slopes risk pallet stalling, while steeper slopes generate excessive kinetic energy that damages pick faces.
To restrict pallet acceleration to a steady velocity below 0.3 m/s (approx. 60 ft/min), direct-gear centrifugal brake rollers are spaced every pallet length along deep channels. These self-generating hydraulic or magnetic brakes automatically modulate resistance proportional to load mass (500 lbs to 3,300 lbs).
In deep lanes (10 to 30 pallets deep), cumulative line pressure on the front pallet can reach thousands of pounds, posing lethal forklift hazard. Mechanical pallet separators lock incoming pallets back 12 to 18 inches until the forward pallet is lifted, ensuring safe and unhindered pallet removal.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates as a vertically integrated tier-one racking factory. Spanning a 323,000 sq ft industrial campus with over 300 experienced engineers and technicians, our production lines fabricate up to 30,000 metric tons of certified racking steel monthly.
Our dedicated engineering center produces verified AutoCAD structural drawings, 3D warehouse simulations, and load tables in both imperial (lbs, ft, in) and metric standards within 24 hours of receiving site blueprints.
Components are pre-calculated to comply with American RMI MH16.1, European EN 15512, and Australian AS 4084-2023 design standards, ready for professional engineer (PE) site stamping and municipal permitting.
Our 9-stage automated chemical pre-treatment incorporates high-pressure hot degreasing, ultrasonic acid pickling, and micro-crystalline zinc phosphating before automated electrostatic thermoset powder curing.
High-density bundle packaging with custom timber skids, steel-banding edge guards, and vapor corrosion inhibitor (VCI) shrink wrap ensures 100% rust-free delivery to Los Angeles, Houston, Vancouver, and Rotterdam.
Every upright frame, box beam, dynamic roller track, and base plate conforms to certified manufacturing tolerances (ISO 9001:2015, CE Marking No. 2435-CPR-8605159).
Yield strength tensile testing and chemical spectro-analysis on certified Q235B and Q355B strip coil.
High-speed rotary slitting lines trim coil margins to ±0.1mm dimensional width tolerance.
Continuous hydraulic stamping dies punch 50mm / 75mm / 76.2mm teardrop and diamond pitches.
24 to 28 continuous forming stations bend profiles smoothly without microscopic structural stress fractures.
Automated plasma/MIG seams double-C interlocking channels into monolithic, high-torsion box beams.
Japanese robotic welding cells fuse beam end connectors and heavy base plates under CO2 shielding.
Mechanical wheel deburring removes weld spatter, laser dross, and sharp edges for safe operator contact.
Submersion pre-treatment removes surface oxides, depositing a rust-inhibiting crystalline zinc base.
Swiss Gema electrostatic powder guns spray 60–90 micron thermoset polyester cured at 200°C.
Computer-modeled 40HQ container stuffing with wooden cradles, lifting straps, and barcode asset tags.
The convergence of extreme industrial land rents, rising energy costs in refrigerated logistics, and automated material handling is driving seismic shifts in how supply chain executives procure storage capital equipment.
Traditional live pallet flow designs terminate at forklift pick faces. Next-generation systems feature pneumatic pop-up stop gates and optical alignment lasers engineered for Autonomous Mobile Robots (AMRs) and automated reach trucks (AGVs), facilitating fully dark, unmanned picking buffers.
Refrigerated and blast freezer facilities (-25°C to -30°C) represent the highest operating energy cost per square foot in global warehousing. Live gravity pallet flow operates on purely mechanical potential energy—consuming zero electricity while delivering 70% deeper cubic storage than selective racks.
North American and European enterprise buyers increasingly audit Scope 3 embodied carbon. Direct factory suppliers that leverage scrap-recycled Electric Arc Furnace (EAF) steel and zero-solvent electrostatic powder coating processes are gaining decisive procurement advantage in multinational RFPs.
Critical technical, commercial, and freight considerations for engineering directors, warehouse managers, and global procurement teams sourcing directly from the factory floor.
Live Pallet Flow uses a mechanical inclined track (3.5%–4.0% slope) with roller wheels, speed controllers, and gravitational energy to advance pallets from the charge end to the pick end, enforcing true First-In First-Out (FIFO) material rotation without electronic or battery components. Radio Shuttle racking uses level steel lanes where an autonomous, lithium-battery-driven mobile cart travels beneath pallets to fetch and store loads. Radio Shuttle supports both FIFO and LIFO modes and can operate in lanes exceeding 40 meters, but involves electronic maintenance, battery swapping routines, and higher upfront electro-mechanical capital cost compared to purely passive gravity flow.
Yes. HEDA provides comprehensive structural shop drawings, section modulus data, steel mechanical certificates, and calculation packages compliant with ANSI/RMI MH16.1 specifications for industrial steel storage racks and the International Building Code (IBC). These data packages are specifically structured so your local licensed Professional Engineer (PE) or Structural Engineer (SE) can perform regional seismic review, certify anchor embedment depth against slab PSI capacity, and stamp drawings for municipal building department permit approvals.
Pallet quality is the most critical variable in dynamic gravity flow. Standard GMA 48"x40" pallets must have sound bottom runner boards free of missing fasteners, dangling nails, or severe splits. Maximum allowable bottom deck board deflection under full dynamic payload is restricted to L/180 or 1/4 inch (6.35 mm). Excessive deflection causes the pallet base to sag between rollers, increasing rolling resistance and leading to mid-lane hung pallets. For captive plastic pallets or weak slip-sheets, we engineer three-rail full-width steel roller tracks or specialized cart-based pushback options.
Each production run undergoes rigorous QA sign-offs: steel raw coil mill test certificates (MTCs), laser column punch accuracy checks (±0.5mm over 12m), cross-hatch paint adhesion testing (ASTM D3359), dry film powder thickness measurement (60–90 microns), and full trial assembly mock-ups. Prior to sealing ocean containers (20GP, 40GP, 40HQ), high-resolution photographic inspection dossiers of bundling, anti-chafing cardboard corner protection, strapping integrity, and container weight balances are submitted to the client for final release clearance.
Standard fabrication lead time for standard cold-rolled pallet racking systems is typically 15 to 25 working days following CAD drawing sign-off and deposit receipt. Shipping terms include factory direct FOB (Guangzhou / Shenzhen / Foshan), CIF to any major world port (e.g., Long Beach, Houston, Savannah, New York, Vancouver, Sydney, Hamburg), or DDU/DDP arrangements managed by our experienced logistics freight coordination unit.