Engineering Authority & Supply Chain Guide

Top 10 Heavy Pallet Racking Manufacturers & Suppliers

A comprehensive global benchmarking report, structural engineering framework, and procurement white paper for warehouse architects, 3PL directors, and supply chain executives.

Enterprise Heavy Racking Systems

High-Performance Storage Equipment & Solutions

Direct factory-engineered structural systems fabricated under strict ISO 9001:2015 controls, rated for North American and European industrial duty loads.
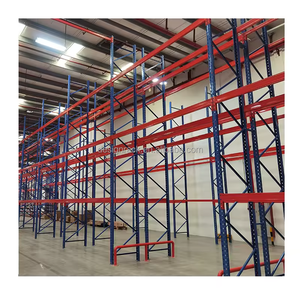
Heavy Selective Heavy Duty Shelving Storage Easy Assemble Material Racking Unit Industrial Pallet Rack Solution

Heavy Duty Industrial Pallet Rack Solution Racking System
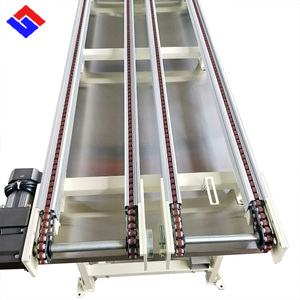
Q235B High Tensile Up to 4,500 kg/Tier Easy Teardrop/Keyhole
Conveyor Pallet Flow Aluminum Rail Motorized Duplex Chain Pallet Flow Industrial Assembly Double Speed Chain Conveyor
High Density Drive in Pallet Racking Warehouse Rack Dividers Stacking Shelves for Warehouse Storage

Drive In Pallet Racking Heavy Warehouse Dividers
80% Footprint Sav. LIFO Dynamic Reinforced Arms
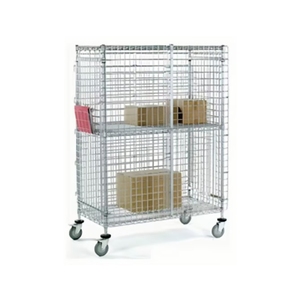
ESD Industrial 4-Tier Chrome Wire Shelving Unit Adjustable Industrial Storage Rack ESD-Safe

4-Tier Adjustable Chrome Wire Shelving ESD-Safe Rack
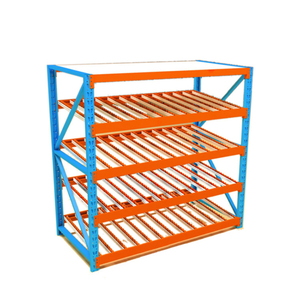
Heavy Chrome Plate Anti-Static Ready Cleanroom / Dry DC
Gravity Flow Blue Orange Steel 5 Layer Sliding FIFO Flow-Through Racking System

5-Layer Steel FIFO Dynamic Flow-Through Racking
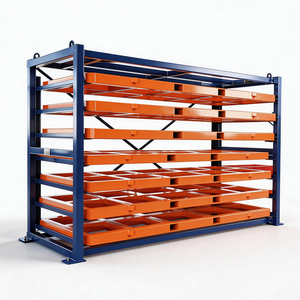
Strict FIFO Rotation Centrifugal Brakes Fast Picking Line
CE Certified CE Certified Industrial Warehouse Steel Shelving System Heavy Duty Storage Racks

CE Certified Heavy Duty Metal Cargo Shelving Systems
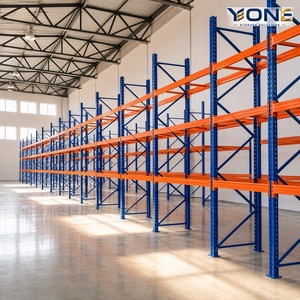
EN 15512 Approved Cold-Roll Profiles Durable Epoxy Coat
Q235B Standard Steel Storage Rack Heavy Duty Pallet Racking Q235B Steel Selective Racking

Selective Q235B Steel Pallet Rack Industrial System
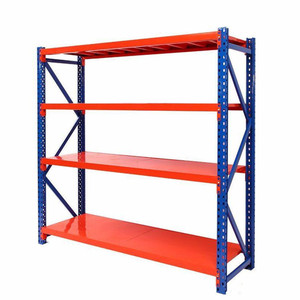
100% SKU Access GMA 48x40 Match Dual C-Box Beams
Tailored Engineering Custom Heavy-Duty Metal Rack Storage Shelf High Quality Iron Warehouse Racking

Custom Engineered Heavy-Duty Cargo Iron Racking

Non-Standard Spans Bespoke Finishes Heavy Duty Baseplate
Executive Benchmark & Market Dynamics

Global Industrial Pallet Racking Landscape

Analyzing structural engineering standards, manufacturing scalability, and supply chain efficiency across top global manufacturers.

Modern warehouse infrastructure has evolved beyond simple structural steel assemblies into engineered, high-precision storage systems capable of supporting multi-tiered automation, intense seismic shear loads, and ultra-dense SKU management. As global supply chain pressures demand maximized cubic-foot volume utilization rather than mere square-foot footprint, the selection of heavy pallet racking manufacturers requires rigorous engineering qualification. Industrial purchasers must balance yield strength tolerances, cold-roll metallurgical consistency, electrostatic finish longevity, and seismic compliance certifications against total capital expenditure.

Under international codes such as the Rack Manufacturers Institute (RMI) MH16.1 in North America and EN 15512 / EN 15620 across the European Union, upright columns, boxed step beams, and structural row spacers undergo sophisticated finite element analysis (FEA) to ensure structural safety factors typically exceeding 1.65 to 1.95 against buckling. Choosing the right industrial partner directly determines warehouse operational safety, throughput velocity, inventory preservation, and lifelong return on invested capital (ROIC).

System Architecture Pallet Accessibility Space Utilization Structural Load (kg/level) Rotation Principle Ideal Industry Use-Case
Selective Pallet Racking 100% Direct 40% – 50% 1,000 – 4,500 kg FIFO / LIFO Flexible General 3PL, FMCG, Diverse Retail Warehousing
Drive-In / Drive-Through Lane Entry Only 70% – 80% 1,200 – 2,000 kg LIFO (Drive-In) / FIFO Cold Storage, Seasonal Harvest, Beverage Bottling
Pallet Flow (Gravity Roller) Single Face Dedicated 80% – 85% 800 – 1,800 kg Strict FIFO Perishable Goods, Pharmaceuticals, Chemical Batches
Push-Back (Cart/Sled) Aisle Face Accessible 65% – 75% 1,000 – 1,500 kg LIFO Only Medium SKU Velocity, High-Bay Cold Warehousing
Radio Shuttle Racking Automated Deep-Lane 85% – 90% 1,000 – 2,500 kg Automated FIFO / LIFO Food Distribution, Deep Freezer, Automated Hubs
Heavy Cantilever Systems Unobstructed Front 50% – 65% 1,500 – 6,000 kg Flexible Access Structural Steel, Timber, PVC Piping, Sheet Plate
Comparative Vendor Profiles

Top 10 Heavy Pallet Racking Manufacturers & Suppliers

In-depth technical analysis of the world's most reputable racking manufacturers based on engineering capability, global delivery scope, steel grades, and project performance.

1. Guangzhou HEDA Shelves Co., Ltd.

Factory Direct Leader
Founded in 2001, HEDA Shelves is an internationally recognized powerhouse in high-density pallet racking, industrial shelving, and heavy mezzanine platforms. Operating a massive 30,000 m² (approx. 323,000 sq ft) manufacturing campus equipped with automated slitting, cold roll-forming lines, robotic welding stations, and multi-stage powder coating chambers, HEDA produces up to 30,000 metric tons of steel storage equipment per month. HEDA delivers customized structural racking designed directly around North American (48"x40" GMA) and European pallet formats, complete with certified 2D CAD engineering schematics, 3D structural simulations, and imperial/metric load tables in 24 hours.
ISO 9001:2015 CE Construction Cert 30,000 m² Plant 10,000+ Completed Projects

2. SSI Schaefer Group

Global Automation Pioneer
Headquartered in Neunkirchen, Germany, SSI Schaefer is one of the world's largest logistics solutions providers. Renowned for end-to-end intralogistics ecosystems, their heavy pallet racking offerings integrate seamlessly with automated storage and retrieval systems (ASRS), shuttle systems, and conveying mechanics. Their high-bay racking systems can exceed 40 meters in clear height, forming the structural clad-rack framework for major automotive and retail multinational distribution hubs worldwide.
Clad-Rack Systems ASRS Integration EN 15512 Specialist European Footprint

3. Mecalux, S.A.

Transatlantic Heavyweight
With headquarters in Barcelona, Spain and an expansive North American presence as Interlake Mecalux, this manufacturer commands substantial market share across the Americas and Europe. Mecalux specializes in versatile selective racking, cantilever designs, and radio shuttle solutions. Their proprietary Easy WMS software seamlessly orchestrates multi-deep pallet channels, making them a standard for pharmaceutical and FMCG facilities requiring robust inventory management integrations.
Interlake Teardrop WMS Integration Dual Continent Mills RMI MH16.1 Tested

4. Frazier Industrial Company

Structural Steel Icon
Based in Long Valley, New Jersey, Frazier Industrial is distinguished as North America's premier manufacturer of 100% hot-rolled structural steel racking systems. In contrast to standard roll-formed sheet steel, Frazier builds uprights and shelf channels using heavy structural C-channels, making them virtually impervious to catastrophic forklift impact abuse in rigorous cold storage, beverage warehouse, and rough 3PL environments.
Hot-Rolled Structural Impact Abuse Proof Severe Cold Duty North American Base

5. Daifuku Co., Ltd.

Intralogistics Leader
Headquartered in Osaka, Japan, Daifuku consistently ranks at the pinnacle of global material handling system integrators. Daifuku's racking solutions are primarily engineered for complex high-throughput automation, semiconductor cleanroom storage, and stacker-crane interfaces. Their heavy-duty racking columns maintain exceptional dimensional precision to ensure sub-millimeter tolerances required by laser-guided optical sorting cranes.
Automated Stacker Interface Cleanroom Certified Precision Machined Asia-Pacific Leader

6. Stow Group

European Engineering Power
Headquartered in Belgium, Stow Group is one of the fastest-growing European rack manufacturing enterprises with an extensive global distribution network. Known for its innovative pallet shuttle automation systems (Movia) and heavy-duty Atlas storage series, Stow produces precision cold-formed upright profiles with high steel yield resistance. Their modular platforms serve diverse distribution centers across pan-European and export markets.
Movia Shuttle Atlas Racking Line Multi-Factory Scale High Yield Formings

7. Jungheinrich AG

Integrated Vehicle & Rack
Operating from Hamburg, Germany, Jungheinrich holds a unique market advantage as both a premium material handling equipment manufacturer (narrow-aisle reach trucks and AGVs) and a manufacturer of heavy industrial racking systems. This allows Jungheinrich engineers to optimize narrow aisle (VNA) clearances down to bare operational margins, minimizing aisle widths while preventing truck mast oscillation collisions with racking beams.
VNA Specialists AGV Synergy German Engineering Turnkey Operations

8. Dexion (Gonvarri Material Handling)

Historic Storage Architect
A founding pioneer of modern slotted-angle and teardrop racking principles dating back to 1937, Dexion operates as a cornerstone of the Gonvarri Material Handling group. Dexion provides comprehensive warehousing architectures, including heavy pallet racking, dynamic carton live flow, and custom cantilever structures. Their systems are widely deployed throughout the UK, Scandinavia, Australasia, and continental Europe.
Slotted Angle Heritage Gonvarri Group Backing High Seismic Designs Industrial Sturdiness

9. Steel King Industries, Inc.

US Structural Specialist
Based in Stevens Point, Wisconsin, Steel King is an established US supplier respected for producing both heavy-gauge roll-formed and structural channel pallet racks (such as the SK2000 and SK3000 series). Steel King emphasizes welded tubular columns, closed-tube upright designs that provide 250 times greater torsional resistance than conventional open-back column profiles, crucial for heavy manufacturing tool-and-die racking.
Closed Tubular Columns SK2000 / SK3000 Extreme Torsion Shield Made in USA

10. Constructor Group / Constructor Dexion

Nordic & Central EU Leader
With deep market penetration across northern Europe, Constructor Group provides specialized heavy-duty pallet racking engineered for cold temperature stability and high-dynamic automated shuttle systems. Their focus on custom zinc-plated corrosion protection ensures optimal structural resilience in damp cold rooms, fishing industry freezers, and maritime transit terminals.
Galvanized Options Cold Chain Resistance Nordic Quality Modular Pallet Bays
Production Integrity & Quality Control

Enterprise Advantages: Guangzhou HEDA Shelves

Combining 25+ years of metallurgical roll-forming expertise with factory-direct pricing, certified QA/QC protocols, and rapid global logistics.
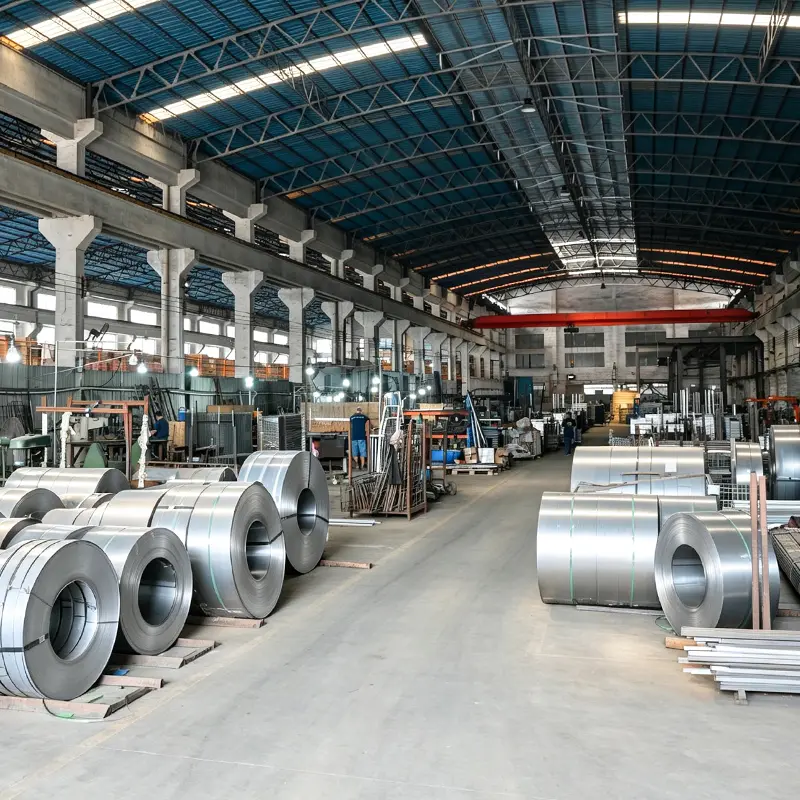
2001yr
Established Heritage
30,000m²
Manufacturing Plant
30,000t/m
Monthly Steel Output
10,000+
Global Projects Completed
25+ Years Industrial Racking Production Expertise

25+ Years of Proven Expertise

Every beam connector claw, foot baseplate anchor hole, and column bracing pitch is informed by empirical performance across 10,000+ warehouse installations globally.
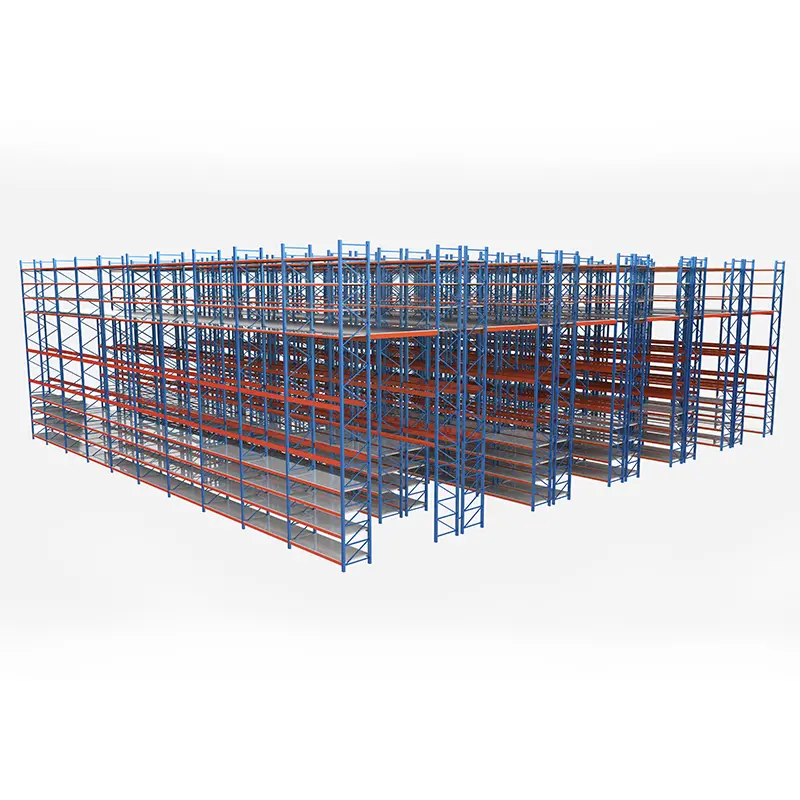
Free CAD and 3D Structural Engineering Drawings

Free CAD & 3D Engineering within 24h

Our senior structural logistics team converts warehouse CAD files into detailed plan views, 3D clearance animations, and imperial/metric load capacity tables in 24 hours.
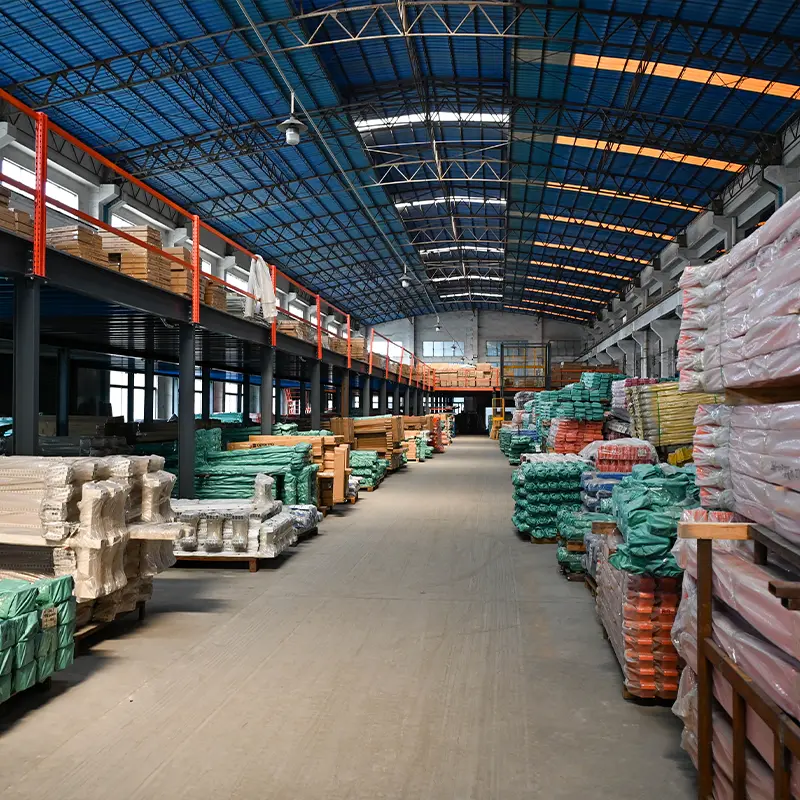
Automated Pickling, Phosphating and Powder Coating Lines

Safe, Certified Structural Steel

Certified Q235B / Q355B coil steel undergoes automated CNC shearing, continuous roll forming, multi-step acid pickling, phosphating, and heavy electrostatic epoxy coating.
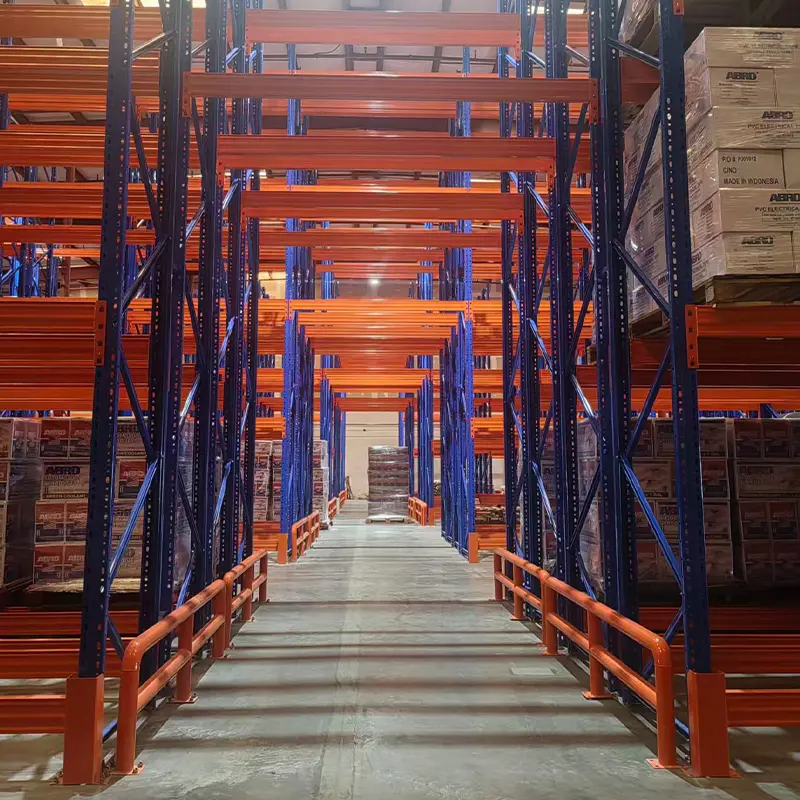
Fully Customized Enterprise Warehouse Storage Solutions

Full OEM/ODM Sourcing Support

Custom beam lengths matching standard 48x40 GMA or non-standard heavy pallets, specialized seismic anchor plates, customized powder coat RAL colors, and branded private labeling.

Procurement Strategy 2025–2030

Future Purchasing Trends in Heavy Pallet Racking

How supply chain executives, industrial developers, and institutional buyers are shifting procurement models to optimize lifecycle costs and sustainability.

Total Cost of Ownership (TCO) vs Capital Outlay

Buyers are moving away from evaluating initial invoice price per beam level. Modern procurement frameworks account for structural damage resistance, ease of beam replacement, powder coat longevity in corrosive humidity, and factory direct containerization efficiency that reduces inland transit damage.

Standardized Modularity & Hybrid Storage

With volatile e-commerce SKU churn, fixed-dimension racking is being superseded by hybrid reconfigurable bays. Uprights engineered with unified punch configurations allow effortless retrofitting from standard selective beams to carton-flow conveyors or radio shuttle tracks without dismantling primary vertical frames.

Direct-from-Source Precision Logistics

By eliminating multiple tiers of regional brokers and distributors, large 3PLs are directly partnering with major primary manufacturers like HEDA Shelves. Direct container-optimized loading directly from ISO certified mills cuts procurement markups by 25% to 40% while preserving direct engineering accountability.

Technological Innovations

Emerging Engineering Trends in Storage Architecture

The convergence of material science, seismic modeling, robotic intralogistics, and digital asset tracking across modern industrial warehouses.

ASRS-Ready Tight Tolerance Engineering

As automated guided vehicles (AGVs) and autonomous mobile robots (AMRs) replace manual counterbalanced forklifts, permissible deflection limits are tightening from traditional L/200 down to L/350. Cold roll-formed profiles must maintain near-zero twist and deviation to avoid laser sensor tripping.

Advanced Seismic Dissipation Baseplates

Global building codes (such as California IBC Seismic Design Category E/F and Eurocode 8) mandate ductile baseplate anchoring systems that dissipate lateral ground acceleration without cracking concrete slabs, ensuring high-bay rack survival during major geological seismic events.

Cold-Room Anti-Embrittlement Alloys

Sub-zero cold storage warehouses (-25°C to -30°C) induce severe cold brittleness in lower-grade steels. Next-generation racking relies on normalized low-carbon steels micro-alloyed with vanadium or niobium, preventing catastrophic brittle failure under shock loading at freezing temperatures.

Purchaser Knowledge Base

Heavy Pallet Racking Procurement FAQ

Direct answers to critical technical, compliance, logistical, and structural questions encountered by enterprise procurement directors.

What are the key structural steel standards required for North American and European racking installations?
In North America, racking must comply with the Rack Manufacturers Institute (RMI) Specification ANSI MH16.1, which sets strict parameters for allowable stress, column buckling, beam deflection under maximum load (typically span divided by 180 or 200), and floor anchor bolt pullout safety. In Europe, the definitive standard is EN 15512:2020 for structural design, alongside EN 15620 for tolerances, deformations, and clearances. Guangzhou HEDA Shelves utilizes certified Q235B and Q355B hot-rolled and cold-formed coil steels that meet or exceed ASTM A36 and EN 10025 structural yield points, backed by third-party CE and ISO 9001:2015 certifications.
How do you calculate the required clear aisle width between pallet racking rows?
Clear aisle width is fundamentally dictated by the forklift truck's right-angle stacking turning radius plus pallet overhang and safety clearance. As a general rule:
  • Standard Counterbalance Forklifts: require 12 to 14 feet (3.65m to 4.2m) aisle clearance.
  • Reach Trucks: operate comfortably within 8.5 to 10 feet (2.6m to 3.0m).
  • Very Narrow Aisle (VNA) Turret Trucks: require only 5.5 to 6.5 feet (1.65m to 2.0m), often guided by inductive in-floor wire or optical laser tracks.
HEDA's layout engineering team incorporates exact forklift chassis data into every 2D/3D CAD layout before manufacturing starts.
Can factory-direct racking from HEDA Shelves be stamped by a local Professional Engineer (PE)?
Yes. For clients requiring municipal building permits, seismic approvals, or third-party engineering verification, HEDA Shelves provides complete structural calculation packets, weld certifications, cross-sectional moment of inertia specifications, and material mill test certificates (MTC). These engineering dossiers are prepared in imperial (lbs/inches) or metric units to ensure rapid, frictionless review and wet-stamping by your local Engineer of Record (EOR) or licensed structural PE.
What surface treatment is best for heavy pallet racks exposed to chemical or cold storage conditions?
For standard ambient distribution centers, an automated electrostatic epoxy-polyester powder coat (baked at 180°C–200°C after thorough acid pickling and phosphating) provides superior scratch, impact, and corrosion resistance. For damp cold storage, agricultural fertilizer storage, outdoor lumber yards, or caustic chemical facilities, hot-dip galvanizing (HDG) conforming to ASTM A123 or pre-galvanized high-yield steel sheet is highly recommended to eliminate the risk of flaking rust or paint degradation.
What information must a buyer prepare to receive an accurate CAD layout and price quote?
To provide an itemized Bill of Materials (BOM) and optimized layout within 24 hours, our engineering department requires:
  1. Warehouse Architectural Drawing: Showing clear ceiling height, column grid positions, dock doors, and building egress paths.
  2. Pallet Dimensions & Maximum Load: Width, depth, load height including pallet base, and maximum gross weight per pallet.
  3. Material Handling Equipment: Make and model of forklift or lift height capability.
  4. Turnover Strategy: High-density FIFO vs 100% selective access requirements.

Transform Your Warehouse Storage Density & Throughput

Connect directly with HEDA Shelves' senior racking engineers. Receive a factory-direct quotation, customized 2D/3D CAD design layout, and structural load analysis within 24 hours.

Inquire Now