Precision Heavy-Duty Racking & Gravity Dynamic Modules
Explore engineered warehouse storage configurations designed for high-density inventory consolidation, seamless pallet velocity, and severe cyclic warehouse loading conditions.
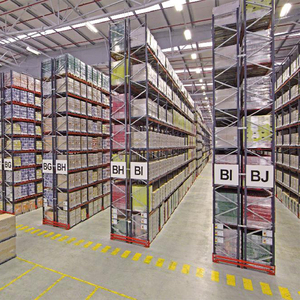
Guangzhou Adjustable Pallet Racking System
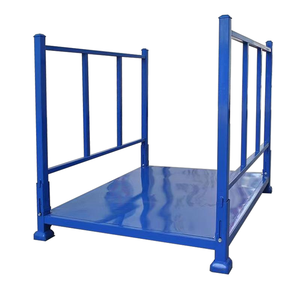
Customizable Heavy-Duty Portable Steel Stacking Racks
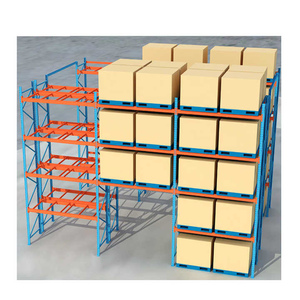
5-Layer Metal Drive-In High-Density Racking System
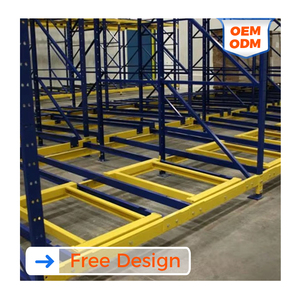
DJ Gravity Steel Push Back Rack for Warehouses
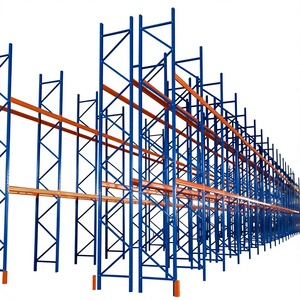
Hongxin Heavy-Duty Multi-Level Steel Racking
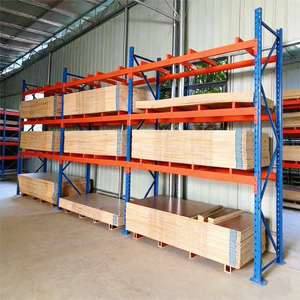
Industrial 5-Layer Steel Heavy Storage Racking
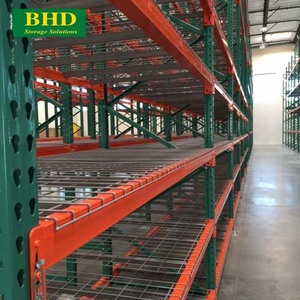
Top Selling Heavy-Duty Teardrop Steel Pallet Racking
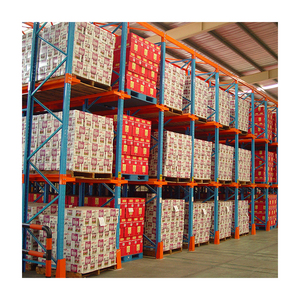
Drive-In Multi-Tier Through Racking System
Engineering Dynamics of Pallet Flow & Gravity Roller Beds
Gravity flow racking (often designated Pallet Flow or Dynamic Storage) is an unpowered kinetic storage system operating under controlled gravitational acceleration. By angling roller beds between 2.5% and 4.0% grade, palletized goods naturally travel from the load side (rear) to the discharge retrieval face (front).
Centrifugal Speed Controllers
Uncontrolled gravity poses catastrophic collision risks to structural beams and pallets. Heavy-duty magnetic or planetary gear centrifugal brake rollers are spaced every 1 to 2 pallet lengths along the lane. They passively absorb kinetic energy, maintaining a terminal velocity between 0.2 m/s and 0.35 m/s, irrespective of pallet weight swings between 300 kg and 1,500 kg.
Pallet Separation Devices
When extracting the front pallet, trailing pallets exert severe line pressure: $F_{\text{push}} = n \cdot W \cdot \sin(\theta)$. In a 15-pallet lane, thousands of pounds of line force wedge against the lead unit. Mechanical pallet separators lock trailing inventory back until the forklift safely raises the lead load, removing extraction back-pressure and protecting mast components.
Roller Track Metallurgical Profiles
Industrial gravity beds use split three-track or full-width heavy steel rollers with cold-drawn seamless carbon steel jackets ($t \ge 2.0\text{mm}$) mounted on sealed 6204/6205 precision bearings. For plastic runner pallets, zinc-galvanized ribbed rollers avoid point indentation, ensuring smooth motion down to -30°C in blast freezer facilities.
Top 10 Global Gravity Flow Rack Suppliers & Exporters Directory
Evaluated against cold-formed steel manufacturing scale, proprietary kinetic speed-governor engineering, seismic engineering validation (RMI / EN 15512), and export compliance track record.
Guangzhou HEDA Shelves Co., Ltd.
China (Global Sourcing Hub)Founded in 2001, HEDA Shelves operates a state-of-the-art 30,000 m² (323,000 sq ft) production campus yielding 30,000 metric tons of engineered steel monthly. Renowned for direct-factory North American and European logistics exports, HEDA engineers custom gravity roller channels, heavy-duty push-back nested cart systems, and turnkey dynamic pallet flow racks supported by imperial/metric PE stamp calculations within 24 hours.
- ISO 9001:2015 & CE Certified
- 30,000 Tons/Month Cold Rolling
- True FIFO Braking Calibrations
- 10,000+ Global Project Portfolio
Interroll Group
SwitzerlandRegarded as the global gold standard for internal dynamic gravity components, Interroll specializes in high-durability flow modules, the MSC 50 magnetic speed controller, and dynamic time-delay roller separators. While their structural uprights are frequently co-engineered with tier-1 fabricators, their proprietary roller tracks define industry reliability.
- Magnetic Speed Governor Tech
- Ultra-Low Maintenance Roller Beds
- Global Component Distribution
- Strict DIN / EN Safety Protocols
BITO-Lagertechnik Bittmann GmbH
GermanyBITO manufactures sophisticated carton flow (pieces/totes) and heavy pallet flow systems with patented ergonomic pick-tray adapters. Their engineering focus centers on zero-defect order preparation for European automotive lines and pharmaceutical clean-room cold chains, backed by precision tooling and automated cold-roll forming.
- Carton & Pallet Flow Synergy
- Boltless Quick-Adjust Lanes
- Automated Pick-Face Tilted Trays
- DIN EN ISO 14001 Compliant
NEDCON B.V. (Avoestalpine)
NetherlandsA voestalpine group company, NEDCON excels in large-scale automated flow rack installations integrated with crane-served clad-rack buildings. Their structural calculation models solve micro-deflection issues under 25-meter ceiling heights, ensuring roller bed pitch remains precise across dynamic seasonal thermal cycles.
- High-Bay Clad Rack Integration
- High-Yield Specialized Steels
- High Seismic Tolerance Design
- Full AS/RS Dynamic Interfacing
Mecalux S.A.
Spain / United StatesMecalux maintains extensive fabrication facilities across Europe and North America. Their pallet flow line offers split-roller designs for GMA pallets, intermediate braking units, and double-entry discharge bays that integrate directly into their proprietary Easy WMS software for automated replenishment scheduling.
- Global Logistics Presence
- Easy WMS Software Interoperability
- Dual North American Footprint
- Heavy Section Uprights
Advance Storage Products
United StatesAdvance Storage Products dominates North American structural pushback and dynamic gravity systems. Renowned for their Lo-Pro pushback and deep-lane flow beds, they fabricate systems utilizing rugged structural C-channel steel capable of withstanding rough forklift impacts in harsh food distribution centers.
- Heavy Structural C-Channel Steel
- Lo-Pro Low-Profile Flow Modules
- Severe Impact Resistance
- ANSI/RMI MH16.1 Compliant
Stow Group
BelgiumStow Group provides high-efficiency live pallet storage solutions engineered for continuous FIFO product cycles. With extensive cold-forming capabilities and continuous automated powder-coating lines, Stow designs dynamic gravity channels matched with their proprietary Atlas shuttle carriers for hybrid warehouse automation.
- Hybrid Shuttle / Gravity Systems
- Automated European Manufacturing
- Deep Lane Storage Efficiency
- Fully Scalable Frame Sections
Frazier Industrial Company
United StatesFamous for 100% hot-rolled structural steel construction, Frazier’s gravity flow racking offers unyielding load-bearing resilience in deep-freeze environments (-20°F). Their all-structural upright channels eliminate punch holes on critical impact surfaces, reducing frame failure risks from heavy reach trucks.
- 100% Structural Steel Channel
- Extreme Impact Deflection Strength
- Harsh Cold-Chain Longevity
- Certified Seismic PE Calculations
Jungheinrich AG
GermanyJungheinrich combines intralogistics material handling vehicles with modular flow racks. Their gravity live-storage lines are engineered around mast dynamics, featuring custom entry guides that align AGVs (Automated Guided Vehicles) and manual forklifts seamlessly into lane centerlines.
- Turnkey AGV-to-Rack Integration
- Optical Loading Visual Guides
- Precision European Mechanics
- End-to-End System Warranties
SSI Schaefer Systems
Germany / GlobalGlobal material handling giant SSI Schaefer provides engineered live storage racking with advanced ergonomic carton flow picking systems. Their high-throughput roller beds feature modular bolt-in cassettes, high-impact polycarbonate wheels, and automated pick-to-light bracket channels.
- Modular Quick-Swap Cassettes
- Integrated Pick-to-Light Raceways
- Comprehensive Global Delivery
- Robust Galvanized Shelf Tracks
Gravity Flow Rack Structural & Operational Comparison
Comprehensive engineering data to guide corporate capital expenditure (CapEx), safety audits, and mechanical load verification.
| Supplier | Primary Steel Spec | Brake Roller Technology | Pallet Separator Type | Max Lane Depth | Seismic / Standards Cert. |
|---|---|---|---|---|---|
| Guangzhou HEDA Shelves | Q235B / Q355 Cold-Formed, RMI Standard Spec | Adjustable Magnetic & Centrifugal Mechanical | Pneumatic & Foot-Treadle Mechanical Release | Up to 25 Pallets | ISO 9001:2015, CE Marking, PE Calculations |
| Interroll Group | High-Tensile Cold-Rolled Galvanized Sections | MSC 50 Non-Contact Eddy Current Governor | Time-Delay Mechanical Release Lever | Up to 30 Pallets | TÜV Rheinland, DIN EN 15512, CE |
| Advance Storage | ASTM A36 Hot-Rolled Structural C-Channel | Direct Contact Friction Brake Rollers | Heavy Mechanical Drop-Latch Catch | Up to 20 Pallets | RMI MH16.1, AISC Seismic Compliant |
| BITO-Lagertechnik | High-Yield Cold-Formed Dual-Phased Sheet | Internal Planetary Gearbox Brake | Step-Release Positive Locking Catch | Up to 22 Pallets | RAL-RG 614, DIN EN 15620, ISO 9001 |
| Mecalux | High-Elastic Micro-Alloy Structural Steel | Centrifugal Counter-Balanced Rollers | Automated Disconnect Treadle Arm | Up to 20 Pallets | EN 15512, RMI, ISO 14001, ASTM |
| Frazier Industrial | 50,000 PSI Hot-Rolled Structural Channels | Heavy Enclosed Viscous Drag Rollers | Structural Weight-Actuated Latch Arms | Up to 18 Pallets | RMI 2012, AISC 360, AWS Certified |
Strategic Sourcing & Technological Trends in Dynamic Storage
The gravity flow rack sector is experiencing substantial technological advancement, driven by e-commerce fulfillment speed, cold chain expansion, and autonomous material handling.
1. Autonomous AMR Discharge Interfaces
Traditional gravity discharge faces depend on human forklift operators to gently clear the separation plate. Modern automated warehouses pair gravity flow discharge bays with Autonomous Mobile Robots (AMRs) and Automated Guided Forklifts (AGFs). This requires ±1.5mm tolerance on end-stop positioning and optical retro-reflective sensors mounted along the roller channel to report real-time bay fullness back to warehouse execution systems (WES).
2. Contactless Magnetic Braking Rollers
Conventional friction brakes suffer from internal pad degradation, requiring messy hydraulic maintenance and continuous line shutdowns. The transition toward magnetic eddy-current brake rollers creates frictionless kinetic deceleration proportional to pallet speed. These wear-free components operate continuously for over 10 years without maintenance, eliminating grease leaks in food-grade or pharmaceutical distribution centers.
3. Cryogenic Polymers for Cold Chains
With temperature-controlled pharmaceutical shipments and rapid frozen food distribution expanding globally, gravity flow components must endure extreme environments down to -30°C (-22°F). Procurement teams are rejecting brittle PVC wheels in favor of ultra-high-molecular-weight (UHMW) polyethylene wheels with low-temperature synthetic lubrication to prevent roller lock-up and pallet hang-ups.
Why Enterprise Importers Partner with Guangzhou HEDA Shelves
Direct manufacturer capabilities that bridge complex engineering layouts with container-optimized worldwide shipping.
For overseas procurement directors, third-party logistics operators (3PLs), and material handling distributors across North America, Europe, and Australasia, Guangzhou HEDA Shelves Co., Ltd. resolves the primary friction points of dynamic rack sourcing: engineering precision, lead-time control, and structural verification. Rather than acting as a standard trading firm, HEDA operates an integrated heavy roll-forming facility equipped with automated stamping lines, high-frequency continuous profile mills, automated robotic welding cells, and multi-stage pickling, phosphating, and electrostatic powder coating lines.
HEDA engineers understand that structural rack frames destined for the United States, Canada, or Mexico must conform strictly to ANSI/RMI MH16.1 specifications, seismic site classifications, and local building code load tables. For European deployments, frames and beams are calculated in full alignment with EN 15512 and EN 15620. Whether specifying standard 48" × 40" GMA grocery pallets, 1200 × 1000 mm European pallets, or heavy steel automotive skids, HEDA formulates custom gravity drop slopes, brake roller intervals, and entry funnel guides designed for seamless throughput.
All export packages are custom palletized, bundle-strapped, and moisture-protected inside 20GP or 40HQ ocean shipping containers with color-coded assembly tags and installation manuals. Clients receive complete CAD shop drawings, 3D structural renderings, and engineering load calculations within 24 hours of inquiry.
Frequently Asked Questions on Gravity Flow Rack Engineering
Detailed answers addressing structural calculations, pitch engineering, cold storage performance, and international logistics.