Stackable & Modular
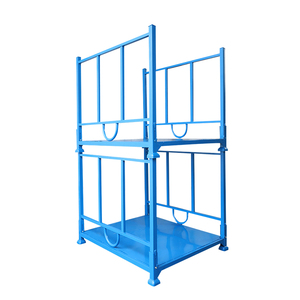
Warehouse Storage Metal Stackable Rack Heavy Duty Pallet Stacking Frames
- Foldable post nesting design
- Load rating: Up to 1,500 kg / pallet
- Dynamic staging buffer integration
Direct factory production engineered for rigorous pallet dynamic forces, cold room performance, high-density live storage, and multi-tier picking fulfillment hubs.
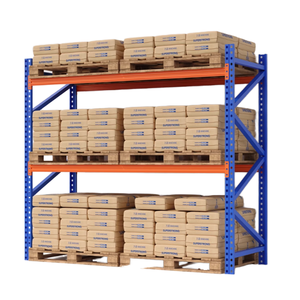
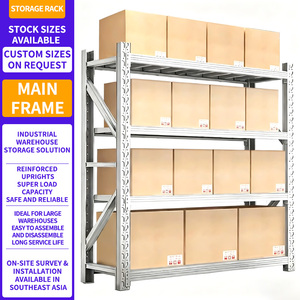
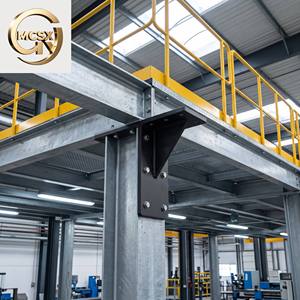
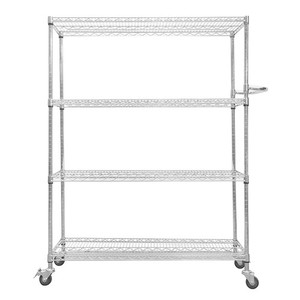
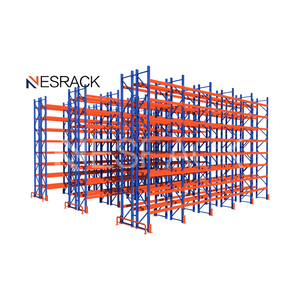
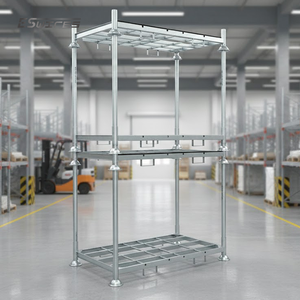
Modern distribution complexes, high-velocity omnichannel order-fulfillment centers, and temperature-controlled food cold chains demand exact tolerances from gravity-fed roller systems. As an integrated OEM/ODM manufacturer, HEDA Shelves addresses the core structural variables that prevent pallet hung-ups, rack runaway, and line-side fatigue failure.
Unlike static selective pallet racks that carry purely deadweight compressive loads, roller racks (such as carton flow beds, live pallet gravity flow channels, and push-back cart systems) must absorb continuous dynamic momentum, load deceleration shockwaves, and torsional deflection across extended spans.
Our engineering calculates incline gradients between 2.5% and 3.5% (approx. 7/16" per foot) calibrated precisely against bottom-deck pallet deflection, ambient operating temperature, and unit loads ranging from 25 lbs tote bins up to 3,300 lbs heavy timber/composite GMA pallets.
To ensure system safety under international standards (RMI MH16.1, EN 15512, and FEM 10.2.02), cold-formed high-tensile carbon steel (ASTM A1011 equivalent or Q235B/Q355B) undergoes precision computerized roll-forming. Upright frames are engineered with variable column punch profiles, ensuring pitch adjustability without weakening the vertical load-bearing web.
OEM Manufacturing: We fabricate strictly according to your mechanical shop drawings, stamping your private brand logo onto load beams, column faces, and safety drop pins, while matching proprietary teardrop, slotted, or keyhole connector configurations.
ODM Engineering: Provide your building envelope, floor slab PSI, pallet weight range, and forklift aisle tolerances. Our structural design desk supplies complete 3D structural CAD layouts, FEA stress analyses, and stamped engineering documentation within 24 hours.
Parametric comparison of carton flow, heavy pallet gravity roller tracks, and hybrid push-back solutions.
| Structural Configuration | Roller Track / Bed Geometry | Load Capacity Rating | Brake System Architecture | Primary Industrial Sector |
|---|---|---|---|---|
| Light/Medium Carton Flow | Hardened PE/Nylon wheels on 50mm centers, cold-rolled galvanized steel C-channel | 50 – 150 kg/meter (35 – 100 lbs/ft) | Self-governing pitch friction / Entry end-stops | E-commerce, FMCG picking split-case, Lean Kanban |
| Heavy Dynamic Pallet Flow | Continuous electro-galvanized Ø60mm / Ø76mm steel rollers with precision 6204 ball bearings | 500 – 1,800 kg/pallet position | Centrifugal speed controller brakes every 1 pallet distance | Cold storage freezers, dairy, beverage mass dispatch |
| Nested Push-Back Roller Cart | Dual-flanged steel guide wheels rolling on inclined structural rectangular hollow tubing | 1,000 – 1,500 kg/lane (2-6 pallets deep) | Gravity counter-resistance on inclined nested rail profiles | Raw material staging, retail bulk goods, buffer bays |
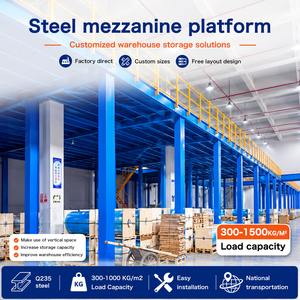
| Live Roller Chute & Mezzanine | Modular staggered multi-wheel beds integrated into structural steel mezzanine decks | 300 – 1,000 kg/m² uniform deck rating | Impact-resistant decelerator plates with hydraulic dampers | Distribution hubs, multi-level auto parts fulfillment |
How Tier-1 material handling procurement managers are balancing capital expenditure, supply-chain resilience, automation integration, and carbon footprint compliance.
Procurement teams are moving away from fixed roller tracks that require static forklift access. Next-generation RFQs require drop-in roller beds fitted with photoelectric sensors and automatic safety stops that align with autonomous mobile robots (AMRs) for touchless end-of-lane unloading.
With freezer energy consumption rising globally, distribution engineers prioritize gravity roller lanes that deliver dense FIFO storage without requiring truck exhaust fumes inside -25°C chambers. Low-temperature synthetic greases and zinc-plated structural steel guarantee maintenance-free roller rotation.
US and Canadian buyers require engineering packages calculated simultaneously in imperial (lbs/ft) and metric (kg/mm) units. Sourcing from manufacturers capable of supplying PE-stamped calculations compatible with local IBC (International Building Code) avoids costly permit delays.
Over 25 years of specialized structural fabrication, rigorous ISO 9001 certified batch testing, and high-volume containerized export infrastructure.
Every cold-formed upright and beam undergoes an automated sequence: chemical degreasing, industrial pickling, phosphating, pure water neutralization, followed by electrostatic thermosetting powder coating cured at 200°C. This ensures salt-spray resistance and zero paint peel under intense roller vibrations.
Send your building footprint, column grids, ceiling clear heights, and material flow volumes. Our senior rack architects return 2D layout drawings, 3D realistic rendering models, and comprehensive bill of materials (BOM) within 24 hours to streamline your procurement approvals.
We pack upright columns in heavy-gauge steel strapped bundles with protective corner angles, while beams, roller lanes, and small hardware components are palleted and shrink-wrapped. Every 40ft High-Cube container is maximized for cubic volume, saving up to 22% in transpacific landing costs.
Clear, technically rigorous answers covering load calculations, seismic certifications, cold-room dynamics, and ocean transit logistics.
Submit your facility dimensions, pallet specifications, and throughput targets. Our engineering department will return a comprehensive 3D CAD layout, load capacity calculation, and transparent landed quote within 24 hours.