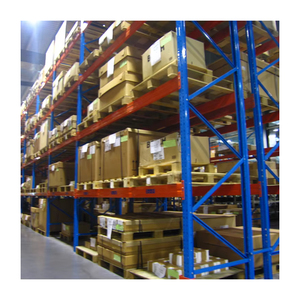
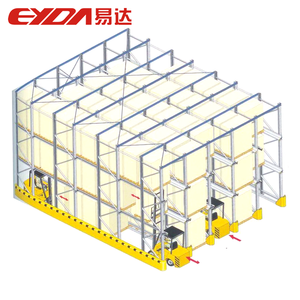
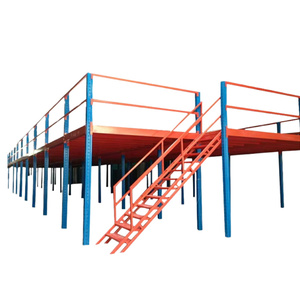
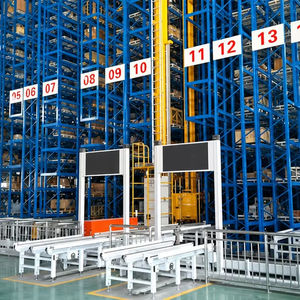
AS/RS Automated Storage and Retrieval System, High Bay Heavy Duty Pallet Rack
- Max Frame Height: Up to 40 meters
- Deflection Ratio: 1/200 - 1/300 tight
- Crane Guidance: Integrated guide rails
Manufactured from certified Q235B/Q355B structural steel, our industrial rack configurations are precision-engineered to maximize vertical cube utilization, handle extreme unit loads, and interface seamlessly with manual or automated handling machinery.
In modern high-throughput logistics terminals and automated distribution hubs, structural pallet racking is not merely static steel shelving; it is an engineered, load-bearing framework subjected to intricate combinations of axial dead weight, dynamic pallet drop impacts, seismic ground accelerations, and asymmetric live loads. Sourcing through qualified OEM/ODM industrial warehouse storage racks manufacturers requires rigorous evaluation of yield strengths, cold-forming tolerances, and FEA (Finite Element Analysis) deflection standards.
At Guangzhou Heda Shelves Co., Ltd., our engineering protocol relies strictly on primary certified prime hot-rolled coils slit and cold-rolled into structural channel sections (Q235B with minimum yield strength $f_y = 235 \text{ MPa}$, and high-tensile Q355B with $f_y = 355 \text{ MPa}$). For sub-zero cold chain freezers operating down to -30°C, we specify low-temperature impact tested structural grades (such as Q355D or Q355E) with Charpy V-notch energy thresholds rated to suppress ductile-to-brittle transitional cracking under shock loads.
Upright frame design incorporates cold-rolled profiles with multi-bend return lips. Every additional bend along the web and flange of the column increases its sectional modulus ($Z_{xx}$ and $Z_{yy}$) and radius of gyration ($r$), allowing superior torsional-flexural buckling resistance under seismic forces while eliminating excess dead tonnage from the storage installation.
| Racking Architecture | Nominal Load / Level | Aisle Clear Width | Space Efficiency | Stock Rotation | Automation Readiness |
|---|---|---|---|---|---|
| Selective Pallet Racking | 1,000 – 4,500 kg | 3,000 – 3,500 mm | 40% – 50% | 100% Selective | Forklift / Reach Truck |
| Double-Deep Pallet Rack | 1,000 – 3,200 kg | 3,000 – 3,300 mm | 60% – 65% | LIFO Mode | Pantograph Reach Truck |
| Drive-In / Drive-Thru | 1,000 – 2,000 kg | Lane Dedicated | 75% – 85% | FILO / FIFO | Counterbalanced Truck |
| Pallet Flow (Gravity Roller) | 800 – 1,500 kg | Loading / Picking Faces | 70% – 80% | Strict FIFO | Gravity Feed Brake Rollers |
| Radio Shuttle Storage System | 1,000 – 2,000 kg | Single Transfer Aisle | 80% – 90% | FIFO & LIFO | Semi-Automated Shuttle Cart |
| High Bay AS/RS Crane System | 500 – 3,000 kg | 1,400 – 1,700 mm | 90% – 95% | WMS Managed | Fully Automated Stacker Crane |
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a premier 30,000 m² (323,000 sq ft) manufacturing campus with 300+ seasoned specialists, delivering complete OEM/ODM engineering across five continents.
Over two decades of pure focus on pallet racking, cantilever systems, and multi-tier mezzanines. Our engineering library holds over 10,000 executed warehouse blueprints for food, pharma, chemical, and 3PL leaders.
Send us your architectural column grid, clear ceiling height, slab capacity, and pallet metrics. Our structural engineers generate complete 2D layout drawings, 3D spatial models, and itemized quotations within 24 business hours.
Fully certified quality control under ISO 9001:2015 (Cert No. 18624Q00169R0M) and Construction Products CE marking (No. 2435-CPR-8605159). Mill test certificates (MTC) with full chemical analysis accompany every steel heat batch.
Complete flexibility for private label branding, custom hole pitch (50mm, 75mm, 76.2mm teardrop), specialized powder coat RAL color palettes, and container loading schemes optimized for US, Canadian, and European ports.
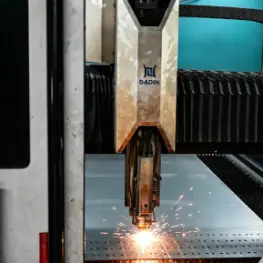
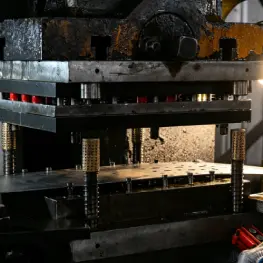
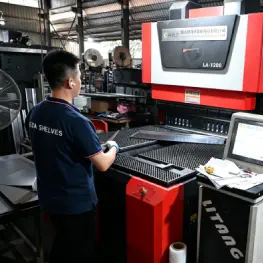
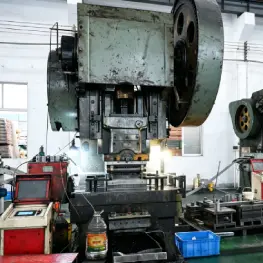
From raw coil slitting to automated electrostatic polymer curing, every mill roll-forming pass is monitored for dimensional consistency and metallurgical integrity.
Chemical composition analysis & yield stress testing of incoming steel coils.
High-speed longitudinal slitting lines cut wide master coils to target widths.
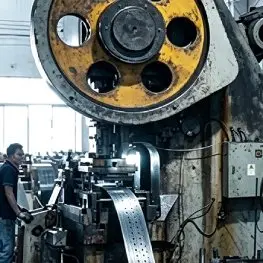
CNC multi-head progressive punch presses forge repeatable hole patterns.
Progressive mechanical break forming to create clean flange geometry.
Heavy roll-former stations shape box beams and multi-ribbed uprights.
Automated and manual edge deburring to prevent handling abrasions.
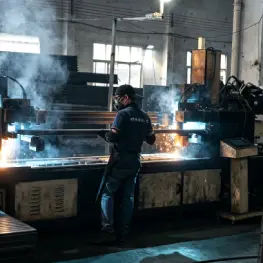
Automated robotic weld cells bond connector claws and heavy baseplates.
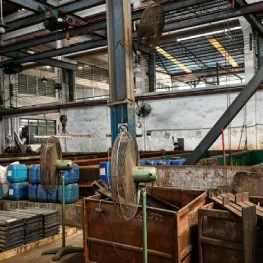
Multi-stage immersion pretreatment eliminates scale and maximizes resin bonding.
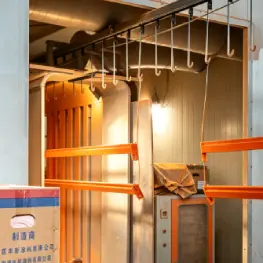
Uniform dry-powder spray booth cured at 200°C for corrosion-resistant 80μm film.
Thickness gauges, cross-cut adhesion tests, bundle strapping, and container stuffing.
Procurement directors and supply chain executives must adapt their storage asset acquisition strategies to combat rising industrial square footage costs, workforce shortages, and decarbonization mandates.
With prime industrial warehousing land values continuing to appreciate, procurement is transitioning from traditional 7-meter clear heights toward 12-to-30-meter high-bay installations. Maximizing vertical density per square meter reduces footprint overhead, local tax liabilities, and roof maintenance costs.
Storage structures must now be specified with robotic vehicle clearance in mind. Modern procurement requests demand tighter manufacturing tolerances (Class 100/200), bottom-tier cantilever pick tunnels, and precise guide rail placements that enable Autonomous Mobile Robots to retrieve unit loads without human intervention.
Multinational enterprises must increasingly disclose Scope 3 upstream emissions. Procurement managers actively favor OEM manufacturers utilizing electric arc furnace (EAF) steel coils, closed-loop zero-effluent chemical pretreatment systems, and heavy-metal-free thermosetting TGIC powder finishes.
Given geopolitical supply chain volatility, enterprise fulfillment centers require modular storage frameworks that can be disassembled, extended, or converted from pallet storage into multi-tier pick towers as consumer SKU velocity shifts between bulk wholesale and omnichannel split-case picking.
Breakthroughs in structural steel micro-alloying, seismic digital twinning, and embedded load monitoring are redefining the safety envelope and service life of modern industrial warehouse racking.
Modern racking engineering uses advanced non-linear dynamic FEA modeling under Site Class D, E, and F ground conditions. By simulating cyclic base shears, inelastic joint slip, and P-Delta lateral drift effects, engineers can optimize baseplate footings and anchor bolt embedment depths to ensure life-safety collapse prevention during severe seismic events.
By transitioning from plain carbon steels to micro-alloyed dual-phase and niobium-treated cold-rolled coils, manufacturers achieve yield strengths exceeding 420–550 MPa without compromising cold bend radius ductility. This metallurgy permits 15% to 22% structural weight reduction while enhancing column buckling resistance.
The integration of optical and piezoresistive strain gauges into critical lower-tier uprights provides real-time digital detection of forklift impacts and overload conditions. Cloud-connected sensors alert warehouse operations teams instantly to localized yielding, plumbness deviation, or excessive beam deflection before structural failure occurs.
Clear, definitive answers to the most common structural, compliance, and logistics questions encountered when sourcing industrial storage racks from an OEM/ODM manufacturer.
Every beam profile and column section is certified in accordance with ANSI MH16.1 (RMI) or EN 15512 standards. We execute physical destructive load testing, finite element beam calculations, and provide signed engineering load tables certifying the allowable uniformly distributed load (UDL) at an L/180 or L/200 deflection limit with a minimum safety factor of 1.65.
Yes. Our automated CNC punching and roll-forming dies support standard American 2-inch punch pitch Teardrop systems, European 50mm and 75mm pitch diamond hole patterns, as well as heavy Australian 76.2mm hole spacing. OEM private-label branding, connector stamping, and custom column geometries are fully supported.
Yes. We supply comprehensive structural calculation calculation books, component sectional property analyses, anchor shear/tension interaction checks, and detailed shop drawings. These documents are compiled to enable your local registered Professional Engineer (PE) or structural engineer of record (SE) to review, stamp, and submit for municipal building and fire permits.
Racking uprights are packed horizontally on specialized wood or steel dunnage with protective corner board protectors, heavy polyester strapping, and stretch film wrapping. Beams are nested with inter-layer foam barriers to prevent powder coating abrasion. Fasteners, baseplates, and hardware are crated in seaworthy, moisture-barrier wooden cases with clear container packing lists.
Following final sign-off of CAD layout drawings and production shop sheets, typical manufacturing lead time ranges from 20 to 35 business days. With a 30,000-ton monthly capacity across multiple roll-forming lines, HEDA can stagger container dispatch to align with the installation contractor's progressive erection sequence on site.
Our layout designs incorporate engineered row spacers that maintain code-mandated 6-inch (150mm) to 12-inch (300mm) longitudinal flue spaces between back-to-back rack rows. We also supply wire mesh decking, pallet stops, and drop-in transverse flue keepers to ensure in-rack sprinkler water can penetrate uninhibited down through the storage matrix in an event of fire.
Collaborate directly with Guangzhou Heda Shelves' dedicated engineering department. Send us your facility dimensions, unit pallet weights, and operational specifications to receive a free CAD floor layout, 3D visualization, and detailed manufacturer-direct quotation within 24 hours.