Product Portfolio
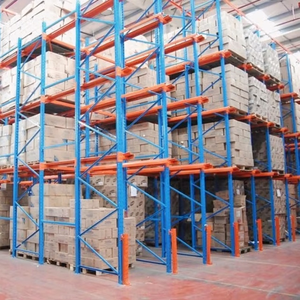
Featured Industrial Pallet Racking & High-Density Storage Systems
Precision cold-formed high-tensile steel racking modules engineered for heavy industrial distribution centers, cold chain freezers, and automated warehouse environments.
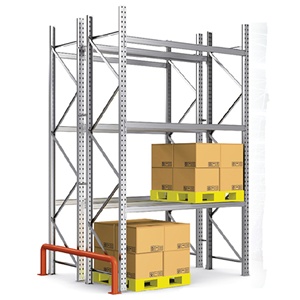
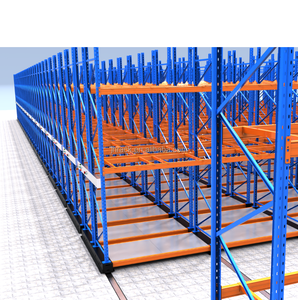
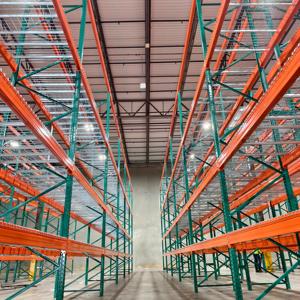
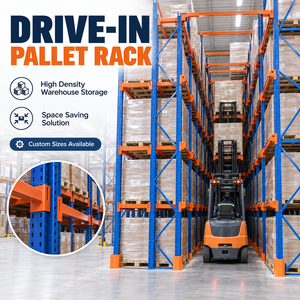
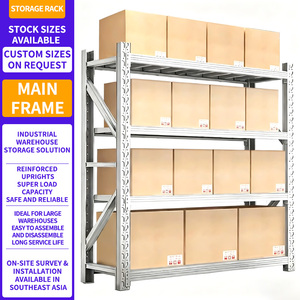
Engineering Authority
Structural Mechanics of Drive-In vs. Drive-Through Racking Systems
A comprehensive architectural evaluation of high-density static storage systems, focusing on cantilever rail moment capacity, top-tie torsional stiffness, and dynamic forklift interactions.
Cantilever Rail & Bracket Arm Dynamics
Unlike selective systems that transfer uniform distributed loads across horizontal box beams, Drive-In and Drive-Through systems rely on continuous side-mounted cantilever support rails. Each pallet rests directly on cold-formed guide rails anchored via multi-tooth heavy-duty bracket arms to vertical upright columns. This creates continuous eccentric torsion on the upright posts. Our OEM engineering calculates combined bending and axial compression stresses using finite element analysis (FEA) under ANSI MH16.1 and EN 15512 specifications, ensuring safety factors exceeding 1.65 under rated working payloads.
Top Tie & Back Portal Frame Bracing
The structural vulnerability of drive-in racking arises from the elimination of standard intermediate cross-aisle horizontal beams to accommodate forklift entry. To prevent longitudinal rack sway and lateral buckling, our structural engineers introduce high-tensile top-tie portal frames, transverse overhead bracings, and rigid rear-tower X-bracing networks (for Drive-In LIFO configurations). In Drive-Through configurations where pallets enter one side and exit the opposite for strict FIFO compliance, back bracing is physically impossible; we compensate using heavy-wall structural tubular top portals and oversized floor anchor anchorages.
Impact Protection & Floor Guide Rails
Because counterbalanced or reach forklifts navigate deep inside pallet lanes, impact fatigue at aisle-entry columns is the leading cause of structural failure. HEDA Shelves integrates standard 100×50×5mm or heavy-duty 120×80×6mm rolled structural steel floor guidance tracks that serve dual functions: guiding forklift wheels precisely along lane centerlines to avoid upright contact, and transferring horizontal impact energy directly to concrete foundations rather than rack upright assemblies. Heavy-duty wrap-around column protectors fabricated from 6mm hot-rolled Q355B steel are standard on all lane entries.
25+
Years Engineering Expertise
30,000 m²
Advanced Manufacturing Plant
30,000 t
Monthly Steel Output Capacity
10,000+
Global Turnkey Projects Built
Architectural Matrix
Engineering Matrix: High-Density Pallet Racking Comparative Analysis
Evaluate structural throughput, space cubic volumetric utilization, and operational equipment criteria across commercial warehousing systems.
| Racking Topology | Inventory Rotation | Floor Space Utilization | Pallet Selectivity | Forklift Cycle Velocity | Ideal Procurement Scenario |
|---|---|---|---|---|---|
| Drive-In Pallet Racking | LIFO Last-In, First-Out | 75% - 85% (High Density) | Low (Per-lane single SKU) | Moderate (3.5 - 5 min/lane) | Bulk homogeneous stock, cold room freezers, seasonal production |
| Drive-Through Pallet Racking | FIFO First-In, First-Out | 70% - 80% (High Density) | Medium-Low (Entry vs Exit) | Moderate (Dedicated ingress/egress) | Perishable food, cold chain distribution, strict date rotation logistics |
| Radio Shuttle Cart Racking | FIFO & LIFO Dual Capable | 85% - 90% (Max Static) | Medium (Shuttle automated lane) | Fast (Forklift never enters lanes) | High-throughput distribution, beverage bottling, automated deep-lane |
| Push Back Pallet Racking | LIFO Nested Cart Gravity | 65% - 75% (Medium-High) | Medium (2–6 pallets deep/lane) | High (Face-aisle only pickup) | Fast-moving retail goods, 3PL batching, multi-SKU medium volume |
| Pallet Flow (Gravity Roller) | FIFO Pure Dynamic Flow | 75% - 85% (Continuous Flow) | High pick face access | Very High (Automatic feeding) | Pharmaceutical DCs, high-turnover FMCG, manufacturing buffers |
| Standard Selective Racking | 100% Selective Any Mode | 40% - 45% (Low Density) | 100% Direct Individual Access | Immediate individual access | E-commerce, 3PL universal SKU hubs, low-volume high-diversity stock |
Market Intelligence
Procurement & Engineering Trends: High-Density Warehousing 2025–2030
Anticipate evolving seismic building standards, AGV automated guided forklift compatibility, and structural carbon efficiency in your next warehouse expansion.
1. Hybrid AGV/AMR Autonomous Counterbalance Integration
Traditional drive-in systems were built for manual forklift navigation with generous human clearance. The 2025–2030 procurement cycle is characterized by retrofitting drive-in and drive-through systems for automated guided vehicles (AGVs) and autonomous reach trucks. This transformation requires millimeter-tolerance roll-forming, laser-aligned floor guide rails, integrated optical positioning reflectors on bracket arms, and enlarged pallet entrance funnels. HEDA Shelves designs custom OEM profile geometries optimized specifically for lidar reflection and robotic pallet positioning.
2. Stringent Seismic Zoning & Ductile Base Anchor Design
With North American building codes (IBC 2024 / ASCE 7-22) and European Eurocode 8 updating seismic risk models, high-density racking designs must incorporate higher ductility reduction factors. Because drive-in racking possesses low inherent portal framing damping along the entry axis, our engineering team supplies heavy structural ductile baseplates with dual embedment chemical epoxy anchors (Hilti / Fischer systems), engineered yield zones, and thickened cold-formed post gauges (up to 3.0mm Q355B high-strength alloy) to satisfy strict local Professional Engineer (PE) stamped reviews.
3. Sub-Zero Cold Chain Optimization & Anti-Corrosion Finishes
Cold chain logistics operations are modernizing to counteract soaring refrigerated kilowatt-hour costs. Drive-in systems in -25°C to -30°C frozen storage represent the highest ROI per cubic meter. However, condensation cycling demands superior metallurgy. HEDA Shelves utilizes automated 10-stage pre-treatment with zirconium nanotechnology phosphating followed by thermoset electrostatic TGIC-free polyester powder coating (80–110μm), or continuous hot-dip galvanizing (ISO 1461) to guarantee zero embrittlement, zero micro-cracking, and maximum rust prevention under harsh thermal shock.
Manufacturing Excellence
Why Global Distributors & Project Integrators Choose HEDA Shelves
From raw coil slitting to automated robotic welding and export container crating, our 30,000 m² facility delivers end-to-end industrial storage manufacturing.
Raw Steel Traceability & Certification
We source prime hot-rolled structural steel coils exclusively from top-tier tier-1 mills (Baosteel, Shougang). Every batch is mechanically and chemically tested for tensile yield strength, elongation, and charpy impact tolerance, verified with 3.1 Mill Test Certificates (MTC).
Full OEM & ODM Custom Engineering
Whether you require standard 50mm / 75mm European pitch, 76.2mm (3-inch) American teardrop punched uprights, or proprietary custom beam connector profiles for private label distributors, our tool and die division builds custom progressive tooling in-house.
Rigorous International Quality Assurance
Certified under ISO 9001:2015 (Certificate 18624Q00169R0M), CE Marking (2435-CPR-8605159) for structural steel construction products, and RoHS material safety compliance. Every production run undergoes automated ultrasonic weld tests and 500-hour salt spray analysis.
Export Dunnage & Container Nesting
Our logistics team engineers custom container packing models in 3D CAD to maximize freight cube. Uprights and guide rails are interleaved with protective corrugated wraps, strapped with heavy polyester banding, and supported on wooden dunnage for damage-free maritime shipping.
Procurement Knowledge Base
Frequently Asked Questions: Sourcing Drive-In Racking Systems
Detailed technical and logistical considerations for procurement directors, operations managers, and warehouse systems integrators.
What is the structural difference between Drive-In and Drive-Through racking systems?
While both systems use identical cantilever rail principles to support pallet loads along deep storage bays, their operational topology and structural stability differ completely:
- Drive-In Pallet Racking: Operates on a Last-In, First-Out (LIFO) inventory model. Forklifts enter and exit through the same front loading aisle. Because the rear end of the lane is closed, structural engineers can incorporate comprehensive back diagonal cross-bracing (X-bracing) between rear uprights. This provides exceptional longitudinal shear stiffness and horizontal wind/earthquake restraint.
- Drive-Through Pallet Racking: Operates on a First-In, First-Out (FIFO) inventory model. Forklifts load from one dedicated aisle and retrieve pallets from the opposite aisle. Because both ends must remain open for vehicle transit, back cross-bracing cannot be utilized. Instead, the system relies on reinforced overhead portal bridge ties, heavier box-section tie beams, and stiffened floor baseplate column anchorages to achieve equivalent structural rigidity.
What minimum aisle widths and forklift clearances are required inside drive-in lanes?
Forklift clearance calculations inside drive-in lanes must consider three critical dimensions:
- Overall Forklift Chassis Width: The overall outside width of the forklift (including mast and overhead guard) must typically be at least 150mm to 200mm (6–8 inches) narrower than the clear width between left and right pallet support arms.
- Pallet Overhang: The system must account for pallet overhang (typically 50mm on either side). The pallet support rail must provide at least 75mm to 100mm of secure bearing width under the pallet runner/stringer.
- Mast Clear Height: Collapsed mast height must clear the lowest pallet support rail level, and maximum lift height must accommodate the top tier pallet plus an additional 150mm to 200mm of vertical lift clearance to lift pallets off the support rails during extraction.
Can HEDA Shelves manufacture racking according to imperial measurements and North American codes?
Yes. A significant portion of our export volume serves the United States, Canada, and Mexico. We routinely manufacture systems to standard North American imperial dimensions:
- Pallet Compatibility: Engineered specifically for standard 48" × 40" GMA (Grocery Manufacturers Association) wood pallets, 48" × 48" drums/IBC containers, and custom plastic pallets.
- Imperial Upright & Beam Profiles: Frame depths configured to 42", 44", or 48", column heights up to 40 feet in single seamless cold-formed lengths, and teardrop hole punching patterns with 2" or 3" vertical adjustment increments.
- Engineering Calculations: Structural calculation books and component load capacity ratings provided in pounds (lbs), feet (ft), and square inches (sq in), completely prepared to assist your registered local Professional Engineer (PE) in stamping architectural permits under ANSI/RMI MH16.1.
How does HEDA handle sub-zero cold room environments and coating longevity?
Refrigerated warehouse facilities operating between 0°C and -30°C present severe risks of thermal condensation, paint delamination, and low-temperature steel embrittlement. HEDA Shelves safeguards cold chain projects through specialized materials and processing:
- Silicon-Killed Structural Steel: We specify certified steel grades with guaranteed low-temperature Charpy V-notch impact toughness to prevent brittle fracture under operational forklift vibration.
- Advanced Surface Pre-Treatment: Steel parts pass through a 10-step immersion line including alkaline degreasing, acid pickling, micro-etching, and high-density phosphating.
- TGIC-Free Electrostatic Powder Coating: Applied at 80–110 microns thickness with controlled high-temperature curing to form an impervious barrier against moisture penetration. For high-humidity blast freezers, complete hot-dip galvanization according to ISO 1461 (minimum 65–85 microns zinc thickness) is available.
What project parameters are required to receive a free 24-hour CAD design & turnkey quote?
To provide an optimized engineering layout and an itemized factory-direct quote within 24 hours, our design department requests the following data:
- Building Architectural Drawing: Length, width, clear ceiling height under roof trusses, column grid locations, dock door locations, and fire sprinkler clearances.
- Pallet Specification: Length (depth), width (front face), overall loaded height, and maximum load weight per pallet position (including pallet weight).
- Material Handling Equipment: Forklift type (counterbalance, reach truck), collapsed mast height, maximum lifting height, and overall turning radius.
- Operating Environment: Ambient dry warehouse, refrigerated cold storage (temperature in °C/°F), or chemical processing environment, plus local seismic design requirements if known.