Engineering Authority • ISO 9001:2015 & CE Certified

China Top Case Flow Rack Manufacturer & Suppliers

OEM & ODM High-Density Dynamic Gravity Flow Storage Solutions Engineered for Peak Order Fulfillment, Ergonomic Carton Picking, and Maximum Floor Space Utilization.

25+
Years of Precision Racking
Manufacturing industrial warehouse racking & flow systems since 2001.
30,000t
Monthly Steel Capacity
Cold-roll forming, automated punch lines & robotic laser welding lines.
10,000+
Completed Global Projects
Supplying multi-tier picking & pallet systems throughout North America & EMEA.
323ksq ft
Integrated Campus
Guangzhou production plant featuring automated electrostatic powder coating.
High-Performance Warehouse Systems

Precision-Formed Storage & Case Flow Racking Systems

Explore our industrial-grade storage solutions manufactured from Q235B cold-rolled structural steel, optimized for first-in-first-out (FIFO) case picking, heavy-duty pallet handling, and high-density inventory staging.

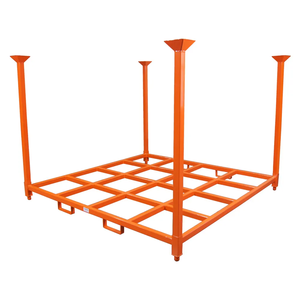
Stackable Inverted Style Metal Pallet Stack Rack

Warehouse Storage Inverted Style Rack Metal Pallet Stack Rack

Removable, nestable post racks providing flexible high-density vertical storage without bolting into concrete slabs.

  • 1,500 kg Load / Layer
  • Hot-Dip Galvanized / Powder Coated
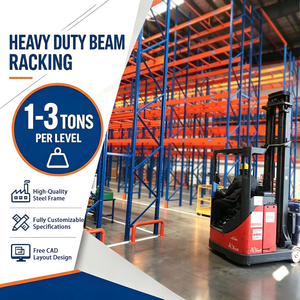
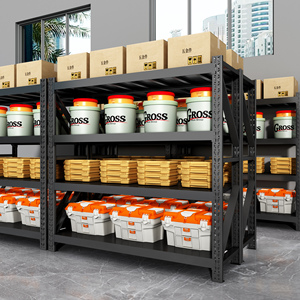
Heavy-Duty Heavy Duty Steel Pallet Rack Industrial Storage System

Custom Heavy Duty Steel Pallet Rack Industrial Storage System

High-capacity teardrop or boxed upright framing with 100% selective access for GMA, Euro, and customized pallet configurations.

  • Up to 4,000 kg / Level
  • Seismic-Engineered Profiles
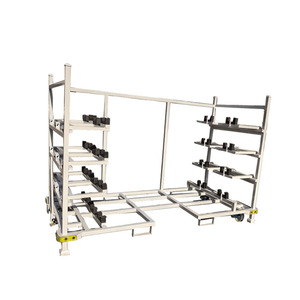
Logistics Automobile Parts Workstation Stacking Turnover Racks and Logistics Trolleys

Automobile Parts Workstation Stacking Turnover Racks & Trolleys

Custom-engineered production-line turnover carts and dunnage racking engineered specifically for line-side automotive part assembly.

  • Custom Dunnage
  • Ergonomic Tow-Bars
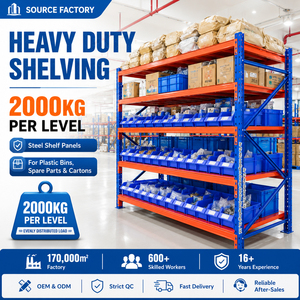
Adjustable 2000KG Adjustable 5 Storage Levels Heavy Duty Shelving System

2000KG Adjustable 5-Level Heavy Duty Steel Panel Racking

Versatile medium-and-heavy span modular shelving featuring rigid step beams, solid panel decking, and 50mm pitch adjustability.

  • 2,000 kg Beam Load
  • Modular Steel Decking
Core Product 5-Layer Carton Gravity Case Flow Rack

Heavy Duty 5-Layer Carton Gravity Case Flow Rack (CE Certified)

High-efficiency case flow system featuring aluminum roller tracks, dynamic lane dividers, and impact-resistant entry guides for split-case picking.

  • True FIFO Picking
  • Engineered Roller Beds
Gravity Flow Gravity Flow Pallet Racking System

Industrial Gravity Flow Pallet Storage Racking System

Multi-roller lanes with centrifugal brake rollers and speed controllers to gravity-feed loaded pallets smoothly from replenishment aisle to retrieval face.

  • Centrifugal Speed Retarders
  • Separator Separator End-Stops
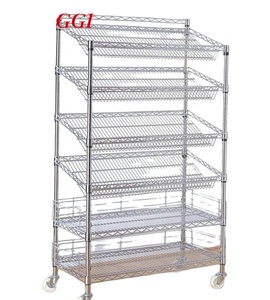
Split-Case Pick Light Duty Wire Basket Shelving Wire Rack Shelving

Light Duty Wire Basket Shelving & Industrial Wire Rack

Chromed or powder-coated wire shelving systems tailored for dust-free staging, retail micro-fulfillment, and sterile inventory pick locations.

  • Air & Sprinkler Permeable
  • Tool-Free Shelf Spacing
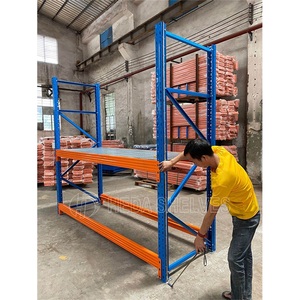
Heavy-Span Heavy Duty Metal Pallet Storage Racking 1000kg-3000kg

Heavy Duty Metal Pallet Storage Racking (1,000–3,000kg / Layer)

High-tensile beam and column configurations with 5-tooth connection claws, safety pins, and integrated row spacers for industrial multi-tier distribution.

  • Continuous Roll Formed
  • ISO / CE Compliant Profiles

Case Flow Rack Engineering Architecture & Operational Dynamics

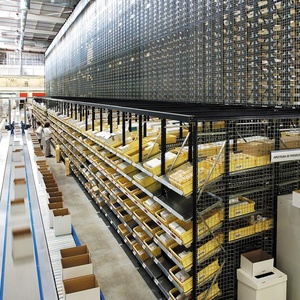
In high-throughput e-commerce fulfilment centres, 3PL logistics hubs, and fast-moving consumer goods (FMCG) facilities, static shelving represents a severe labor bottleneck. As order volume increases, picking travel time accounts for up to 65% of an order selector's daily active shift. Case flow racks—also known throughout the material handling industry as carton flow racks—transform conventional static storage into dynamic, gravity-fed picking faces.

Manufactured using cold-formed structural uprights and dedicated intermediate shelf frames, case flow racks incorporate inclined roller tracks or polycarbonate wheel beds pitched between a 2.5% to 5.0% gradient. Tote boxes, cartons, and plastic bins are loaded from the rear replenishment aisle (charging side) and roll automatically via gravity down to the forward picking face (discharging side). When a picker retrieves the front carton, the trailing inventory glides forward to index into position immediately.

Strict FIFO Rotation

Enforces automatic first-in, first-out stock turn. Eliminates batch obsolescence, spoiled shelf-life goods, and fragmented inventory clusters.

Aisle Separation & Safety

Decouples stocking and order selection. Restockers load from rear replenishment corridors without impeding forward pickers or causing forklift cross-traffic collisions.

Density & Footprint Savings

Condenses up to 40 distinct pick SKUs into a single bay opening, eliminating unused travel aisles and recovering up to 50% of active square footage.

Comparative Engineering: Case Flow Rack vs. Alternative Order-Picking Systems

Material handling directors and warehouse supply chain planners must weigh case flow racks against traditional static shelving, selective pallet racks, and automated AS/RS carousels. The matrix below defines the engineering trade-offs across capital intensity, ergonomics, and SKU accessibility:

System Type SKU Density Pick Travel Efficiency Inventory Rotation Restock Interference CAPEX per Pick Face
Case Flow Rack (Gravity Track) Ultra High (4–12 Cartons Deep) Minimized (Compact Pick Wall) Strict FIFO (100% Gravity Enforced) Zero (Dedicated Rear Loading) Moderate (Fast 6–14 Mo. ROI)
Static Industrial Shelving Low to Medium (1 Deep) Extensive (High Footprint Travel) LIFO or Manual Oversight Severe (Shares Same Front Aisle) Low (High Ongoing Labor Cost)
Selective Pallet Racking Low for Broken-Case Picking Extremely Wide Aisle Traversal Random / Batch LIFO Forklift Conflicts with Pedestrians Low Initial Capex
Multi-Tier Mezzanine Picking Very High (Vertical Utilization) Moderate (Vertical Elevators / Stairs) Flexible Configuration Separated Zones Moderate to High
Automated Mini-Load AS/RS Maximum Vertical Stacking Automated to Picker (Goods-to-Person) System-Software Controlled Fully Automated Induction Very High ($$$$ Capital Intensive)

Future Technology Trends in Case Flow Rack Design (2025–2030)

The manufacturing landscape for case flow racking in China is shifting from purely structural cold-rolled steel profiles toward intelligent, digitized, and hybrid material handling ecosystems. Procurement managers evaluating supply partners must account for the following technological evolutions:

1. Direct Integration with Pick-to-Light (PTL) and Vision Systems

Next-generation case flow tracks now feature pre-punched mounting raceways designed specifically for wireless Pick-to-Light modules, LED guidance strips, and digital order-confirmation pushbuttons. By directing operators visually to the precise pick lane and display quantities, picking errors drop below 0.01% while throughput rates exceed 350 to 500 lines per picker hour.

2. Autonomous Mobile Robot (AMR) & AGV Charging Interfaces

Warehouses are increasingly deploying AMRs for cross-dock replenishment. Top Chinese racking manufacturers engineer case flow racks with reinforced loading side entry funnels, precision dock plates, and RFID transponder mounts, allowing autonomous forklifts or tugger trains to deposit plastic tote bins directly into gravity roller tracks without manual human lifting.

3. Low-Friction Thermoplastic & Anti-Static (ESD) Roller Engineering

In electronics, semiconductor, and medical distribution facilities, electrostatic discharge can destroy delicate assemblies. Contemporary case flow tracks utilize conductive polymers (surface resistivity < 106 Ω) mounted on high-grade galvanized steel side channels. Dual-radius roller geometries prevent lateral carton drift and ensure smooth movement of paper boxes even under high humidity conditions.

Strategic Case Flow Rack Procurement Trends & Sourcing Framework

When selecting a primary China Case Flow Rack Manufacturer & Supplier, North American and European procurement teams must bypass middlemen and audit core manufacturing proficiencies. Racking that suffers weld micro-cracking, substandard powder paint curing, or roller pitch binding causes costly operational shutdowns.

Steel Certified Metallurgy

Always mandate mill test certificates confirming Q235B or Q355B prime high-tensile steel coils with verified carbon, silicon, manganese, and phosphorus content.

Roller Pitch & Deflection

Validate that roller axle centers align with package bottom profiles. Box sagging (pillow effect) will halt gravitational rolling if pitch calculations are defective.

Finishing & Salt-Spray Testing

Insist on automated shot blasting followed by 10-step pickling, phosphating, and electrostatic powder curing (60–80μm thickness) to resist impact abrasion.

Factory Direct Precision Since 2001

Guangzhou Heda Shelves Co., Ltd. Manufacturing Authority

Founded over 25 years ago, HEDA Shelves operates a state-of-the-art 30,000 square meter (323,000 sq ft) industrial manufacturing campus in Guangzhou, backed by over 300 experienced technical staff and dedicated storage engineers.

We are a true single-source factory partner for warehouse distribution projects in the United States, Canada, Mexico, and global distribution hubs:

  • 30,000 Metric Tons Monthly Capacity: Automated slitting, roll forming, punching, and certified robotic welding stations running multiple shifts.
  • Imperial & Metric Engineering Drawings: Comprehensive 3D CAD design, load engineering calculations (lbs/level and kg/level), and stamped-ready documents within 24 hours.
  • Global Export Logistics Optimization: Container packaging engineered to maximize shipping cubic volume and prevent transit scuffing, shipped directly to Long Beach, Houston, Savannah, Vancouver, and Newark.
  • Verified Quality Standards: Accredited with ISO 9001:2015 Quality Management System (Cert: 18624Q00169R0M) and CE Marking (No. 2435-CPR-8605159).
Inquire Now
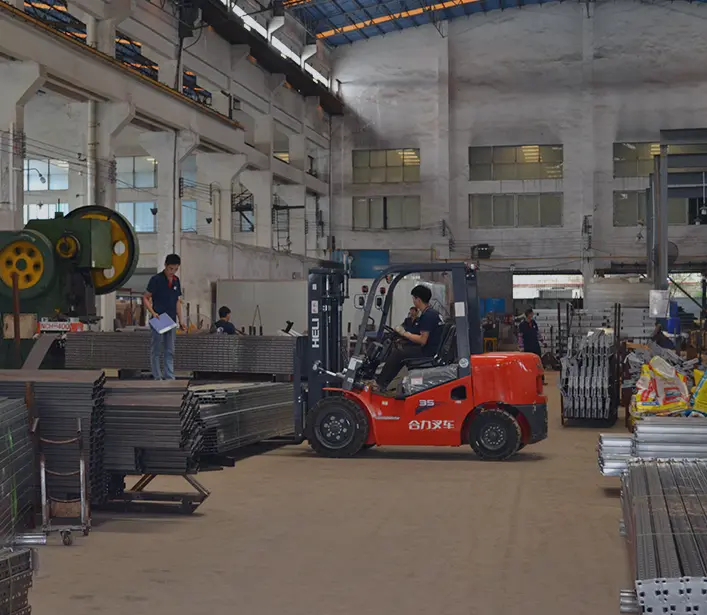
HEDA Shelves Racking Factory Production Floor
Automated Manufacturing Base

Continuous CNC cold-roll upright lines, automated electrostatic powder coating & quality testing lab.

Expert Solutions

Case Flow Rack Procurement & Engineering FAQ

Detailed technical answers addressing engineering tolerances, incline geometry, container shipping logistics, and building code approvals.

How do you determine the correct slope and roller pitch for case flow racks?
The ideal track incline typically ranges between 2.5% to 5.0% (approximately 1/4 to 1/2 inch of drop per foot of track run). The exact angle is governed by package weight, bottom surface rigidity, and carton material. Rigid plastic tote boxes roll freely at smaller gradients (2–3%), whereas corrugated boxes with soft bottoms or heavy contents may require a 4–5% incline. HEDA engineers test sample cartons to determine the precise roller spacing so that at least three rollers are in contact with the carton base at all times, preventing indentation and flow blockage.
Can case flow racking beds be retrofitted into existing selective pallet rack frames?
Yes. We design case flow shelf tracks and universal wheel beds to drop directly into standard roll-formed step beams or structural channel beams. Our brackets clamp securely into front and rear beams using heavy-duty adjustable clips, enabling warehouses to convert lower pallet rack pick levels into dynamic case flow storage while preserving high-bay bulk pallet storage overhead.
How does your factory accommodate North American seismic and building permits?
HEDA Shelves supplies full structural calculations, steel section properties, yield test certifications, and detailed CAD layout drawings formatted in both imperial (lbs, inches, feet) and metric units. These documents are tailored for seamless review by your regional Registered Professional Engineer (Engineer of Record), who provides seismic stamping in compliance with RMI (Rack Manufacturers Institute) guidelines and local IBC codes.
What is the standard manufacturing lead time and ocean container shipping schedule?
Standard factory production time runs between 15 to 25 days following signed approval of CAD drawings. All components are steel-banded, corner-protected, and palletized for 20ft and 40ft high-cube ocean containers. Transit times from our Guangzhou port facility average 14–22 days to West Coast ports (Los Angeles/Long Beach, Vancouver) and 28–35 days to East Coast and Gulf ports (Houston, Savannah, New York).
What finishes and coatings are provided for extreme environments or cold storage?
For ambient industrial distribution, components receive our standard multi-stage zinc-phosphate pretreatment and thermoset polyester powder coating cured at 180°C. For refrigerated coolers, sub-zero freezers, or high-humidity outdoor applications, we supply hot-dip galvanization (HDG compliant with ASTM A123) and high-impact plastic/nylon rollers that retain elasticity and eliminate brittle fracture down to -30°C (-22°F).
Can lane widths and dividers be reconfigured as product packaging dimensions change?
Absolutely. Our full-width roller assemblies and track-style case flow shelves utilize snap-in, tool-free zinc-plated steel lane dividers and entry guides. Warehouse maintenance technicians can adjust lane dividers horizontally in increments of 10mm (0.4 inches) to match new packaging sizes within minutes, offering long-term flexibility as SKUs rotate.

Transform Your Warehouse Order Picking Efficiency Today

Consult with senior storage engineers at Guangzhou Heda Shelves Co., Ltd. Submit your warehouse dimensions, clear height, and SKU carton specifications to receive a complete 2D/3D CAD design layout and itemized FOB/CIF quotation within 24 hours.

Inquire Now