EN 15512:2020 & ISO 9001:2015 Structural Compliance
CE Certified Pallet Racking System Warehouse Manufacturer & Factory
Industrial-grade high-bay structural engineering, precision roll-forming, and high-density material handling systems designed for mission-critical logistics hubs worldwide.
Engineered Storage Portfolio
Standard & Heavy-Duty Certified Pallet Racking Series
Direct factory configurations manufactured from high-yield Q235B structural steel, strictly tested according to FEM 10.2.02 and EN 15512 standards for maximum structural reliability, dynamic stability, and high seismic zone resistance.
Structural Integrity & European CE Conformity (EN 15512:2020)
Industrial pallet racking is not merely static steel shelving; it is an engineered structural system subject to extreme live loading, dynamic horizontal seismic acceleration, cyclic operational impacts, and progressive deflection thresholds. As an export-oriented certified manufacturer, HEDA Shelves engineers every racking element according to EN 15512:2020 (Steel static storage systems – Specification of beam-and-upright pallet racking systems) and RMI MH16.1 specifications.
Our upright columns are cold-roll-formed with continuous closed or semi-closed multi-rib geometry using premium certified Q235B and Q355B hot-rolled structural steel coils. The metallurgical properties guarantee high tensile yield strength (min. 235–355 MPa) and superior elongation under catastrophic earthquake ground movement. Through Finite Element Analysis (FEA) computer modeling, our structural engineers evaluate second-order P-Delta effects, sway stability, and torsional buckling limits to ensure an absolute safety factor exceeding 1.65 to 1.95 under maximum allowable unit load conditions.
Every connector incorporates heavy-duty cold-stamped multi-claw hooks with integrated automatic safety lock pins to prevent accidental beam dislodgement caused by improper forklift mast retraction. Furthermore, beam deflection under design load is strictly constrained within the L/200 limit (where L represents clear span length), fully protecting automated handling equipment from binding or premature operational fatigue.
EN 15512:2020 Validated
CE CPR-8605159 Certificate
ISO 9001:2015 Monitored
30,000
Metric Tons Monthly Capacity
323,000
Sq Ft Production Facility
Seismic & Mechanical Engineering Deliverables:
Comprehensive CAD elevation & floor plan layouts (ft/in or mm)
Stiffness matrices for local PE/Engineer of Record review
Floor anchor slab point load & shear load calculations
NFPA 13 longitudinal & transverse flue space compliance
Pallet Racking System Operational & Engineering Matrix
Compare pallet selectivity, cubic volume utilization, throughput dynamics, and specialized handling equipment constraints to select the optimal racking architecture for your facility footprint.
System Type
Pallet Selectivity
Floor Space Efficiency
Stock Rotation
Typical Beam Load
Forklift Compatibility
Optimal Industry Application
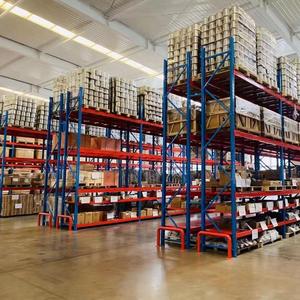
Selective Pallet Racking
100% Direct Access
40% – 45% Floor Area
FIFO / LIFO Any
1,000 – 4,500 kg
Standard Counterbalance, Reach
FMCG, 3PL Distribution, High SKU Variety
Double Deep Racking
50% Immediate Access
55% – 65% Floor Area
LIFO Priority
1,200 – 3,200 kg
Pantograph Pantographic Reach Truck
Cold Storage, Paper Rolls, Medium SKU counts
Drive-In / Drive-Thru
20% – 30% Access
70% – 80% Floor Area
LIFO (Drive-In) / FIFO
1,000 – 2,000 kg/level
Counterbalance, Narrow Reach
Seasonal Bulk Goods, Deep Freezer Warehouses
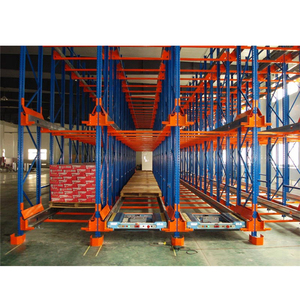
Automated Radio Shuttle
Channel Face Access
80% – 88% Floor Area
Flexible FIFO or LIFO
1,500 kg / pallet
Standard Forklift (Outside Lane)
High-Volume Food, Cold Chain Logistics, Beverages
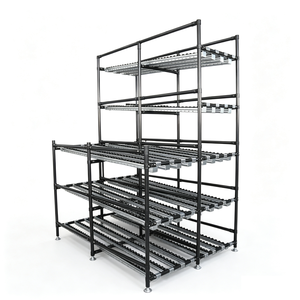
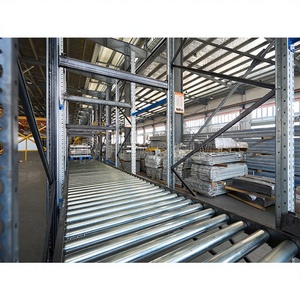
Pallet Flow (Gravity)
Pick Face Dedicated
75% – 85% Floor Area
Enforced Strict FIFO
1,000 – 1,500 kg/lane
Counterbalance (Inlet) & Reach (Outlet)
Perishable Dairy, Pharma, High-Turnover Buffer
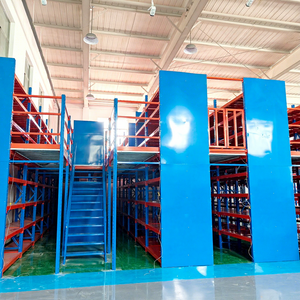
Rack-Supported Mezzanine
Multi-Level Access
180% – 260% Usable Footprint
Tiered Hybrid SKU
300 – 1,000 kg/sqm floor
Pallet Jacks, VRC Lift, Conveyors
Auto Spare Parts, E-Commerce Each-Pick Sorting
Heavy Cantilever System
100% Column Front Access
50% – 60% Linear Span
Continuous Linear
500 – 3,500 kg/arm
Side Loaders, 4-Way Multi-Directional
Structural Steel, Extrusions, Timber, PVC Pipes
Forward-Looking Procurement
Emerging Trends Shaping Global Warehouse Racking Procurement
Strategic supply chain investments demand infrastructure built to outlast cyclic market shifts. Industrial distribution facilities must incorporate flexibility, automation readiness, and carbon-efficient supply chains.
Automation Hybridization & AMR Readiness
Warehouses are shifting from pure manual forklift handling to hybrid ecosystems where Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs) work alongside selective and shuttle racks. Future-proof procurement requires ultra-tight beam fabrication tolerances, floor track leveling considerations, and integrated sensor clearance.
With industrial real estate costs soaring globally, procurement teams are abandoning standard 6-meter ceiling layouts for 12 to 20-meter high-bay installations. This necessitates reinforced heavy-gauge structural uprights, high-capacity baseplate anchoring, and narrow aisle (VNA) laser-guided truck integration to unlock 400% greater density per acre.
Procurement directors are actively navigating tariff structures, localized building code certifications, and steel price volatility. By working directly with integrated manufacturers like HEDA Shelves, enterprises eliminate distributor markups and secure certified low-emissions powder coating that satisfies strict corporate ESG environmental compliance.
The Engineering Evolution of Modern High-Bay Storage
Examine how conventional static pallet racking has transformed into dynamic, semi-automated structural systems engineered for higher velocity and reduced labor dependencies.
From Static Selective to Deep-Lane Density
Early distribution operations relied exclusively on static wide-aisle selective layouts where over 55% of floor space was consumed by forklift travel lanes. Today, drive-in, push-back nested cart systems, and carton flow systems convert wasted cubic volume into active product locations, doubling storage capacity without changing the warehouse footprint.
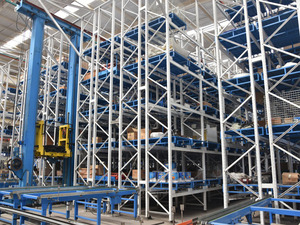
The development of ultra-thin, wireless radio shuttle cars has revolutionized deep-lane warehousing. Forklifts simply deliver pallets to channel entrances; the automated shuttle transports the load down 40-meter channels. This minimizes mast collision damage against uprights, accelerating load-unload cycle times by up to 35% in sub-zero freezers.
Vertical real estate optimization has accelerated the adoption of multi-tier rack-supported and structural steel mezzanines. By turning open air above ground-level staging into heavy picking floors, fulfillment facilities house conveyor sortation, light manufacturing, and multi-tier pick towers without the multi-million-dollar capital outlay of facility expansion.
Guangzhou HEDA Shelves Co., Ltd. – Global Manufacturing Scale
Founded in 2001, HEDA Shelves operates a modern 30,000 square meter manufacturing complex with 300+ seasoned engineers and precision technicians, shipping over 10,000 completed warehouse installations across North America, Europe, Southeast Asia, and Latin America.
Our in-house structural engineering office delivers comprehensive CAD plan views, elevations, 3D isometric renderings, and imperial/metric load capacity schedules within 24 hours of your site data submission.
03 / METALLURGY
Q235B / Q355B Certified Steel
Strict raw material procurement protocols ensure every coil matches certified chemical composition and tensile elongation parameters. Mill Test Reports (MTR) are provided alongside all batch container consignments.
04 / COMPLIANCE
CE, ISO 9001 & RoHS Validated
Independently verified under European Construction Products Regulation CE (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 quality assurance frameworks, guaranteeing full confidence during local building permit reviews.
Every upright frame, box beam, and bracing channel manufactured at HEDA undergoes continuous quality control checkpoints from raw steel receipt to final container staging.
STEP 01
Raw Material QC
High-grade Q235B/Q355B steel coils verified for chemical and mechanical specs.
Multi-roller pass machines form precision flanges, ribs, and interlocking channels.
STEP 05
Roll Profile Forming
Dedicated roll formers produce continuous seamless uprights and box beams.
STEP 06
Robot Deburring
Edges and connection cutouts are mechanically deburred to guarantee installer safety.
STEP 07
CO2 Robotic Welding
Beam end-connectors and baseplates welded under automated shielding gas control.
STEP 08
Pickling & Phosphating
8-stage chemical bath strips oil and scale, etching the steel for durable paint bonding.
STEP 09
Powder Coating
Electrostatic thermoset polyester powder applied and oven-cured at 200°C.
STEP 10
Final Staging & QC
Coating thickness, load deflection tests, bundling, and ocean packing.
Direct Engineering Consultation
Frequently Asked Questions by Industrial Buyers & Engineers
Get clear, authoritative answers regarding international standards, building permitting, floor slab requirements, and global container logistics.
How does HEDA Shelves support local building permits and seismic reviews?
We provide full calculation packages, structural drawings, component sectional properties (moment of inertia, section modulus, cross-sectional area), and detailed beam connection moment-rotation curves. These engineering packages are formatted for your local structural engineer of record (EOR) to apply local seismic coefficient stamps (IBC, ASCE 7, or Eurocode 8).
Are HEDA racking components fully compatible with standard 48"x40" GMA pallets?
Yes. While we customize systems for any dimension, our standard production lines configure beam spans (such as 96", 108", or 144") and frame depths (42" or 48") specifically calibrated around 48"x40" GMA pallets, Euro-pallets (800x1200mm), and heavy industrial metal stillages with safety stops.
What concrete slab specifications (PSI, thickness, flatness) are required?
Standard selective installations generally require a reinforced slab with a minimum 3,000 to 4,000 PSI compressive strength and 6" to 8" thickness. For high-bay, very narrow aisle (VNA) or high-density radio shuttle racks over 10 meters, floor flatness ratings of FF 45 / FL 35 or better are recommended to prevent excessive mast sway and dynamic lean.
How does your electrostatic powder coating handle sub-zero cold room environments?
Our 8-stage pre-treatment removes all grease, rust, and surface oxides, followed by an acid phosphating layer that forms a microscopic crystalline bonding foundation. Our heavy-duty thermoset polyester powder coating cures at 200°C, offering exceptional adhesion, impact resistance, and corrosion stability down to -30°C without flaking.
What is the typical production and ocean transit schedule to major ports?
Standard manufacturing cycle time is 15 to 25 days depending on project tonnage. Ocean container shipments from Guangzhou/Shenzhen port take approximately 14–18 days to US West Coast (Los Angeles/Long Beach), 26–32 days to US East Coast/Gulf (Savannah, Houston, NY/NJ), and 24–28 days to Western European destination ports.
How are structural components packaged to prevent damage during ocean transit?
Beams, frames, and decking are nested, bundled, banded with high-tensile steel strapping, and wrapped in protective multi-layer film with heavy edge-cushioning. Frame columns and cross-ties are pre-kitted to maximize 40HQ container cube utilization while allowing swift unloading by forklift slip-sheets or slings on site.
Request an Engineered Layout & Factory-Direct Quotation
Ready to maximize your warehouse cubic volume and lower your cost per pallet position? Contact our application engineering department with your building blueprints, clear height, pallet weights, and forklift parameters. Our team delivers a complete 2D CAD layout, 3D render, and transparent factory-direct proposal within 24 hours.
Live Project Review
Connect immediately with our senior logistics application specialists for instant design feedback.