Automatic 4-Way
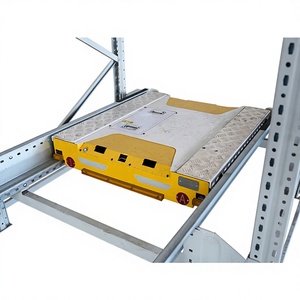
Automatic 4-Way Pallet Shuttle Racking System for Cold Storage
Sub-zero Rated
4-Direction Travel
WMS/WCS Linked
Explore our certified movable, shuttle, and modular pallet storage systems designed to maximize cubic volume utilization across cold stores, regional logistics hubs, and manufacturing plants.
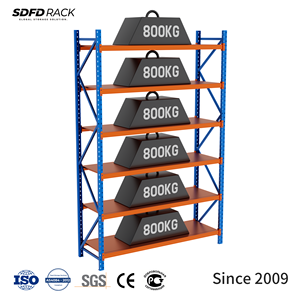
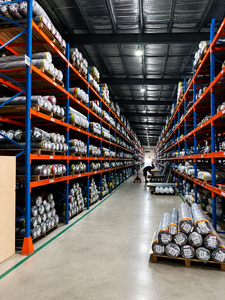
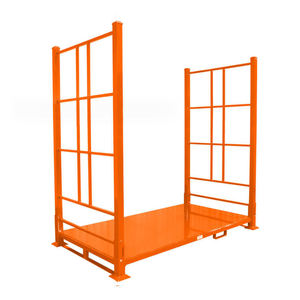
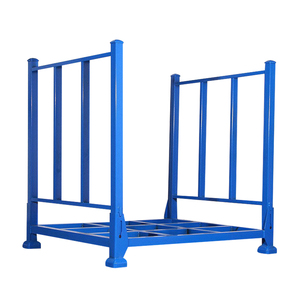
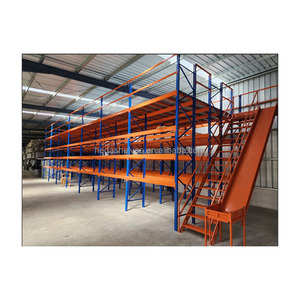
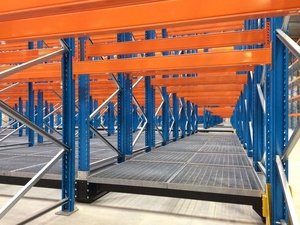
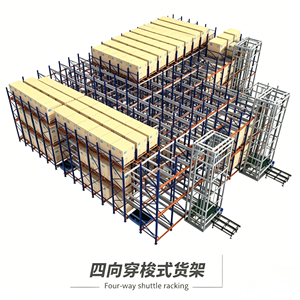
A comprehensive technical assessment for facility planners, logistics directors, and structural procurement specialists evaluating mechanical, motorized, and shuttle-assisted mobile storage assets.
Traditional static selective pallet racking dedicates as much as 60% of total warehouse floor surface to passive transit aisles. In contemporary industrial facilities grappling with surging square-meter land values, power expenses in temperature-controlled spaces, and regional inventory consolidation, this static model imposes severe capital waste. The implementation of CE-certified movable pallet racking systems replaces redundant dedicated corridors with a dynamic, single-access operational aisle operated manually, mechanically, or through synchronized industrial Programmable Logic Controllers (PLCs).
By mounting heavy-duty racking upright frames directly onto motor-driven mobile chassis running along precision-level in-floor steel guide rails, facilities eliminate up to 85% of redundant transit voids. The structural framework preserves 100% individual pallet SKU selectability while virtually doubling total storage capacity within the identical physical envelope. As a verified manufacturing exporter, our designs undergo rigorous calculation based on FEM 10.2.07 design codes, EN 15095 mechanical-safety regulations, and EN 15512 structural limits.
Technical Design Benchmark: Industrial movable pallet racking integrates electro-mechanical drives featuring soft-start and soft-stop frequency inverters to safeguard tall, stacked pallet configurations against dynamic horizontal acceleration shocks, ensuring compliance with international seismic, dynamic, and worker safety operational tolerances.
| Storage Topology | Volumetric Efficiency | SKU Selectability | Structural Floor Impact | Cold Chain Suitability | Permit Complexity |
|---|---|---|---|---|---|
| Motorized Mobile Racking | 85% - 90% | 100% (Direct Access) | Embedded Flush Guide Rails | Exceptional (50% HVAC reduction) | Seismic / Mechanical Stamped |
| Automatic 4-Way Shuttle | 90% - 95% | FIFO / LIFO by Lane | Standard High-Flat Slab | Maximum Efficiency | Automation / Software Code |
| Stackable Movable Racks | 60% - 75% | Block Selective | Zero Anchoring / Surface Load | Moderate | Minimal (Equipment Class) |
| Selective Pallet Racking | 40% - 50% | 100% (Direct Access) | Standard Slab Anchor Expansion | Baseline Cost Driver | Standard Building Permit |
Strategic insights for EPC engineers, operations leaders, and corporate procurement directors mapping CAPEX allocations through 2026–2030.
Cold chain facilities are shifting aggressively from wide-aisle configurations toward automated movable racking and four-way shuttle solutions. Because cooling empty aisle air represents up to 40% of refrigeration power costs, condensing footprint reduces both operating expenses (OPEX) and facility carbon profiles.
Modern mobile racking systems are shedding isolated analog interfaces. The new standard requires cloud-synchronized PLC control nodes equipped with industrial fieldbus APIs (Ethernet/IP, PROFINET) that interface directly with fleet-managed AMRs and automated reach trucks for hands-free pick cycles.
Global supply chain volatility has intensified scrutiny over cold-rolled steel metallurgy. Leading buyers reject generic cold-bent profiles in favor of certified Q355B and high-yield alloy formulations that preserve elongation, impact toughness, and load tolerance under -30°C deep freeze environments.
Combining 25+ years of engineering rigor, automated cold-roll forming capacity, and rigorous export documentation to serve global distribution operations.
Every movable chassis, upright column, and box beam undergoes automated continuous roll-forming, high-precision laser and CNC punching, certified CO2 protective welding, and automated multi-stage pickling, phosphating, and electrostatic powder coating in our dedicated manufacturing facilities.
Backed by official CE certification (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 quality management systems, our structural steel calculations and dynamic racking profiles comply with European EN guidelines, ready to assist client-side Professional Engineer (PE) seismic stamping.
Shipping long structural profiles demands specialized packing systems. Our logistics engineers configure high-density container stuffing solutions using customized steel cradles, vapor-corrosion inhibitors (VCI), and bundled strapping to ensure goods arrive true, undamaged, and site-ready worldwide.
Direct technical and operational answers to address common engineering, safety, permitting, and commissioning questions.
Connect directly with our senior racking engineering specialists. Submit your warehouse blueprint and storage profile to receive a complete CAD structural design, capacity analysis, and direct factory pricing within 24 hours.