25+
Years Racking Expertise
10,000+
Global Installations
30,000t
Monthly Output Capacity
100%
CE & ISO 9001:2015 Verified
Industrial Product Showcase
Engineered Dynamic Storage & Picking Infrastructure
Precision-fabricated gravity rollers, heavy-duty upright frames, and modular carton containment accessories certified to stringent international safety and performance criteria.
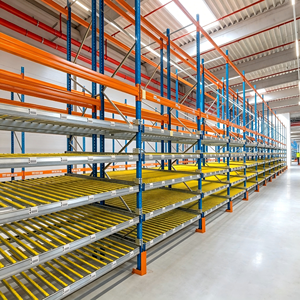
Technical Whitepaper: Precision Engineering in Modern Carton Flow Systems
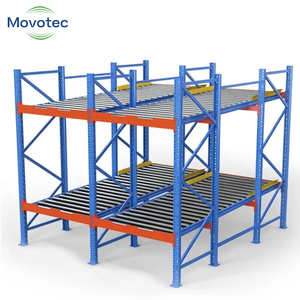
A CE Certified Carton Flow Rack System represents the foundational pillar of high-efficiency order fulfillment facilities, split-case picking modules, and high-velocity distribution hubs worldwide. Unlike static shelving configurations that create logistical bottlenecks, carton flow mechanisms utilize gravity-driven roller tracks laid at a calibrated incline—typically engineered between 2.5% and 5% pitch depending on tote material and package tare weight. This mechanical layout establishes distinct physical segregation between the restocking (loading) aisle and the order assembly (picking) interface.
As an internationally accredited manufacturer and premier exporter, we manufacture dynamic flow systems strictly in accordance with EN 15512, EN 15620, and the European Machinery Directive (2006/42/EC) under our CE certification (Certificate No. 2435-CPR-8605159). These design parameters ensure optimal shear resistance, load distribution without permanent deflections, and dependable material longevity across aggressive 24/7 operating environments.
Kinematic Efficiency: The Mechanical Physics of Dynamic Roller Tracks
The mechanical efficiency of a carton flow rack system rests entirely on wheel pitch, bearing friction coefficients, and bed frame rigidity. Our systems incorporate cold-formed, pre-galvanized sheet steel tracks fitted with heavy-duty polypropylene or high-impact polycarbonate wheels. Each roller wheel features a self-lubricating nylon bush or precision steel bearing rated for minimum rolling resistance under variable point loads ranging from 5 kg up to 50 kg per linear carton foot.
When totes travel down the lane, dynamic acceleration is governed by the tangent component of gravitational acceleration minus rolling friction. In extended-depth flow beds (exceeding 3,000 mm), uncontrolled acceleration poses safety risks to operators and increases box crushing incidents. Our export configurations integrate proprietary centrifugal brake rollers and entry impact dampers that maintain steady descent velocities below 0.3 m/s, delivering pristine merchandise directly to the operator's ergonomic strike zone.
| Evaluation Parameter | Static Industrial Shelving | Standard Push-Back Units | CE Certified Carton Flow Racks |
|---|---|---|---|
| Inventory Stock Rotation | Unregulated / Strict LIFO Manual | LIFO (Last-In, First-Out) | Enforced FIFO (First-In, First-Out) |
| Order Picking Travel Index | Baseline: 100% (High operator travel) | 70% - 80% (Moderate travel) | 25% - 35% (Minimal condensed travel) |
| Replenishment Interference | Direct aisle collision during pick cycles | Direct pick face loading conflict | Zero: Separate charge & discharge aisles |
| Storage Density Efficiency | Low (Aisles consume up to 60% floor space) | High (Compressed pallet lanes) | Maximum (Up to 150% picking surface utilization) |
| Ergonomic Strike Zone Accuracy | Requires bending & high reaching | Level reach; deep-reach friction | Drop-tray presenting pick face at natural tilt |
By enforcing an uncompromised FIFO (First-In, First-Out) sequence, facilities processing perishable foodstuffs, pharmaceutical medications, temperature-monitored cosmetics, and sensitive electronic assemblies completely eliminate date-expiration losses and maintain absolute stock visibility.
Strategic Market Forecasting
Future Trends in Carton Flow Racking & Procurement Directives
In-depth technical analysis for warehouse operations managers, 3PL procurement specialists, and materials handling engineers navigating supply chain automation.
Hybrid Pick-to-Light (PTL) Integration
Modern flow lanes are increasingly integrated with digital pick-to-light LED channels and sensor grids. Modern procurement contracts require pre-punched wiring ducts along intermediate crossbeams, allowing rapid deployment of optical sensors and zero-error fulfillment infrastructure.
AMR & AGV Charging Interface Standardization
The industry is transitioning toward automated rear-replenishment. Autonomous Mobile Robots (AMRs) now place replenishment totes directly onto charge roller beds, necessitating precise entry funnel geometries and dynamic impact guards rated for robotic docking forces.
Micro-Fulfillment & Multi-Tier Mezzanine Synthesis
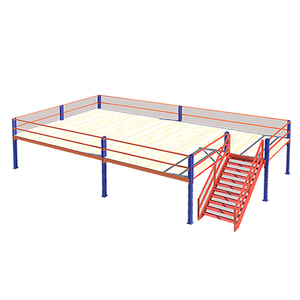
Urban real estate inflation drives distribution operations vertical. Procuring carton flow racks integrated directly within structural steel or rack-supported multi-tier mezzanines expands pick faces fourfold within the identical ground footprint, maximizing cubic volume utilization.
Eco-Coating & Lifecycle Decarbonization
Global environmental mandates emphasize non-toxic pretreatment cycles. Forward-looking buyers prioritize manufacturers employing electrostatic dry powder coatings cured without VOC emissions and cold-formed structural steel traceable to certified low-carbon melt facilities.
Manufacturer Provenance
Why Global Logistics Leaders Partner with Our Manufacturing Hub
Direct-from-factory engineering capability, unmatched scale, and complete ISO 9001:2015 certified quality systems delivering unyielding reliability to international distributors.
323,000 Sq Ft Precision Campus
Our expansive 30,000 m² modern manufacturing plant houses over 300 experienced technical experts, automated cold-roll forming lines, laser tube profiling cells, and high-throughput electrostatic coating lines yielding up to 30,000 tons of structural steel output each month.
Complimentary Engineering CAD & 3D Modeling
Our structural design department delivers bespoke CAD approval layouts, elevation schedules, and 3D visual renderings within 24 hours. Calculations can be natively scaled in imperial units (lbs/ft/in) or metric to facilitate smooth structural sign-offs.
Comprehensive Document Package & Stamped Calculations
Every export delivery is accompanied by comprehensive mill material certificates, ISO 9001:2015 tracking, CE compliance dossiers (CE 2435-CPR-8605159), component loading capacity labels, and step-by-step graphic installation manuals.
Container-Optimized Ocean Export Packaging
Upright posts, track assemblies, and shelf beams are packaged in timber-dunnage strapped bundles with protective edge angles, vapor corrosion inhibitors (VCI), and nested component palettes to eliminate sea transit damage and enable swift forklift offloading.
Frequently Asked Questions
Technical & Procurement FAQ: Carton Flow Rack Export Systems
Direct, unvarnished engineering clarity to assist project teams during system qualification and vendor due diligence.
What specific dynamic load limitations apply to carton flow tracks?
Our standard cold-formed steel roller tracks support up to 150 kg (330 lbs) per linear meter on standard span profiles, while heavy-duty reinforced track designs support up to 300 kg (660 lbs) per linear meter. Track beds can be subdivided into multiple parallel lanes via snap-in, tool-less zinc-plated steel lane dividers, ensuring carton alignment without track deflection under continuous dynamic loading.
How is the correct gravity track slope determined for diverse box materials?
The optimal flow gradient is determined by bottom-surface friction, total package weight, and base deflection. Standard smooth corrugated boxes function cleanly at a 3% to 3.5% gradient. Molded polypropylene totes or rigid plastic containers with recessed rims generally perform best at a 2.5% to 3% pitch. For recycled or soft-bottom cartons prone to sagging between roller axes, our engineers configure high-density roller arrays with pitch centers reduced to 28 mm, operating at an adjusted 4% to 4.5% pitch.
Can carton flow rack beds be retrofitted into existing selective pallet rack structures?
Yes. Our universal drop-in carton flow shelf beds are engineered with adaptable hanger brackets compatible with teardrop, slotted uprights, 50 mm, 75 mm, and 76.2 mm pitch column punches. This modular retrofit capability allows warehouses to convert lower pallet storage bays into high-efficiency split-case carton picking tunnels without replacing the existing heavy-duty upright frames or overhead buffer pallet tiers.
What surface pretreatment protocols guarantee long-term corrosion prevention?
Every structural component undergoes a thorough automated multi-stage pretreatment process: alkaline degreasing, clean-water immersion rinsing, acid pickling to eliminate mill scale, and zinc phosphate bath treatment to prepare optimal metal bonding adhesion. Components then enter an electrostatic powder application line depositing 60–80 microns of thermoset polyester powder coating cured at 180°C–200°C. Galvanized track profiles and zinc-plated dividers provide durable mechanical impact resistance against repetitive wheel loading.
What documentation is supplied to satisfy local municipal code and safety inspections?
We provide a comprehensive technical documentation package comprising full CAD drawings, static and dynamic stress analysis calculations, EN 15512/RMI-compliant design load sheets, CE Declarations of Performance, ISO 9001:2015 tracking reports, and raw material mill chemical analysis certificates. These verified documents allow local engineers and inspection authorities to approve operational building permits swiftly.
Transform Your Warehouse Throughput & Picking Performance
Consult directly with our logistics design engineers. Send us your facility footprint, carton dimensional criteria, and throughput requirements to receive a complimentary custom 3D layout, engineering load matrix, and direct export quotation within 24 hours.
Contact Us